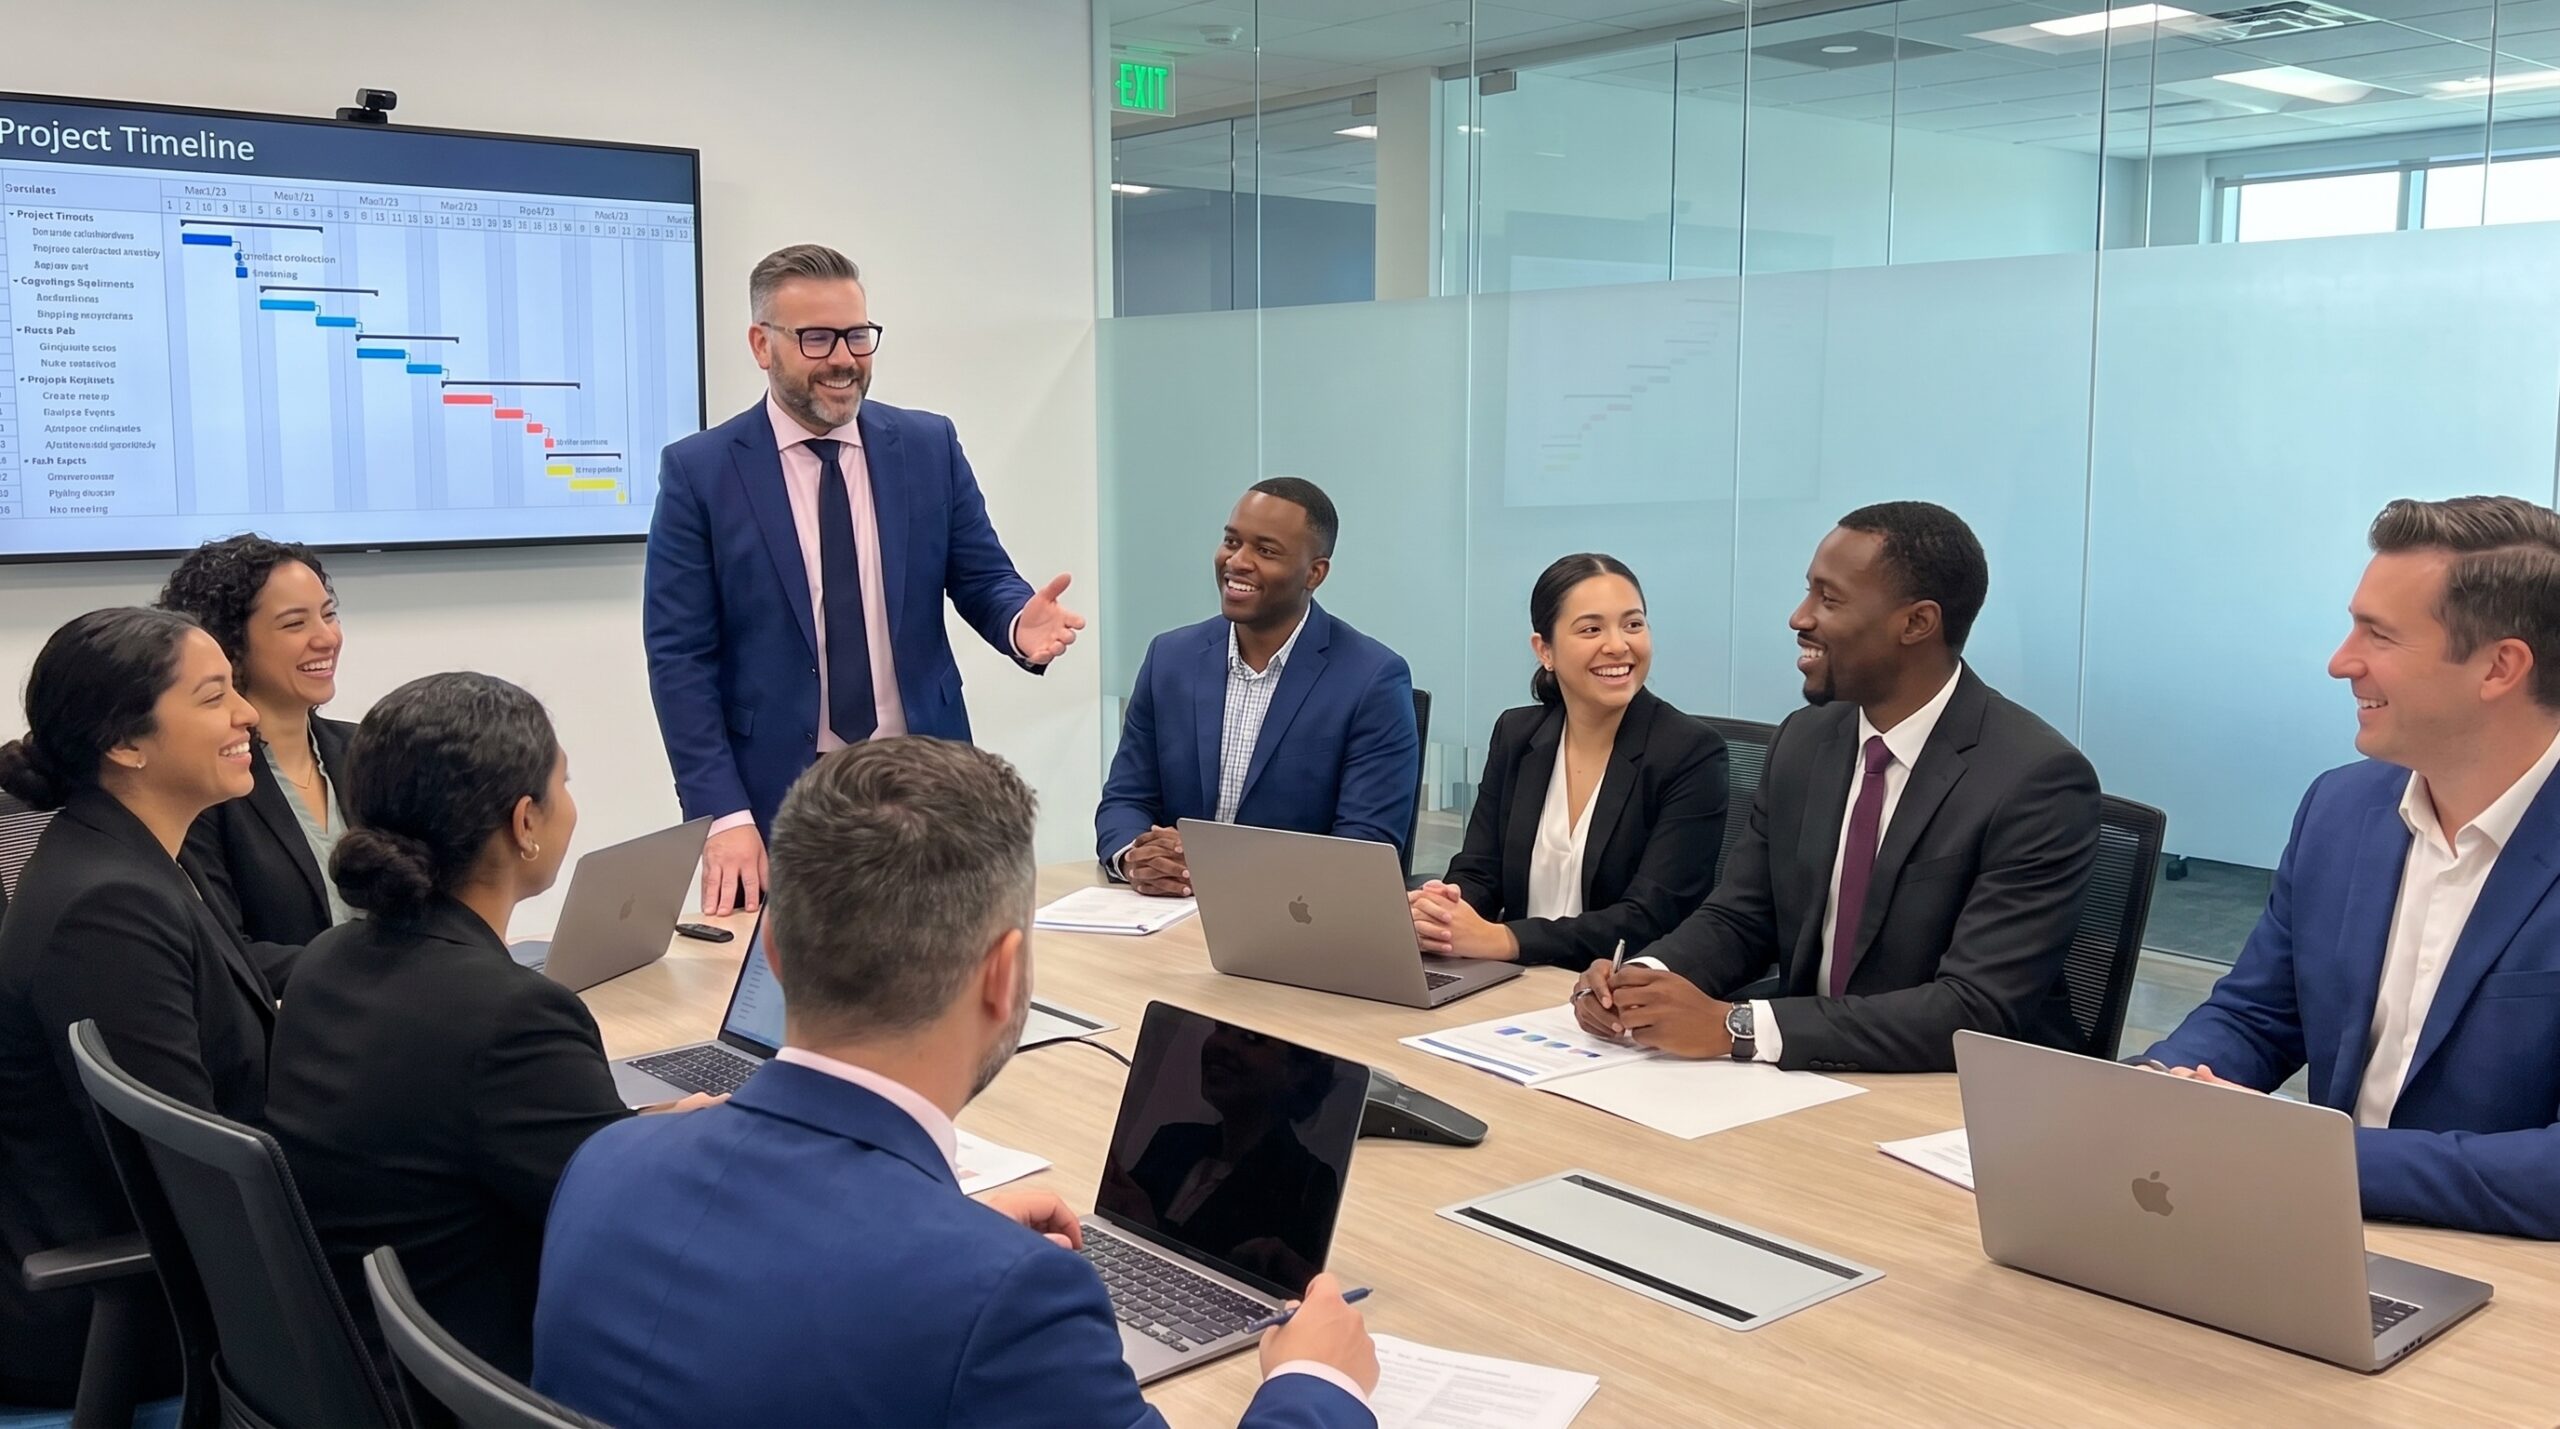
Most manufacturing organisations are structurally divided into isolated departments. Engineering, production, quality, procurement, and logistics each operate with their own manager, their own budget, and their own isolated objectives. This matrix is necessary for functional management, but it is lethal for product quality.
The resulting friction is predictable. Production blames quality for overly restrictive tolerances. Quality blames production for ignoring standard work. Engineering blames both for failing to understand the design intent, while the customer waits for their parts. Departmental silos are the enemy of continuous improvement because they obscure the process handoffs where most defects are actually generated.
Cross-functional teams are the operational answer to this systemic failure. This is not about creating a new department or adding a layer of middle management. It is a targeted mechanism for forcing different functions to align on a single, measurable objective. Having implemented and transitioned ISO 9001 systems across automotive and aerospace plants, I have seen cross-functional alignment reduce internal lead times by up to 97% simply by forcing engineering and quality to share the same dashboard.
What Defines a Cross-Functional Quality Team
A cross-functional team is a specifically selected group of personnel drawn from different departments who are held jointly accountable for one shared goal. They do not abandon their departmental roles, but they commit to a unified operational target. The structure is temporary and highly focused.
The composition of a typical quality-driven team must reflect the reality of the product lifecycle. For an Advanced Product Quality Planning (APQP) launch or an 8D problem-solving effort, you need diverse operational lenses. A standard configuration includes a Quality Engineer as the process owner, a Process Engineer, a Production Supervisor, and a Design Engineer.
You also need representation from the supply chain and material handling. A Purchasing Representative and a Logistics Representative are critical to ensure that tooling and raw materials are available. Most importantly, I always mandate the inclusion of a Production Operator. The people closest to the manufacturing process invariably hold the most accurate data regarding process failure modes and cycle constraints.
Selecting the wrong stakeholders guarantees failure. If a team lacks the authority to change a work instruction, alter a purchase order, or update a Control Plan, the initiative stalls. Empowerment is the prerequisite for execution.
Deploying Teams Across the Quality Lifecycle
Cross-functional structures are not a universal solution applied identically to every scenario. You must match the team configuration to the specific phase of the quality lifecycle. The trigger for the team must be a clear operational event.
A new product launch demands an APQP team focused on achieving PPAP submission without deviations. A field failure or major customer complaint requires an 8D team focused on containment and root cause analysis. Supplier non-conformances require a dedicated supplier development team that bridges your engineering, procurement, and the vendor's quality assurance.
| Operational Trigger | Team Configuration | Primary Output |
|---|---|---|
| New Product Launch | APQP Team | Approved PPAP Package |
| Customer Complaint | 8D Problem Solving Team | Verified Root Cause & CAPA |
| System Transition | QMS Implementation Team | Certified ISO 9001 / IATF 16949 System |
| Supplier Nonconformance | Supplier Development Team | Corrected Process Flow & Stable Cpk |
When a structural management system change is required, such as transitioning from ISO 9001 to AS9100, the implementation team must guide the entire organisation. They map the standard requirements to existing procedures and manage the gap analysis. Using the wrong team for an RCA investigation wastes engineering hours and delays corrective actions.
Five Rules for Leading Cross-Functional Teams
Gathering people in a room does not constitute a team. Managing these dynamics requires a disciplined approach to leadership. Without clear rules of engagement, the team will default to departmental defensiveness, protecting their own KPIs rather than solving the problem.
Rule one is a singular, shared objective. The goal must be universally understood and measurable. A target like 'reduce scrap' is inadequate because production may achieve it by slowing down the line. A proper target is 'reduce scrap on line four without compromising the cycle time or Cpk requirements.'
Rule two is structural equality within the meeting space. A Production Operator has the same voting power as a Plant Director. Rule three mandates data over opinion. If someone claims a machine cannot hold a tolerance, they must present the capability study. Rule four focuses on momentum: secure quick wins early to build credibility.
Rule five is strict meeting cadence. Weekly stand-up meetings must be limited to fifteen minutes to review blockers. Monthly reviews should take sixty minutes to analyse progress against the project Gantt chart. Without a forced communication rhythm, the team disintegrates.
The Mechanics of Team Velocity
APQP Execution: Anatomy of a Saved Launch
Consider a new product launch for a tier-one automotive supplier. The timeline was fixed at twenty-eight weeks to achieve PPAP submission. At week twelve, engineering executed an uncontrolled change to the raw material specification to improve structural integrity.
Because the change occurred in a silo, production continued without updated work instructions. The quality department was unaware that the existing Control Plan was now invalid. Procurement had not ordered the new resin, and the logistics team had not adjusted the warehouse allocation.
The solution was the immediate formation of a cross-functional APQP team. We established a shared project dashboard, implemented a clear RACI matrix to define decision rights, and mandated weekly thirty-minute stand-up meetings. The shared objective was non-negotiable: deliver a zero-finding PPAP package by day 196.
Empowerment is the prerequisite for execution. If a team lacks the authority to change a work instruction, the initiative stalls.
The team identified the missing material immediately, updated the PFMEA, and accelerated the new capability studies. The PPAP was submitted on day 189—one week ahead of schedule—with zero customer findings. The silo failure was converted into a functional launch through rigorous project governance.
Bridging the Departmental Divide
Eliminating silos is not about redrawing the organisational chart. Functional departments must exist to maintain specialised expertise and manage budgets. The solution is constructing deliberate operational bridges between these functions.
When an operator, a design engineer, and a buyer sit at the same table to solve a dimensional capability issue, the dynamic changes. The conversation shifts from blame allocation to process verification. The engineer sees the fixture interference, the buyer understands the material constraint, and the operator explains the handling difficulty.
This alignment is what turns theoretical quality planning into actual product conformity. Effective cross-functional teams succeed not because the individuals are unusually gifted, but because the process forces them to share data, align their targets, and execute decisions collectively.
Stop allowing departmental boundaries to dictate your quality output. Build the cross-functional structure, enforce a strict meeting cadence, demand data over opinion, and tie their performance to a single, unified objective.