Cross-functional blame is the default reaction when a defect escapes to the customer. Production blames tooling, tooling blames the material supplier, and quality insists the process ran out of specification. Meanwhile, the customer escalates. Having implemented quality systems across automotive and aerospace plants, I have watched this cycle waste weeks of engineering capacity without addressing the actual failure mode.
Structured problem solving breaks this loop by forcing the conversation onto a single, standardised sheet. A3 Problem Solving, derived from the Toyota Production System, takes its name from the standard 297 × 420 mm paper format. The physical constraint is deliberate. If a team cannot articulate the problem, the root cause, and the verified corrective action on one page, they have not yet grasped the situation.
This is not a simplification of the engineering process. It is a mechanism for disciplined thinking. A3 forces a transition from opinion-based arguments to evidence-based analysis. It replaces firefighting with a systematic progression from problem definition to root cause verification and process integration.
The Seven Phases of A3 Methodology
An A3 is not a blank canvas for unstructured brainstorming. It is a storyboard with strictly defined phases. Each section must be completed sequentially to prevent teams from jumping straight to corrective actions before validating the underlying failure mode.
The first phase demands business context. You must quantify the impact of the defect on the customer, delivery, and commercial risk. When a supplier faces three customer complaints over two weeks with twelve thousand euros in warranty costs and a high risk of losing an OEM contract, that financial and delivery exposure suddenly secures the attention and resources of plant management.
The second phase requires mapping the current state. You map the process exactly as it operates on the floor, not as it exists in the approved control plan. Using a value stream map or flow diagram, you identify where value is lost and where defects are generated. A gearbox housing might pass through six operations, three of which lack defined inspection points. A winding tension parameter out of specification for months goes unnoticed simply because it became a normalised deviation.
The third phase sets the target condition. The goal must be specific and time-bound. The objective is not to generally improve quality, but to reduce the housing defect rate from 2.3 percent to under 0.1 percent within sixty days. Without a quantifiable target, the A3 degrades into an academic diagramming exercise.
Executing Root Cause Analysis
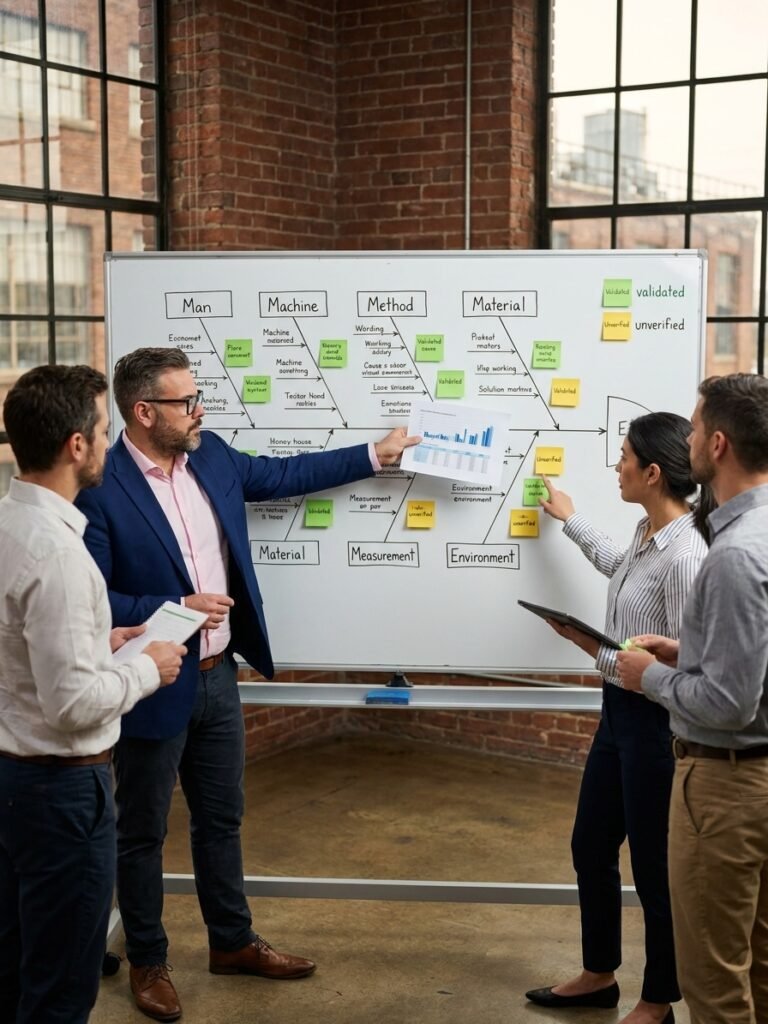
Root cause analysis is where the rigorous work begins. Teams typically apply the 5 Whys alongside an Ishikawa diagram to isolate the fundamental failure mechanism. The goal is to separate the systemic root cause from the immediate symptom. In the case of the defective housing, analysis consistently points to multiple contributing factors across different operational domains.
An operational cause might involve an incorrectly calibrated machine parameter. A systemic cause often stems from a missing go/no-go gauge or inspection template at a critical stage. A human cause frequently traces back to a lack of operator certification or inadequate training for a newly introduced material grade. The A3 methodology demands that each identified cause be verified with process data, not assumptions.
Proposing countermeasures follows the root cause verification. Solutions are mapped directly to the identified causes, assigned a clear owner, and given a firm deadline. Corrective actions must be designed as testable hypotheses. They are implemented to see if they eliminate the specific failure mode identified during the analysis phase.
| Identified Root Cause | Corrective Action | Owner & Deadline |
|---|---|---|
| Winding pressure deviation | Recalibration and SPC monitoring | Maintenance (7 days) |
| Missing post-operation 4 inspection | Manufacture go/no-go gauge | Tooling (14 days) |
| Lack of material handling knowledge | Operator certification programme | Quality & HR (30 days) |
Implementation and Follow-up
The implementation phase dictates who executes the countermeasures, what resources are required, and when the actions will be completed. A simple timeline or Gantt chart tracks progress. This section of the A3 operates as a living document, updated continuously to reflect the reality of the shop floor rather than a static plan left on a manager's desk.
Follow-up monitoring is critical. If the countermeasures work, the team needs objective proof. This requires defining the exact metrics that will be tracked and the duration of the monitoring period. When a team implements a viable solution, the monitoring data confirms its effectiveness and triggers the transition to standardised work.
For the gearbox housing, the team implemented an SPC chart for the critical dimension, tracked weekly customer complaints, and instituted a monthly layered process audit. Within ninety days, the defect rate dropped to 0.04 percent, and customer complaints ceased entirely. The solution was verified, and the new controls were integrated into the standard control plan.
Why A3 Outperforms Fragmented Reporting
The primary reason A3 delivers results where 8D reports and isolated digital dashboards fail is visualisation. When a cross-functional team stands around a single physical A3 sheet, the blame game evaporates. The facts of the process, the data, and the identified failure modes speak directly, removing the emotional friction that stalls corrective action.
The rigid structure of the document prevents cognitive shortcuts. Human nature naturally gravitates toward immediate fixes, but the A3 format enforces analysis before action. You cannot fill out the countermeasure section without first completing the root cause analysis. This sequencing is what separates systemic problem solving from reactive firefighting.
The quality of the A3 correlates directly with the depth of the team's engineering analysis.
Using A3 as an after-the-fact reporting tool to satisfy management is a waste of engineering resources. Filling out the document retrospectively means the critical thinking was never structured. A3 is a thinking tool designed to guide a team through problem resolution in real-time, on the shop floor, not an archive document for a compliance audit.
Integrating A3 with Core Quality Tools
A3 does not operate in isolation. It functions as the structural framework that integrates core quality methodologies into a single, coherent narrative. The analytical power of the document relies entirely on the underlying quality tools applied during its creation.
A3 Integration with Quality Methodologies
- 01Cause AnalysisIntegrate 5 Whys and Ishikawa diagrams to validate failure modes.
- 02Risk MitigationApply PFMEA logic when designing operational countermeasures.
- 03Process MonitoringUse Statistical Process Control (SPC) data for verification metrics.
- 04StandardisationUpdate the Control Plan and apply PDCA for continuous tracking.
When PFMEA, SPC, and PDCA are tied together under an A3 framework, they generate verifiable engineering data. The methodology ensures that risk analysis informs the countermeasure design, while statistical data dictates whether the process change actually eliminated the defect.
Deploying A3 on the Shop Floor
Implementing A3 requires shifting from desk-based analysis to Gemba-based observation. Select a real, high-impact problem that affects delivery or quality metrics. Form a small, cross-functional team of four or five engineers and operators. The diversity of the team prevents blind spots in process knowledge.
Go to the actual location where the defect is generated. Data in an enterprise resource planning system cannot convey the physical reality of a worn tool or an unstable fixture. The team must map the current state with a pen on the A3 sheet while standing directly in front of the manufacturing process.
Iterate. The first A3 a team produces will likely have analytical gaps. The second will show tighter cause-and-effect logic. Once completed, these documents should be displayed at the point of use. A wall of resolved A3s serves as a visible library of engineering knowledge, training new operators and preventing the recurrence of solved issues.
The ultimate output of this methodology is not a resolved nonconformance report. It is a cultural shift toward systematic thinking. Organisations that adopt A3 build an engineering culture based on verifiable data, standardised work, and verified root cause analysis, fundamentally reducing the frequency and severity of manufacturing defects.