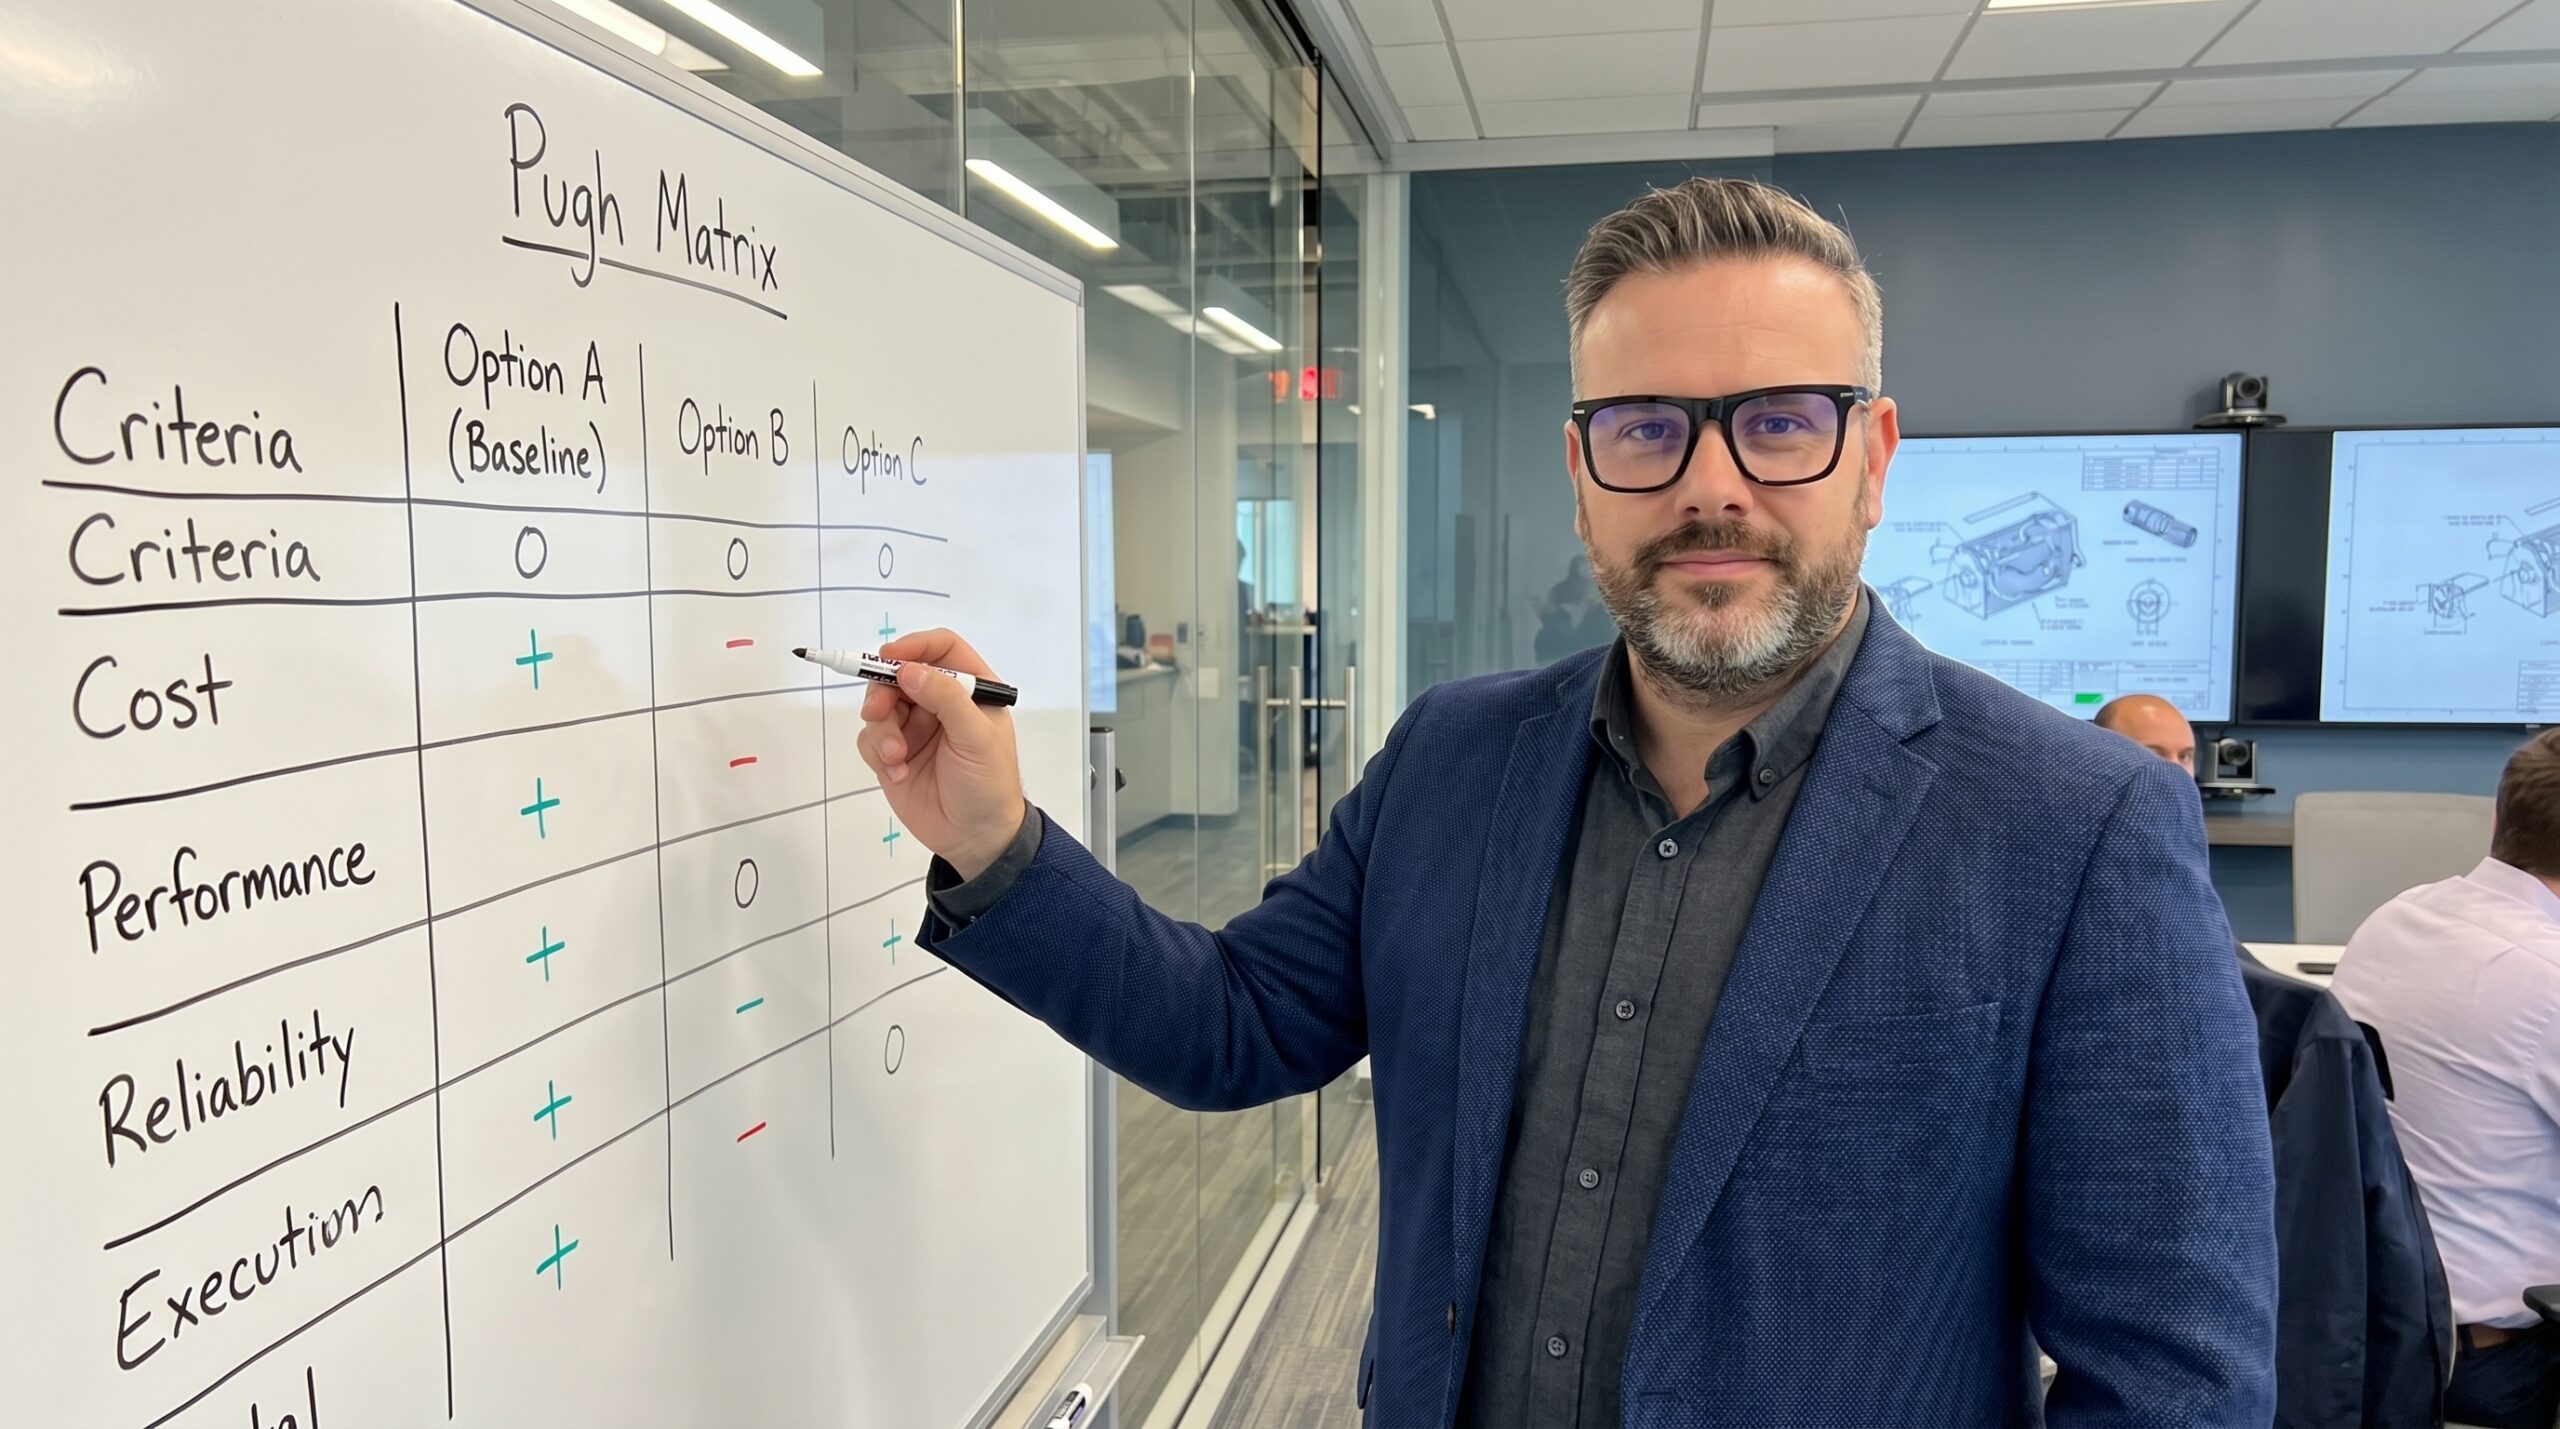
Concept selection in manufacturing engineering routinely descends into a battle of opinions. The lead designer advocates for an innovative feature, the production manager demands manufacturability, and procurement pushes for the cheapest material. Without a structured evaluation framework, the final decision is often dictated by whoever argues loudest in the meeting room. This tribal approach to engineering design destroys traceability and guarantees suboptimal outcomes.
I have sat in those conference rooms. During a critical APQP Phase 2 review at an automotive client, the engineering team spent two hours deadlocked over four competing sensor-mounting designs. Energy was spent defending personal preferences rather than evaluating the requirements. We resolved the impasse in twenty minutes using a Pugh Matrix—a systematic evaluation tool that converts subjective debates into objective, auditable engineering decisions.
Developed by Stuart Pugh, the method evaluates multiple concepts against a baseline reference using predefined criteria. It strips emotion from the decision-making process. In quality engineering, it is the standard mechanism for selecting product designs, supplier sourcing, root cause corrective actions, and measurement methodologies during Advanced Product Quality Planning.
Building the Evaluation Framework
The success of a Pugh Matrix relies entirely on the criteria defined before any concept is evaluated. These criteria must be specific, measurable, and extracted directly from customer specifications, regulatory requirements, and core tools like the House of Quality. Vague parameters like 'quality' or 'ease of use' are unacceptable. You must define concrete metrics such as 'vibration resistance up to 20G' or 'assembly cycle time under 30 seconds'.
A robust matrix requires criteria from multiple disciplines. Design engineering provides technical parameters like load capacity and dimensional tolerance. Manufacturing contributes assembly time, automation potential, and tooling complexity. Procurement supplies material costs and supply chain risk. Quality adds end-of-line testing requirements and serviceability. If these criteria are defined by a single function, the evaluation is fundamentally biased.
Selecting the baseline is a strategic decision. The baseline is your current state or industry-standard solution, and it automatically receives a score of zero (0) for every criterion. If you select a weak baseline, every proposed alternative will look exceptional. If you select an overly ambitious baseline, viable concepts will be discarded. Always use the current production design or the best-known competitor solution as your anchor.
Each alternative concept is then evaluated against the baseline. If a concept performs better than the baseline for a specific criterion, it receives a plus (+). If it performs identically, it receives a zero (0). If it performs worse, it receives a minus (−). The three-level scale forces discipline and prevents teams from hiding marginal improvements behind inflated numerical scores.
Executing the Evaluation Cycle
Filling out the matrix is a facilitation exercise. The cross-functional team must evaluate every concept, criterion by criterion, out loud. This verbalisation exposes assumptions. When a design engineer marks a plus for assembly time, the production engineer must agree based on the defined standard. Disagreements at this stage highlight misunderstandings about the concept itself before any tooling is cut.
The Pugh Evaluation Cycle
- 011. Define CriteriaExtract 8-12 specific parameters from QFD, FMEA, and customer specifications.
- 022. Set the BaselineAnchor the matrix to the current production design or known industry standard.
- 033. Score AlternativesEvaluate each concept against the baseline using +, 0, and − to ensure team consensus.
- 044. SynthesiseCombine the strongest elements of top-scoring concepts into a robust hybrid solution.
Summing the scores provides a mathematical baseline for the discussion. Plus scores equal +1, minuses equal −1, and zeros remain 0. The concept with the highest aggregate score becomes the lead candidate. However, the aggregate score is a discussion prompt, not a final verdict. The matrix organises the debate; it does not replace engineering judgement.
In the automotive sensor bracket evaluation, Concept A (integrated clip) scored highest. However, reviewing the matrix revealed that Concept D (adhesive bonding) scored significantly better for vibration resistance. Instead of blindly accepting Concept A, the team synthesised a hybrid solution. We combined the clip mechanism with an integrated adhesive surface. This final design exceeded the original requirements and entered serial production.
Weighted Matrices and Killer Criteria
Basic Pugh evaluation treats all criteria equally. In reality, a safety requirement or a critical IATF 16949 compliance mandate carries more weight than aesthetics or recyclability. A weighted Pugh Matrix assigns a multiplier (e.g., 1 to 5) to each criterion based on risk and criticality. Multiplying the baseline comparison (+1, 0, −1) by the weight forces the team to explicitly agree on what factors are true showstoppers.
| Criterion | Weight | Concept A (Clip) | Concept D (Adhesive) |
|---|---|---|---|
| Vibration resistance | 5 | 0 | +5 |
| Assembly robustness | 5 | 0 | +5 |
| Tooling investment | 2 | −2 | +2 |
| Recyclability | 3 | +3 | −3 |
| Total Weighted Score | +1 | +9 |
Weighting must be handled with discipline. It is tempting for a functional lead to artificially inflate the weight of their specific domain to ensure their preferred concept wins. Weights must be negotiated and locked before evaluating the alternatives. This prevents manipulation and keeps the focus on system-level optimisation rather than functional favouritism.
Even with a weighted matrix, you must enforce killer criteria. A concept might accumulate the highest mathematical score, but if it receives a minus on a critical safety or regulatory parameter, it is disqualified. No amount of positive scores in aesthetics or assembly speed can override a failure to meet an EASA or FDA mandated requirement. Define these killer criteria explicitly before the evaluation begins.
Integration with APQP and Core Tools
The Pugh Matrix does not operate in isolation. It is a structural bridge between core quality tools. The criteria evaluated in the matrix flow directly from the Quality Function Deployment (QFD) and the Design FMEA. The risks identified during failure mode analysis—such as potential misuse or high assembly variation—become explicit criteria in the Pugh evaluation.
The output of the matrix feeds directly into the subsequent APQP phases. Once a concept is selected, it undergoes a full Process FMEA. The characteristics that drove the Pugh decision—the specific assembly method chosen or the material selected—dictate the controls established in the Control Plan. The PPAP submission then validates that the chosen concept can be manufactured consistently within these defined controls.
This traceability is critical for external audits. An IATF 16949 auditor will ask why a specific manufacturing process was chosen over an alternative. The Pugh Matrix provides the documented evidence. It proves the decision was based on evaluated risks, customer requirements, and cross-functional consensus, rather than arbitrary management preference.
Common Failure Modes in Application
The most frequent failure is mechanical scoring without discussion. Teams calculate the totals and immediately adopt the winning concept. The Pugh Matrix is a facilitation tool, not a calculator. The value lies in the conversation that happens when a production engineer questions a plus score from a design engineer. The final numbers are useless if the team has not debated the underlying physics and assembly realities.
The matrix organises the debate; it does not replace engineering judgement.
Failing to execute a synthesis phase is another major failure. Teams stop when they find a winner. The most innovative engineering solutions often emerge after the initial scoring, when the team examines the matrix to see if they can combine the strongest elements of the top two concepts. Bypassing this step leaves significant technical performance on the table.
Finally, matrices are frequently bloated with thirty or more criteria. This creates noise and guarantees evaluation paralysis. The optimal range is between eight and twelve criteria. This forces the team to filter out minor preferences and focus purely on the parameters that dictate actual product performance, manufacturing capability, and quality system compliance.
Measuring the Impact on Lead Time
Implementing systematic concept selection directly reduces project lead time. In my experience managing greenfield quality departments, mandating Pugh evaluations eliminated the cyclical arguments that stall design reviews. Decisions that previously took weeks of back-and-forth emails were concluded in a single, structured afternoon session.
Pugh Matrix Session KPIs
You can measure this effectiveness by tracking decision cycle times and post-launch engineering changes. Teams that consistently use the matrix during APQP Phase 2 experience fewer late-stage design changes. Because production, quality, and procurement agreed on the evaluation criteria upfront, the selected design survives the transition from prototype to serial production without major structural modifications.
Implement this tool on your next stalled decision. Assemble a cross-functional team, define the criteria based on actual customer and engineering specifications, and score the alternatives against a realistic baseline. Skip the complex AHP software; a simple grid on a whiteboard is sufficient. The goal is to make the engineering knowledge of your team visible and auditable, driving consensus through pure logic.