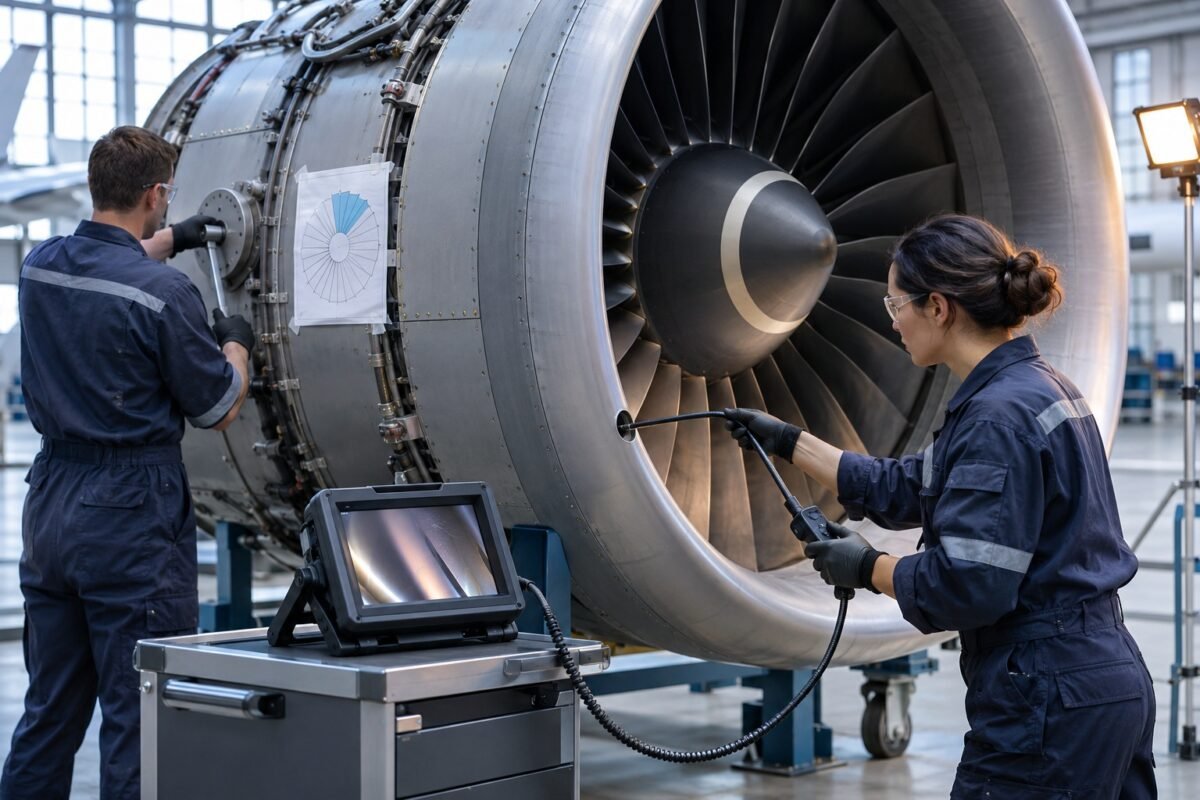
Borescope inspection asks something unnatural of an inspector: form a defect verdict on a component you will never see in its entirety. A turbine blade viewed through a 4 mm port presents perhaps a third of its surface at usable resolution, at an angle you did not choose, through optics that distort geometry at the frame periphery. Every conclusion carries an implied caveat — based on what was visible — and the entire discipline exists to make that caveat as small and as honest as possible.
Across two decades in automotive and aerospace quality, I have seen organisations treat borescope work as "just a visual inspection with a fancy camera", and those are the ones that get caught out. The failure modes differ from bench inspection. Depth perception is largely absent on a 2D monitor, so a shallow pit and a deep corrosion crater look identical until you probe with tip deflection or stereo measurement. Lighting falls off sharply with distance from the distal tip, meaning the far wall of a combustor liner is often assessed at marginal illumination.
The honest framing is this: a borescope inspection is a structured sampling exercise of a surface, conducted under constrained optics. The output is not "the blade is good". The output is "the accessible regions, inspected to this procedure, at this resolution, showed these indications". Discipline means making each of those qualifiers explicit and defensible.
Building Coverage Plans That Mean Something
A coverage plan is the contract between the inspector and the part. Without one, two inspectors will produce two different maps of the same engine, and neither can tell you what was actually examined. The plan should be zone-based: divide each inspectable module — fan, booster, HPC, combustor, HPT, LPT — into discrete zones defined by fixed anatomical references, not inspector discretion. Stage 1 blade pressure side and suction side are separate zones. The blade root platform, the squealer tip and the trailing edge each get their own identity in the record.
For each zone, the plan must specify the inspection point, the insertion path, the tip articulation required and, critically, the expected field of view. When I audit borescope procedures, the fastest way to find weakness is to ask for a photograph of what "complete" looks like for a given zone. If the procedure cannot show a reference image of full coverage, the inspector is navigating by feel, and coverage becomes inspector-dependent. Reference images per zone, captured from a known-good engine, are worth more than pages of prose.
Access physics dictate technique. Turning the rotor to bring each blade row under the port is standard, and the plan must state the increments — indexing blade by blade, or in groups with overlap — so no blade sits in the geometric shadow of a port edge. Overlap is the operative principle: adjacent viewing positions should share visible features, so a defect straddling a boundary appears in at least two image sets.
Where a zone is only reachable at an oblique angle exceeding roughly 45 degrees, the plan should say so and require a compensating method, such as closer approach or a second viewpoint. Obliquity compresses the image and hides cracking aligned with the viewing axis — one of the most consequential blind spots in the entire technique, and entirely preventable if the plan acknowledges it.
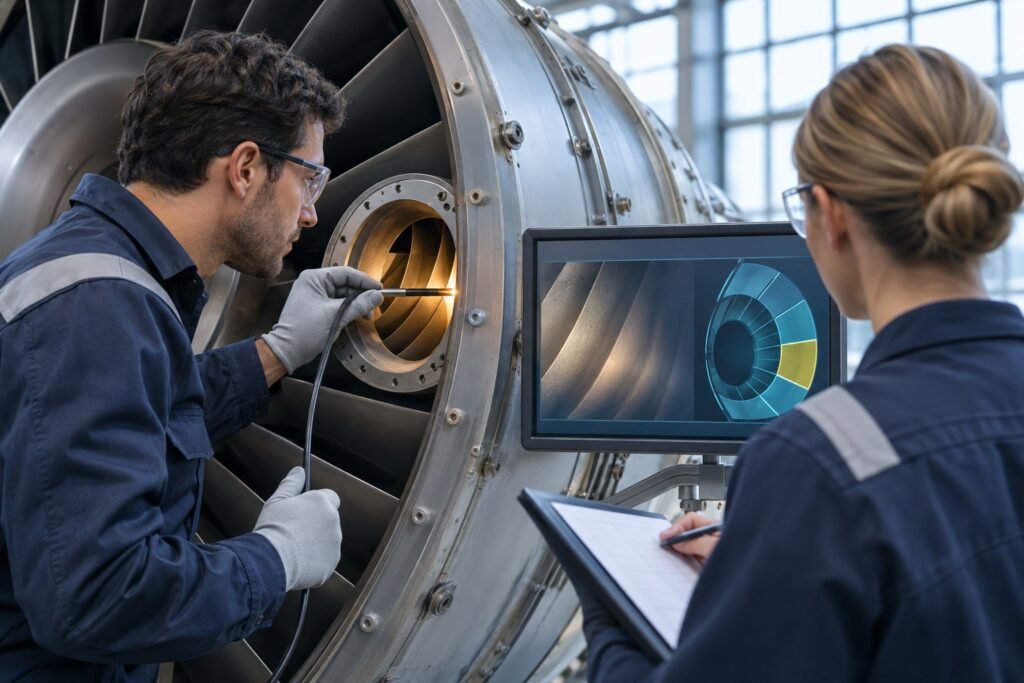
Image Records: Evidence, Not Souvenirs
The image record is the only part of the inspection that survives the day. Engines return to service, inspectors rotate shifts, and eighteen months later a finding needs comparison against a baseline — was that crack always there, has it grown? A folder of JPEGs named "IMG_0421" is not a record. It is clutter with metadata attached.
Each image needs, at minimum, embedded or sidecar data: engine serial number, module, zone identifier per the coverage plan, date, inspector identity, instrument identity including distal tip type, and viewing direction. Still images should be captured at the working distance the assessment was made at, not a staged beauty shot from a different position. Video has a place — it demonstrates the traversal path and proves coverage continuity — but video alone is a poor classification medium, because compression softens the fine texture that distinguishes a scratch from a crack.
Measurement deserves specific care. If indication lengths are recorded from a stereo-measurement tip, the calibration status of that tip and the measurement distance matter, because uncertainty grows with stand-off and viewing angle. A 1.8 mm recorded indication at 70 degrees obliquity carries materially more uncertainty than the same reading taken square-on. When the disposition hinges on whether an indication sits above or below a limit, the record should make the uncertainty visible to the reviewer, not hide it behind a false-precision number.
Retention rules should follow the engine, not the work order. When a shop-visit report later correlates findings across visits, the historical borescope images are the primary evidence of defect progression. I have seen disposition arguments settled or lost purely on whether the previous images could be located and trusted.
Inspector Fatigue: The Quiet Enemy of Small Defects
Borescope inspection is ergonomically hostile work. The inspector holds an articulated probe under tension, often one-handed, while manipulating insertion depth, articulation, zoom and illumination with the other, watching a monitor in a noisy hangar with poor ambient control. Fatigue in this trade does not arrive as dramatic error; it arrives as drift. Coverage increments get larger. Dwell time per blade shortens. The inspector stops re-articulating to check a suspicious highlight and classifies it as reflectance.
Task timing should be managed deliberately. Sustained borescope work degrades detection performance well before the inspector feels tired, and self-reporting is an unreliable guard. Shift the demanding modules — HPT blade inspection, combustor liner — to the first hours of an inspection block, not the last. Cap continuous inspection blocks and mandate breaks that involve genuine visual rest, away from monitors. Rotor indexing is a natural interruption point: use it for a short pause rather than pushing through six blade rows without lifting the head.
Environmental and physiological factors compound. Hangar lighting glaring off the monitor, cold hands from working near engine inlets, awkward postures craning to see lower-half ports on a large engine — all consume attention that would otherwise go to the image. Magnification pushes fatigue in both directions: too low and the inspector strains to resolve fine detail, too high and the search field shrinks until the eye works harder to maintain spatial orientation. Standardising magnification per zone in the procedure removes one decision the tired inspector would otherwise make badly.
Where borescope verdicts degrade
Defect Classification Under Optical Constraint
Classification is where borescope work earns its difficulty. The classic traps are well known: scratch versus crack, spallation versus discolouration, a cooling hole's soot ring versus actual burn-through, tip rub versus foreign object damage. What the optics give you is texture, shadow behaviour under moving illumination, and geometry — and the inspector must read those cues knowing the optics will occasionally lie.
Illumination behaviour is the primary tool. A crack presents as a line that holds a shadow when the light source moves, because it has depth and a wall. A scratch, being a furrow with raised shoulders, catches light along one edge and loses it along the other, flipping as the tip articulates. Pitting shows discrete shadows with defined peripheries; oxidation shows diffuse tonal change without edge structure. Train inspectors to articulate deliberately while observing, because a static image flattens exactly the cue that separates these conditions.
A static image flattens exactly the cue that separates a crack from a scratch; the articulation is the diagnosis.
Correlation with other evidence is essential for anything consequential. A suspected HPT blade crack adjacent to the platform deserves cross-checking against engine performance data, findings from previous visits, and the condition of adjacent blades — thermal-fatigue cracks often appear in populations, while a single linear indication in a high-contact zone may be handling damage. Where classification is genuinely ambiguous and the limit is close, the correct answer is not a cleverer guess through the scope. It is a documented escalation: pull the engine, or apply the manufacturer's conditional-release criteria with the uncertainty stated.
Measurement-based classification should follow the type certificate holder's limits precisely, including where on the indication the measurement is taken — maximum dimension, projected length or area — because these are not interchangeable. Orientation relative to the blade's principal stress axis changes significance: a crack aligned span-wise near the root carries a different conversation than the same length chord-wise at mid-span. The classification record should capture orientation, not just size.
Instrument Control and Recurrent Qualification
Instrument condition matters as much as inspector skill. Distal tips get damaged, illumination LEDs degrade, and articulation cables stretch until the tip no longer reaches the position the procedure assumes. A quick functional check before each use — articulation to specified angles, illumination output, image sharpness against a reference target — is minutes well spent. Log instrument hours and treat probe replacement as scheduled maintenance rather than failure-driven, because a degrading probe produces subtly worse images long before anyone declares it broken.
Training should be conducted on defect-representative hardware, not clean training engines. Welded specimens, seeded cracks and retired blades with genuine service damage build the pattern library in an inspector's head far better than any slide deck. Recurrent qualification should test detection on realistic, partially visible defects at realistic angles.
Qualification events should also occasionally seed nothing. Knowing how to clear a zone confidently is as important as knowing how to find a flaw — an inspector who cannot clear cleanly will either over-reject sound hardware or, worse, learn to dismiss ambiguity. Both failure modes are trained behaviours, and both are preventable with honest test design.
Feeding Findings Back Into the Plan
When a defect is found at a shop visit in a zone that field borescope inspections had repeatedly cleared, the correct response is not blame. It is a hard look at whether the zone was genuinely visible from the inspection points, whether the obliquity made that defect class undetectable, and whether the plan needs a new viewpoint. The plan is a living document; the engine will eventually tell you where it is blind, and the disciplined organisation writes that down.
Closing the loop on a missed defect
- 01Detect the escapeShop visit finds a defect in a zone previously cleared by field inspection
- 02Reconstruct visibilityPull the archived images and determine what the inspection points could actually resolve
- 03Test the techniqueCheck obliquity, magnification and overlap for that zone against the defect class
- 04Revise the planAdd a viewpoint, closer approach or compensating method where the physics failed
- 05RequalifyUpdate reference images and confirm inspectors can execute the revised zone
That loop is what separates a mature programme from a paper one. Coverage plans, image records, fatigue management and classification discipline are not four separate initiatives; they are one system in which each part supplies the evidence the others depend on. The record proves the plan was executed. The plan defines what the record must contain. Fatigue control protects the judgement that classification demands. Build all four, or the weakest one will eventually set the standard for the rest.