I have handed over flawlessly structured Control Plans and complete PFMEAs, only to return a month later and find operators still working the old way. Supervisors ignored the new procedures. Managers cited different priorities. The technical solution was perfect. The implementation failed entirely.
We blame the quality management system, the training budget, or the workforce. The real failure point is simpler and harder to accept: we engineered the process but ignored the people who have to run it.
Technical perfection accounts for roughly half of a project's success. The remaining half is the human factor. Quality professionals who dismiss this as a soft skill are the ones who watch their IATF 16949 or AS9100 compliance initiatives stall year after year. We must treat change management as a core quality engineering discipline, governed by the same rigour we apply to MSA or capability studies.
The Mechanics of Resistance to Change
Resistance to a new quality requirement is rarely irrational. It is a predictable response to disruption. When you introduce a new SPC tracking method or a revised routing verification, you invalidate existing operator experience. People naturally protect their competence.
Fear of the unknown drives much of this resistance. Operators ask themselves if they will still meet takt time with the new checks. They wonder if the new system is being introduced because management believes they are doing a poor job. If you do not answer these unspoken questions, rumours will fill the silence.
Past failures weigh heavily on the shop floor. If a plant has seen three failed ISO 9001 system upgrades in five years, the workforce will treat your new initiative as a passing phase. They will wait you out. You must explicitly acknowledge past failures and explain, with evidence, why this deployment is structurally different.
Standard Communication vs Structured Change
What teams usually do
- Email the updated work instruction as a PDF attachment.
- Give a one-hour PowerPoint presentation to the whole shift.
- Expect compliance because the new standard is logical.
- Leave enforcement to the shift supervisors.
What actually drives adoption
- Show the scrap data and explain the cost of failure.
- Run hands-on practice on the line in small groups.
- Assign a buddy to help operators clear the learning curve.
- Audit the new process daily using Layered Process Audits.
Building the Framework: ADKAR in Practice
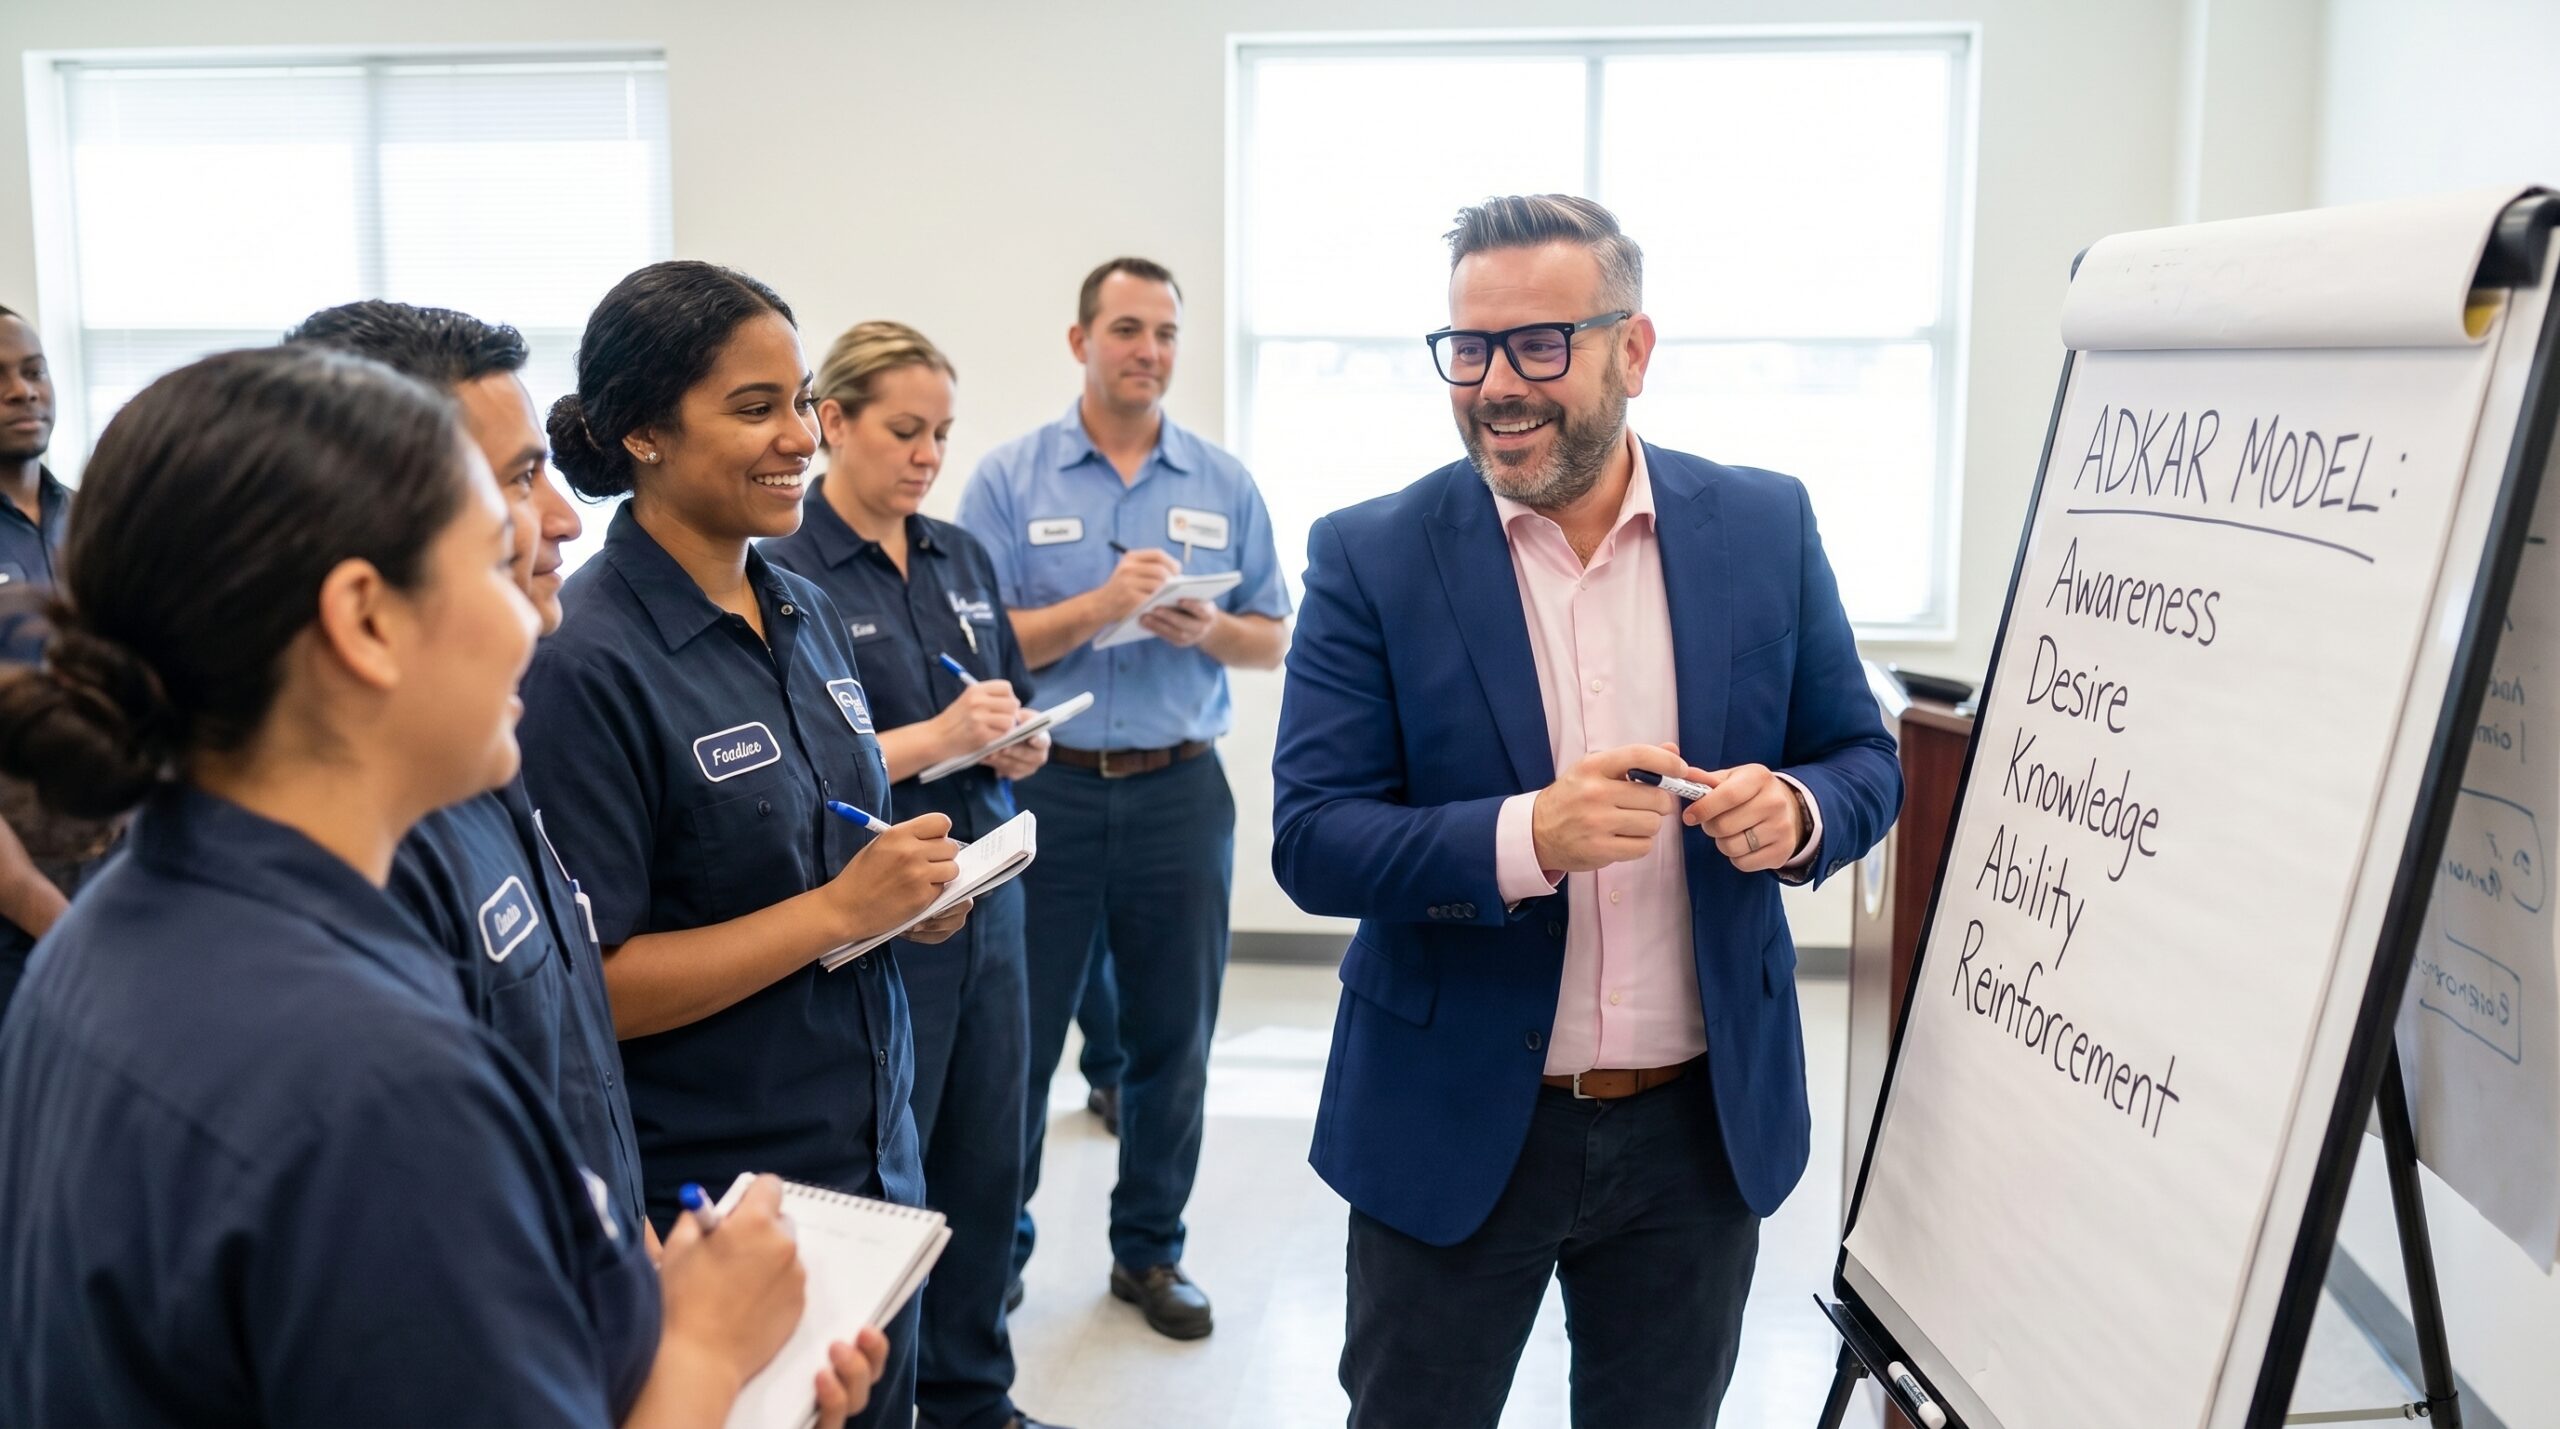
The ADKAR model—Awareness, Desire, Knowledge, Ability, Reinforcement—defines the sequential states an individual must pass through to adopt a change. Skipping a step guarantees failure. If you train people before they want the change, the training is ignored.
Awareness requires hard data. You must present the business case unflinchingly. If customer complaints have driven PPM levels to unacceptable heights, show the charts. Explain that failing to meet the required Cpk of 1.33 risks losing a major contract. Awareness is not about generating fear; it is about establishing the undeniable need for action.
Desire is personal. You build it by answering the question every operator asks: 'What is in it for me?' The new process must be framed as a tool that reduces their stress and rework. When you involve operators in designing the solution—asking them which checks actually add value—their desire to see it succeed increases dramatically.
Converting Knowledge into Operational Ability
Knowledge transfer in quality fails when it relies purely on classroom instruction. A presentation on interpreting SPC charts does not translate to shop-floor competence. Knowledge must be delivered at the gemba, using the actual gauges and materials the operators will handle.
Ability requires time and resources. You cannot mandate a new process on a Monday morning and expect immediate perfection. A quality engineer or technician must be present on the line for the first two weeks. They need to answer questions, troubleshoot the new measurement system, and actively remove the friction that drives people back to the old way.
Deploying a New Quality Requirement
- 01Baseline the DataEstablish current reject rates and process capability.
- 02Communicate the CostShow the plant how the current failure rate impacts business.
- 03Workshop the SolutionInvolve operators in designing the new visual controls.
- 04Co-Run the LineQuality engineers actively support the first two weeks of production.
- 05Lock In with LPAEmbed the new process into Layered Process Audits.
The environment must be prepared. If you introduce a new data collection requirement, the forms, calibrated instruments, and software must be ready before the shift starts. Any delay in providing tools immediately destroys your credibility and validates the operators' skepticism.
Reinforcement: Making the Change Permanent
A change is only sustainable when it survives its first major crisis. The first time a new SPC chart signals an out-of-control condition, or a new check slows down the line, people will revert to old habits. Reinforcement is about catching that reversion immediately and correcting it without punitive action.
I have seen plants celebrate a successful 8D implementation after just two weeks of smooth running. This is premature. You must wait until the new process has survived an audit, a high-pressure delivery week, and the absence of a key supervisor before declaring victory. Celebrating too early signals that the hard work is over.
Layered Process Audits (LPA) are the most effective mechanism for reinforcement. Embedding the new procedure into the daily LPA ensures that supervisors and managers are actively verifying compliance. When leadership checks the standard on the shop floor every day, the workforce understands that the change is permanent.
Leadership Presence and Communication Failures
The most common cause of deployment failure I observe is a communication breakdown. Management emails a revised PPAP package or a new work instruction and considers the communication complete. Archiving a document is not communication. Effective communication requires dialogue, feedback loops, and visible management commitment.
Leadership must be physically present on the line. If a plant manager announces a critical quality initiative but never visits the shop floor to observe the new process, the initiative is dead. 'Do as I say' has never worked in manufacturing. Operators watch what management prioritises, not what they announce.
The best quality system in the world is worthless if the people running the process do not understand or accept it.
Identify your key stakeholders early. Find the most experienced, respected operator—the informal leader—and engage them first. If you can convince them to test the new process and validate it, the rest of the shift will follow. Ignore them, and you will face active resistance from the people who hold the most influence.
Integrating Change Management into Quality Planning
Quality professionals must stop treating change management as an external soft skill. It is a critical competency that belongs inside APQP and project planning. When you build a Control Plan, you must simultaneously build a deployment plan that accounts for operator training, resistance mitigation, and resource allocation.
The arithmetic of implementation is absolute. A perfectly engineered technical solution combined with poor change management yields an unimplemented project. A merely acceptable technical solution, combined with excellent change management, yields a successful transformation that drives continuous improvement.
Before you launch your next quality initiative, map the ADKAR phases against your timeline. Confirm that you have the data to build awareness, the engagement to build desire, the resources to build ability, and the audit strength to reinforce it. If any of these elements are missing, delay the launch until they are resolved.