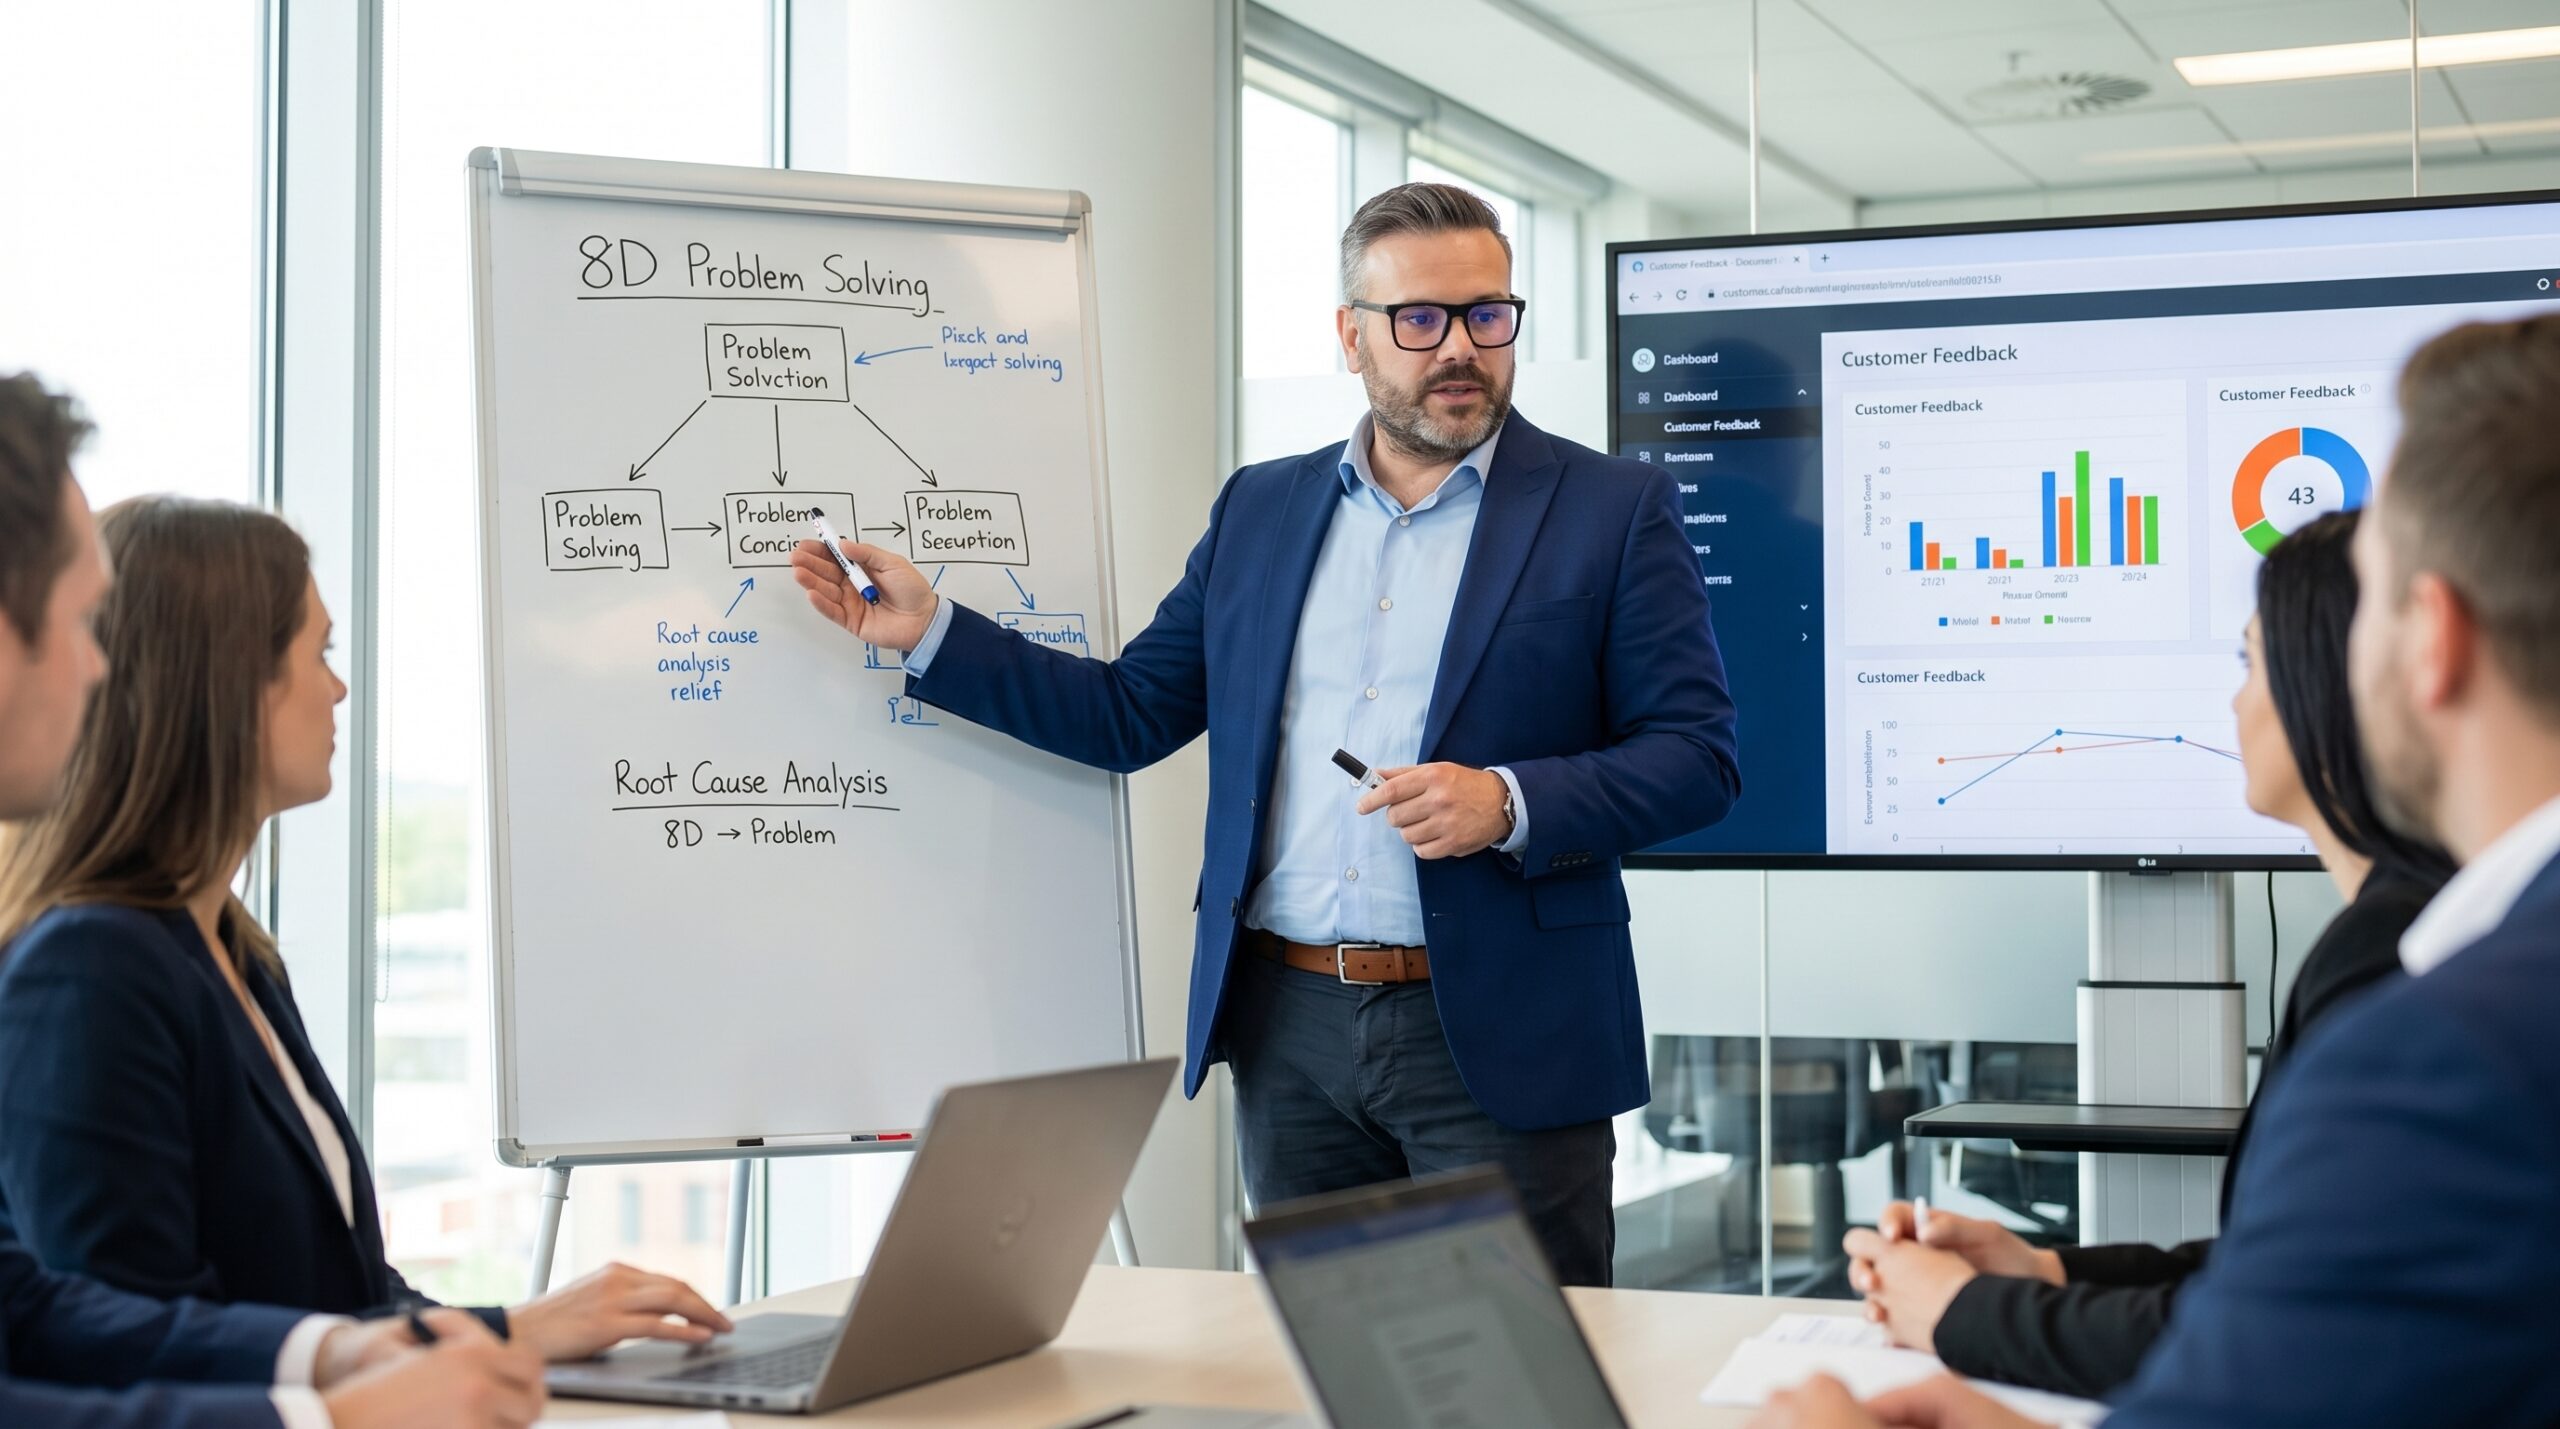
Most manufacturing plants treat a customer complaint as a public relations event. The supply chain manager hides the email, the commercial team issues a credit note, and the quality department never sees the defect. This ad-hoc approach guarantees the failure will repeat on the next shipment.
A complaint is not a diplomatic incident. It is a highly specific, customer-funded process audit revealing exactly where your quality planning failed. Discarding that data without rigorous 8D methodology is the most expensive waste in manufacturing.
I have audited plants that prided themselves on low complaint rates, only to discover they were aggressively filtering 8D requests at the account management level. The actual defect rate was hidden. When they started logging every customer signal as formal 8D case, the volume spiked, but repeat escapes dropped to near zero within twelve months.
Containing the Escape Before It Spreads
The clock starts the moment the customer sends the rejection notice. Under IATF 16949 and AS9100 requirements, your first obligation is physical containment, not investigation. If the defect is in the field, you must identify the inventory footprint immediately to stop the bleeding.
D0 containment means physically locking down all suspect stock at your facility, in transit, and at the customer's distribution centre. You segregate the affected batches, suspend the relevant production line if necessary, and verify that no further nonconforming product can ship.
The response must reach the customer's quality engineer within 24 hours. This containment report outlines the immediate physical actions taken to protect their assembly line. It does not guess the root cause. It simply proves you have locked down the perimeter and are actively managing the risk.
Deploying the 8D Methodology Without Excuses
The 8D framework is the mandatory engine for processing complaints in automotive and aerospace. It forces a cross-functional team—engineering, production, quality—to move through disciplined problem description, root cause identification, and permanent corrective action.
Teams fail at 8D when they skip D2. If you cannot define the defect in strict, measurable terms, your root cause analysis will chase ghosts. "The part was defective" is not a problem description. "Burr height exceeded 0.2 mm on the mounting bore, causing interference fit failure" is a workable D2 definition.
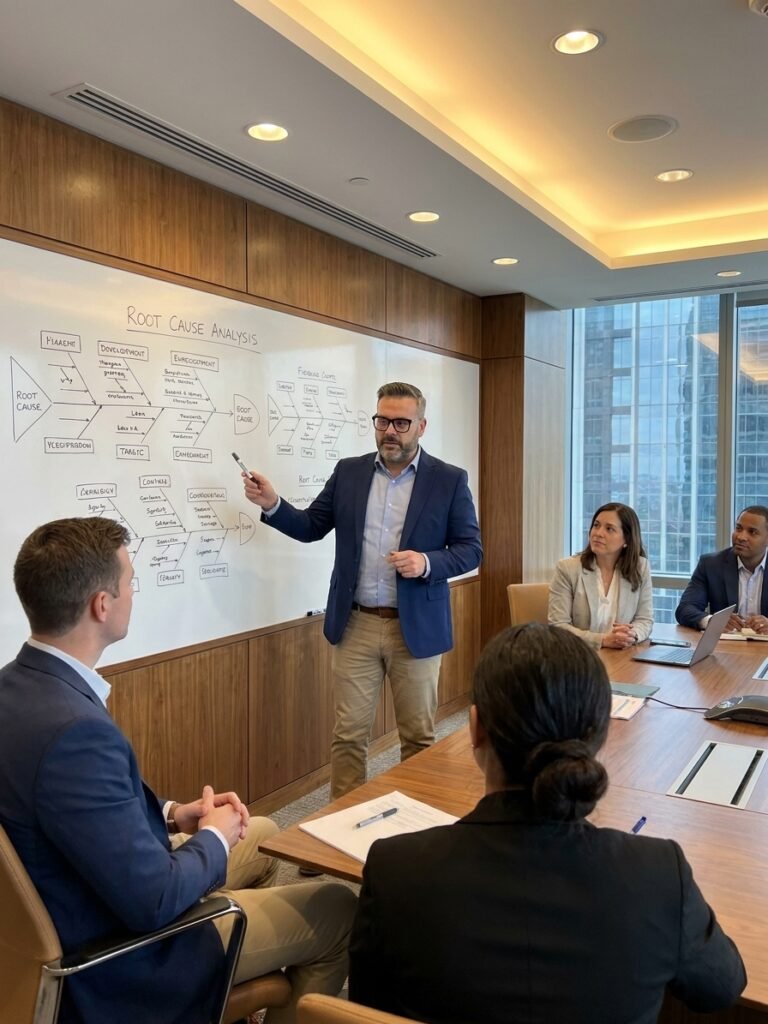
Most organizations want to jump straight from containment to a permanent fix. This bypass of D4 root cause analysis is why defects recur. You must verify the actual mechanism of failure using 5 Whys, Ishikawa diagrams, or Design of Experiments before proposing a permanent correction.
The 8D Containment and Resolution Sequence
- 01D0: Emergency ContainmentLock down all suspect stock globally within 24 hours of notification.
- 02D2: Problem DescriptionDefine the failure in measurable, objective terms to focus the investigation.
- 03D4: Root Cause IdentificationDetermine the specific process failure using 5 Whys or Ishikawa analysis.
- 04D6: Corrective Action VerificationStatistically confirm the fix eliminates the failure mode before full deployment.
- 05D7: Systemic PreventionUpdate PFMEA, Control Plan, and work instructions to lock in the improvement.
Executing Root Cause Analysis on the Factory Floor
Root cause analysis is where supplier quality teams expose their actual competence. A surface-level root cause—operator error—will result in an immediate rejection of your 8D report by any competent customer QA engineer. You must dig into the systemic failure that allowed the operator to make the error.
I managed a packaging compliance complaint where components arrived with outdated labelling at a Tier 1 plant. A lazy investigation would reprimand the packer and close the 8D. The real systemic cause was a lack of layered process audits and an outdated work instruction that did not reflect the new customer requirements.
The corrective action was not disciplinary. It was a revision of the PFMEA, an update to the control plan to include a mandatory label verification step, and a formal training matrix sign-off for all shipping operators. The systemic fix prevents the defect across all product lines, not just the single part that triggered the complaint.
Managing Customer Communication and Perception
Quality engineers are trained to analyze defects, not to manage customer relationships. This is a critical gap. The communication surrounding an 8D investigation dictates whether the customer tightens their audit scope or maintains confidence in your process capability.
Never let the customer discover the timeline. You must provide proactive updates at defined intervals, typically every 48 hours, until the interim containment is verified. Silence breeds assumption, and assumption breeds escalation to the customer's purchasing directory.
A complaint is the only time a customer pays you to audit your own process.
Accept the failure immediately. Defending an obvious defect damages credibility instantly. Acknowledge the escape, present the containment data, and commit to a strict timeline for the full 8D report. This demonstrates control of the quality management system.
Integrating CAPA and PFMEA Updates
Corrective and Preventive Action (CAPA) does not end with the customer accepting the 8D report. The systemic failure must be deployed across your entire manufacturing network. If a specific machine parameter caused a burr on a part for Customer A, you must verify that same parameter on similar parts for Customer B and Customer C.
This horizontal deployment is where you extract the actual return on investment from a complaint. You are using one customer's failure signal to proactively prevent escapes across your entire facility. Without this step, your quality system operates in isolated silos, constantly reacting to identical root causes on different production lines.
The final documentation step is updating the PFMEA and Control Plan. If the risk priority number for the specific failure mode was low, your core documentation is flawed. Adjust the severity, occurrence, and detection ratings to reflect the newly validated reality of the process failure.
Complaint Response: Ad-Hoc vs Systematic
Reactive Approach
- Customer service issues a credit note to close the case.
- Root cause is guessed at by a sales manager without floor presence.
- PFMEA and Control Plans remain unchanged after the escape.
- The same defect recurs on the next production run.
Systematic Approach
- Mandatory 8D initiated within 24 hours of customer alert.
- Cross-functional team verifies root cause on the factory floor.
- Control plans updated with permanent, Poka-Yoke style detection.
- Defect mechanism eliminated horizontally across all product lines.
Measuring the ROI of Complaint Resolution
The financial justification for a rigorous 8D process is straightforward. The cost of implementing systemic corrective action is always a fraction of the cost associated with lost contracts, expedited freight, and line-down penalties at the customer's assembly plant.
When a plant implements strict 8D tracking and PFMEA horizontal deployment, the metrics shift measurably. Warranty costs drop, scrap rates fall due to Poka-Yoke implementations, and customer audit scores rise from conditional to preferred supplier status.
Treat your complaint register as the most accurate process audit data available. The customer is testing your parts in the field under conditions your laboratory cannot replicate. Every 8D report you close correctly hardens your entire manufacturing system against future variation.
Impact of Systematic 8D Deployment