Every quality manager has lived through this conversation. A part fails in the field, the customer demands to know which requirement was violated, and you open the design file to find nothing. Not a failed requirement — an absent one. Nobody ever wrote down that the bracket must survive a 48-hour salt spray exposure, or that the connector must retain its locking force after fifty mating cycles. You cannot test what was never specified, and you cannot claim compliance against a blank page.
I spent the first decade of my career treating design controls as someone else's paperwork. The engineers owned them; I owned the production side. That division of labour cost me on more than one occasion, because the defects that hurt most were the ones seeded before a single drawing reached the shop floor. Across two decades in automotive and aerospace quality, I have come to accept an uncomfortable conclusion: manufacturing quality begins at the design input stage, whether we like it or not.
The deeper problem is that most quality managers are trained to verify conformance, not to interrogate completeness. We audit what exists. When the input set itself has holes, our verification passes cleanly and tells us nothing. That is the trap, and this article is about how to spot it before the customer does.
Design Inputs: Where the Real Specification Lives
Design inputs are not the drawing. The drawing is an output. Inputs are the collected needs — regulatory, customer, functional, environmental, interfacing — from which the design must be derived. In regulated sectors the standard phrase is that design inputs shall be documented, reviewed and approved, and the review is where quality must sit at the table. A vague input such as "must be robust" is untestable; a specific input such as "must withstand 30 g shock for 11 ms without loss of function" flows straight into a test protocol.
Check the input set against the failure modes of the product's intended environment. If the component lives under a vehicle bonnet, inputs must cover thermal cycling, vibration spectra, fluid exposure and electrical transients. If any of those are missing from the input list, you have found a latent defect more dangerous than anything on your production line. Ask the design lead to walk you through the input-to-output derivation for three critical characteristics at random. Hesitation is a signal.
Look also for conflicting inputs. A housing specified for both flame retardancy and a particular recycled polymer may contain an intrinsic contradiction nobody resolved. Conflict resolution records, or their absence, tell you whether the input review was a real engineering activity or a signature collection exercise. That distinction determines whether the whole control chain downstream rests on engineering or on hope.
Verification Versus Validation: Two Different Questions
Verification asks: did we build the product correctly, against the specification? Validation asks: did we build the correct product, against the actual need? The distinction matters because a part can pass every verification test and still fail validation. I have seen fuel system components sail through dimensional and material verification, then fail validation because the customer's assembly operators could not reach the clip with a gloved hand — an ergonomic need nobody captured as an input.
On the verification side, the mechanics are familiar: dimensional layout, material certification, functional bench tests, environmental endurance. Each verified requirement needs a defined method, an acceptance criterion and a sample basis. What quality should police is the orphan test — a protocol run with no traceable requirement behind it, or a requirement with no method assigned. Both directions of mismatch are defects in the control system itself, and both are visible in an afternoon of document review.
Validation is harder because it simulates use, not specification. Vehicle-level durability running, field trial fleets, installation studies with real operators and real tooling, transport and drop testing in production packaging. Schedule pressure always attacks validation first, because it sits at the end of the programme. Resist the substitution of analytical validation for physical validation on safety-related characteristics unless the analysis has genuine correlating test history behind it.
The Traceability Matrix: A Map, Not Bureaucracy
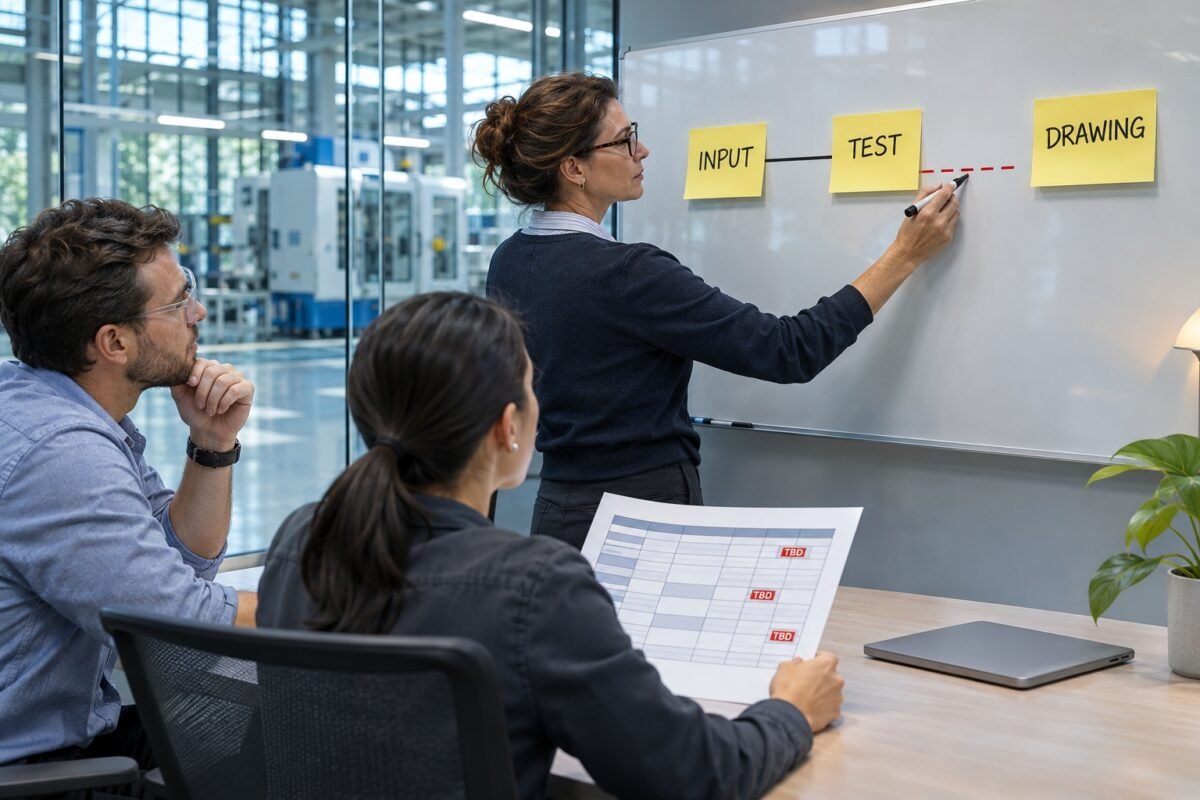
A traceability matrix is a cross-reference table linking each design input to its verification method, test result, and the output — drawing, specification, software requirement — that implements it. Done properly, it is the single most powerful audit tool available to a quality manager, because it exposes three failure modes at once: requirements with no test, tests with no requirement, and requirements with no implementing output.
Build one and read it ruthlessly. Rows where the "verified by" column says TBD past design freeze are unwritten tests waiting to become field failures. Columns referencing cancelled test reports, or reports with deviations never dispositioned, are worse. On one aerospace programme I inherited, the matrix existed but nobody owned it; it had drifted two revision levels behind the requirement baseline and gave false comfort to everyone who glanced at it.
A stale traceability matrix is more dangerous than no matrix at all, because it certifies a control that no longer exists.
The matrix also disciplines change. When engineering proposes a design change, the impact analysis starts there: which requirements does this feature touch, which tests must repeat, which downstream outputs need revision. Without it, change review degenerates into opinion. Insist that the matrix is a living controlled document with a named owner, reviewed at every design review gate — not a deliverable assembled retrospectively for the customer audit.
How an unwritten requirement becomes a field failure
- 01Need discussed, not capturedAn environmental or interface requirement stays in meeting minutes and never enters the input set.
- 02Design proceeds unconstrainedMaterial and geometry are selected without the missing condition, and nothing blocks release.
- 03Verification passesThe test protocol contains no method for the requirement that was never written.
- 04Validation misses itField trial units are never exposed to the real use condition either.
- 05Field failure, wrong ownerCorrective action lands on manufacturing, where the root cause never lived.
How Unwritten Requirements Reach Production
Trace the anatomy of a typical escape. An environmental need — say, resistance to a specific cleaning chemical used at the customer's plant — is discussed in a meeting but never captured as an input. The material is selected without that constraint. Verification passes, because nothing in the protocol addresses chemical exposure. Validation might have caught it, but the field trial units were never run through the cleaning process. Eighteen months later the parts craze, and the corrective action lands on manufacturing.
The pattern repeats with interface conditions. Shaft runout at the mating assembly, harness routing clearances, torque access for the fastening tool, EMI from a neighbouring module two metres away. These are all real requirements of the product in its system context, and none of them appear automatically on a component drawing. Someone must deliberately ask the question at input stage — with quality's prompting.
Build a personal checklist of requirement categories: functional, performance, environmental, interface, regulatory, safety, manufacturability, serviceability, packaging, end-of-life. Run it against the input document of your next new programme. The gaps you find in an afternoon will exceed every nonconformance your lines produced that week.
What Quality Should Actually Do About It
First, get invited to design reviews — formally, with sign-off authority, not a courtesy seat. Your contribution is not opinion on design solutions; it is challenge on requirement completeness, testability and verification coverage. Ask for the acceptance criterion behind every input. If the answer is "engineering judgement", that requirement is untestable today and undefendable in a dispute tomorrow.
Second, audit the traceability matrix on a fixed cadence, the way you audit calibration. Sample ten requirements, follow each to its test report, and check the report's result against the stated criterion. Then check the reverse direction: sample five test reports and find the requirement each one verifies. Bidirectional sampling catches the matrix that looks complete but is populated with plausible fiction.
Third, feed production knowledge backwards. Your nonconformance history, supplier escapes and warranty data are a goldmine of unwritten requirements for the next generation of the product. When a field failure cannot be traced to any specification, capture it as a candidate design input for the successor programme. Close the loop formally; most organisations let this intelligence evaporate inside the corrective action paperwork.
Two audit postures toward design controls
Verifying what exists
- Confirm every stated requirement has a method and a result
- Accept the input set as given by engineering
- Review the matrix before customer audits only
- Treat design reviews as engineering's meeting
Interrogating completeness
- Challenge the input set against environment, interface and regulatory categories
- Demand acceptance criteria, not engineering judgement
- Audit the matrix bidirectionally on a fixed cadence
- Hold sign-off authority at design review gates
The Cost of Learning This Late
When an escape traces back to a missing input, the conversation with the customer changes character entirely. You cannot demonstrate compliance, you cannot demonstrate non-compliance, and the burden falls on you. Sorting, containment, requalification and negotiation all follow, none of them cheap. The design organisation that skipped the input discipline is rarely the one holding the cost.
Contrast that with the discipline itself: an input review meeting, a maintained matrix, a bidirectional audit. Modest effort, boring work, invisible when it succeeds. That is precisely why it gets skipped — and precisely why manufacturing quality managers, who inherit the consequences, must understand it and insist on it.
The requirement you cannot test is not a philosophical curiosity. It is the next field failure, currently sitting in a meeting minute that nobody wrote down. Your job is to find it while it is still a blank line in a document, not a cracked part in a customer's hands.