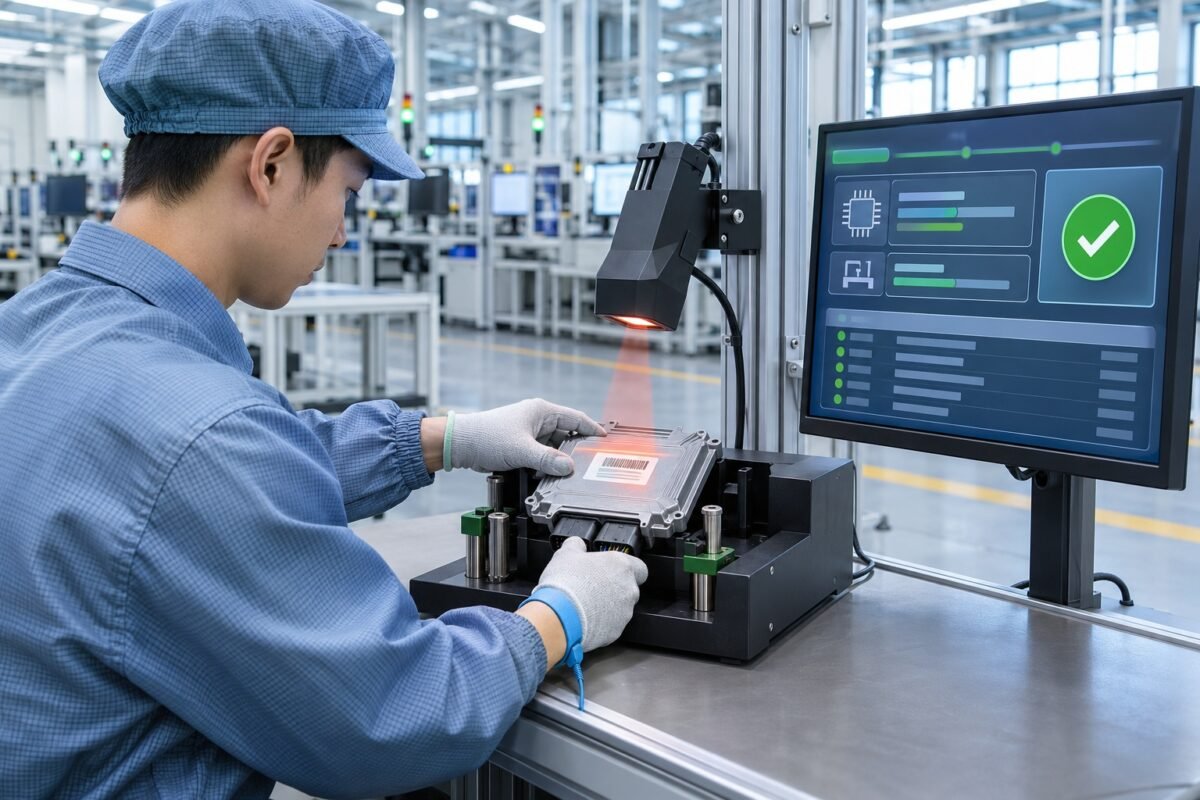
I have stood at more than one containment table with a rejected control module in front of me, only to find the paperwork immaculate. Part number matched the drawing, label matched the part number, shipping documents matched the label. What nobody could say was which firmware was actually inside the unit. The gap between a product's physical identity and its software identity is one of the most under-controlled characteristics in modern manufacturing.
The traditional part number describes hardware: housing, board revision, connector, winding. Firmware changes far more often, sometimes several times within a single production week. If your part number does not encode, or at minimum link unambiguously to, the firmware version it contains, your traceability chain has a hole exactly where the product's behaviour is defined. Two units with the same label can behave differently on the customer's bench, and your 8D team will spend days establishing what should have taken minutes.
Worse, the hole is invisible during audit. A traceability review checks label against BOM against build record; if the build record says nothing about software, the review passes. The failure surfaces in the field, when a customer flashes a different variant or an engineer queries a unit and gets a checksum nobody recognises. By then the evidence trail has gone cold.
The Part Number Must Tell the Truth About Software
The first fix is conceptual: treat firmware as a characteristic of the part, as real as a torque value or a plating thickness, and give it the same identification discipline. That means the released image record for a given part number carries a defined checksum, and every unit's build record references the image it actually received. Whether the linkage lives in the part number itself, in a dash-level suffix, or in the cycle log keyed to the serial number matters less than that it is unambiguous and survives the audit.
Where a hardware part number carries multiple firmware variants, the variant decision must be locked to the order. The build record, the label and the image record must agree before the cycle starts, not be reconciled afterwards by an engineer reading three spreadsheets. Plants that leave variant selection to operator choice eventually ship the wrong variant; the only question is whether they discover it at final inspection or at the customer.
This linkage is also what makes field actions affordable. When a firmware defect surfaces, the affected population is defined by image version, not by hardware lot. Without the serial-number-to-checksum link, a recall scope defaults to everything, which is the most expensive answer available.

Programming Station Control: The Line's Most Dangerous PC
The programming station deserves more scrutiny than almost any other station, yet in most plants it is treated as a commodity operation: someone loads a hex file onto a desktop PC, plugs in the fixture and presses go. Control must be established over four things: which image the station is permitted to run, who can change that permission, how a change is proven, and what happens when the station loses network connection mid-shift.
The failure modes are mundane and repetitive. An engineer copies a hex file to the desktop because the image server was slow, and the copy lingers for weeks. A technician pulls from a network share that someone reorganised, silently falling back to an old local cache. The programmer software has a last-used-file default nobody disabled. Each has caused real escapes in plants I have audited. Each is prevented by removing local storage as an option and forcing the station to pull from a single controlled source, with the pull logged.
Physical control matters as much as logical control. The fixture itself contains firmware — the programmer, the adapter board, sometimes even the USB hub. A station validated in January can behave differently after a fixture swap in March, and the swap appears in no change record. Treat the fixture configuration as a controlled characteristic with its own identification, and record it in the cycle log alongside the image checksum.
Controlled programming cycle
- 01Pull imageStation fetches from the single controlled source; local storage disabled
- 02Verify sourceChecksum of loaded image compared against released image record
- 03Enforce variantLabel scan routes the image; operator cannot select it manually
- 04Program and read backTarget's reported version and checksum compared to the same record
- 05Log the cycleSerial number, checksum, fixture ID, result and timestamp to a controlled store
Checksums, Not File Names
File names are not identification. The FINAL_new.hex joke has circulated through every industry, and I have seen variants of it at aerospace suppliers who should know better. The only defensible identity for a firmware image is its cryptographic checksum — SHA-256 where infrastructure supports it, at minimum a CRC-32 plus file length. The checksum is what the station verifies before programming, what the cycle log records, and what ties the serial number to the software it carries.
Make verification active, not documentary. The station should compute the checksum of the image it actually loaded into memory and compare it against the released record. After programming it should read the image back from the target — or at minimum the version identifier and checksum the target self-reports — and compare again. Read-back verification is the last line of defence against marginal flash writes, wrong-variant programming and interrupted transfers.
Measure the station like any other process. Checksum match rate, read-back failure rate, programming time distribution, and units programmed per image version per shift. A shift in programming time often signals a station pulling a different image size than intended. Review the image version histogram daily; a version that should have ended Tuesday appearing on Thursday is a control breakdown, and you want to find it in the data rather than in a customer complaint.
Bidirectional Traceability: Serial to Software and Back
Firmware traceability means one thing: given a serial number, you can state within minutes the exact image programmed, the station, the fixture, the operator and the timestamp — and given an image version, you can list every serial number carrying it. Both directions must work. Most plants manage the forward direction; the reverse direction, which is what a field action demands, is usually missing.
The mechanism need not be exotic. A station cycle log, written to a controlled location, containing serial number, image checksum, fixture ID, result and timestamp, joined to the existing build record, is sufficient. What is not sufficient is a paper traveller with a tick box reading programmed, or a log on the station's local drive that is wiped when the PC is re-imaged. I have watched both destroy a field investigation.
Handle variants through enforcement, not vigilance. Route the variant decision through the order, through the label, through the scanner that reads the label, so the station physically cannot select the wrong image for the unit in the fixture. Where operator selection is genuinely unavoidable, force a second independent check — scan the label, compare the encoded variant code against the selected image, stop the cycle on mismatch.
Software is a characteristic of the part, as real as a torque value or a plating thickness, and it deserves the same control.
Field Updates: When the Line and the Field Diverge
Field firmware updates have become routine, and they quietly break the assumption that the build record describes the product in service. A unit leaves the line with image A, is updated at a dealer or over the air to image B, and two databases now disagree about what is inside it. Neither is wrong; they describe the unit at different times. If your traceability system has no concept of software state over time, every field return becomes an argument.
The risks concentrate in three places. Update integrity: a field update that fails midway can leave a unit in an undefined, partially written state. Variant discipline: an update applied to hardware it was never validated for — a board revision with a different memory part, say — can brick the unit. Rollback blindness: a unit updated, reverted and updated again has a history your system must capture, because the failure may correlate with the update event, not the final version.
The discipline required in the field is the same as on the line. The update mechanism logs serial number, source version, target version, result and timestamp to a record that survives. The unit reports its version and checksum on demand — over diagnostics, on a label reprint, whatever the interface allows — so a returned unit can be interrogated rather than argued about. And the compatibility matrix between hardware revisions and firmware versions must be a controlled, versioned document, not folklore in an engineer's head.
Documented traceability versus real traceability
What most plants have
- Build record says 'programmed', no image identity
- Cycle log stored on the station's local drive
- Variant chosen by operator from a dropdown
- No record of field updates after shipping
What a mature system delivers
- Checksum against serial number, retrievable in minutes
- Central controlled log surviving PC re-imaging
- Variant enforced by label scan, wrong image physically blocked
- Update history per unit, including reverts and failures
Auditing the Software Chain Without Being a Software Engineer
You do not need to write firmware to audit its control. Start with the image source: show where released images live, who can write to that location, and the record proving this checksum was released for this part number. Then go to the station: disconnect the network and observe what happens; check whether a local image can be selected; pull the last twenty cycle logs and confirm the image versions match what production planning says should have run that week.
Traceability is tested by challenge, not by document review. Pick three serial numbers from finished goods at random and demand the software identity of each. Then name a firmware version and demand the affected serial range. Time both exercises. If the first takes an afternoon and the second is impossible, you have measured your real capability — and it will be a sobering number in hours, not the minutes a mature system delivers.
Finish with the boundary conditions. Ask what happens when a programmer fails mid-write and the unit is reworked, and how reprogrammed units are distinguished from first-pass units in the records. Ask who is authorised to load a special image for engineering trials and how those units are prevented from shipping. Every plant I have audited has an engineering-image loophole; the good ones know about theirs and have fenced it.
Building the Discipline In
None of this requires new technology. It requires deciding that the desktop PC with a hex file on it is no longer acceptable. Decide where the golden image lives, force every station to draw from it, record the checksum against every serial number, verify by read-back, and extend the same chain through every field update. Each element is a standard quality-engineering control applied to a characteristic that happens to be software.
Where to start from nothing: inventory every device in your product line that contains firmware, including the ones inside fixtures and tools. For each, establish the current image and how it is controlled. Fix the production programming stations first, since they generate the population, then the field records. Then reconcile the two periodically — sample finished goods and field returns, read their self-reported versions, and compare against the database.
That reconciliation, done monthly, tells you more about your real software control than any audit checklist. The uncomfortable truth is that hardware traceability matured decades ago, while software traceability is still maturing in plants that would never ship an unlabelled mechanical part. Close the gap and most firmware quality mysteries — the unit that worked when it left here, the variant that somehow shipped to the wrong market — resolve into ordinary, preventable process failures.
The numbers that matter at the station