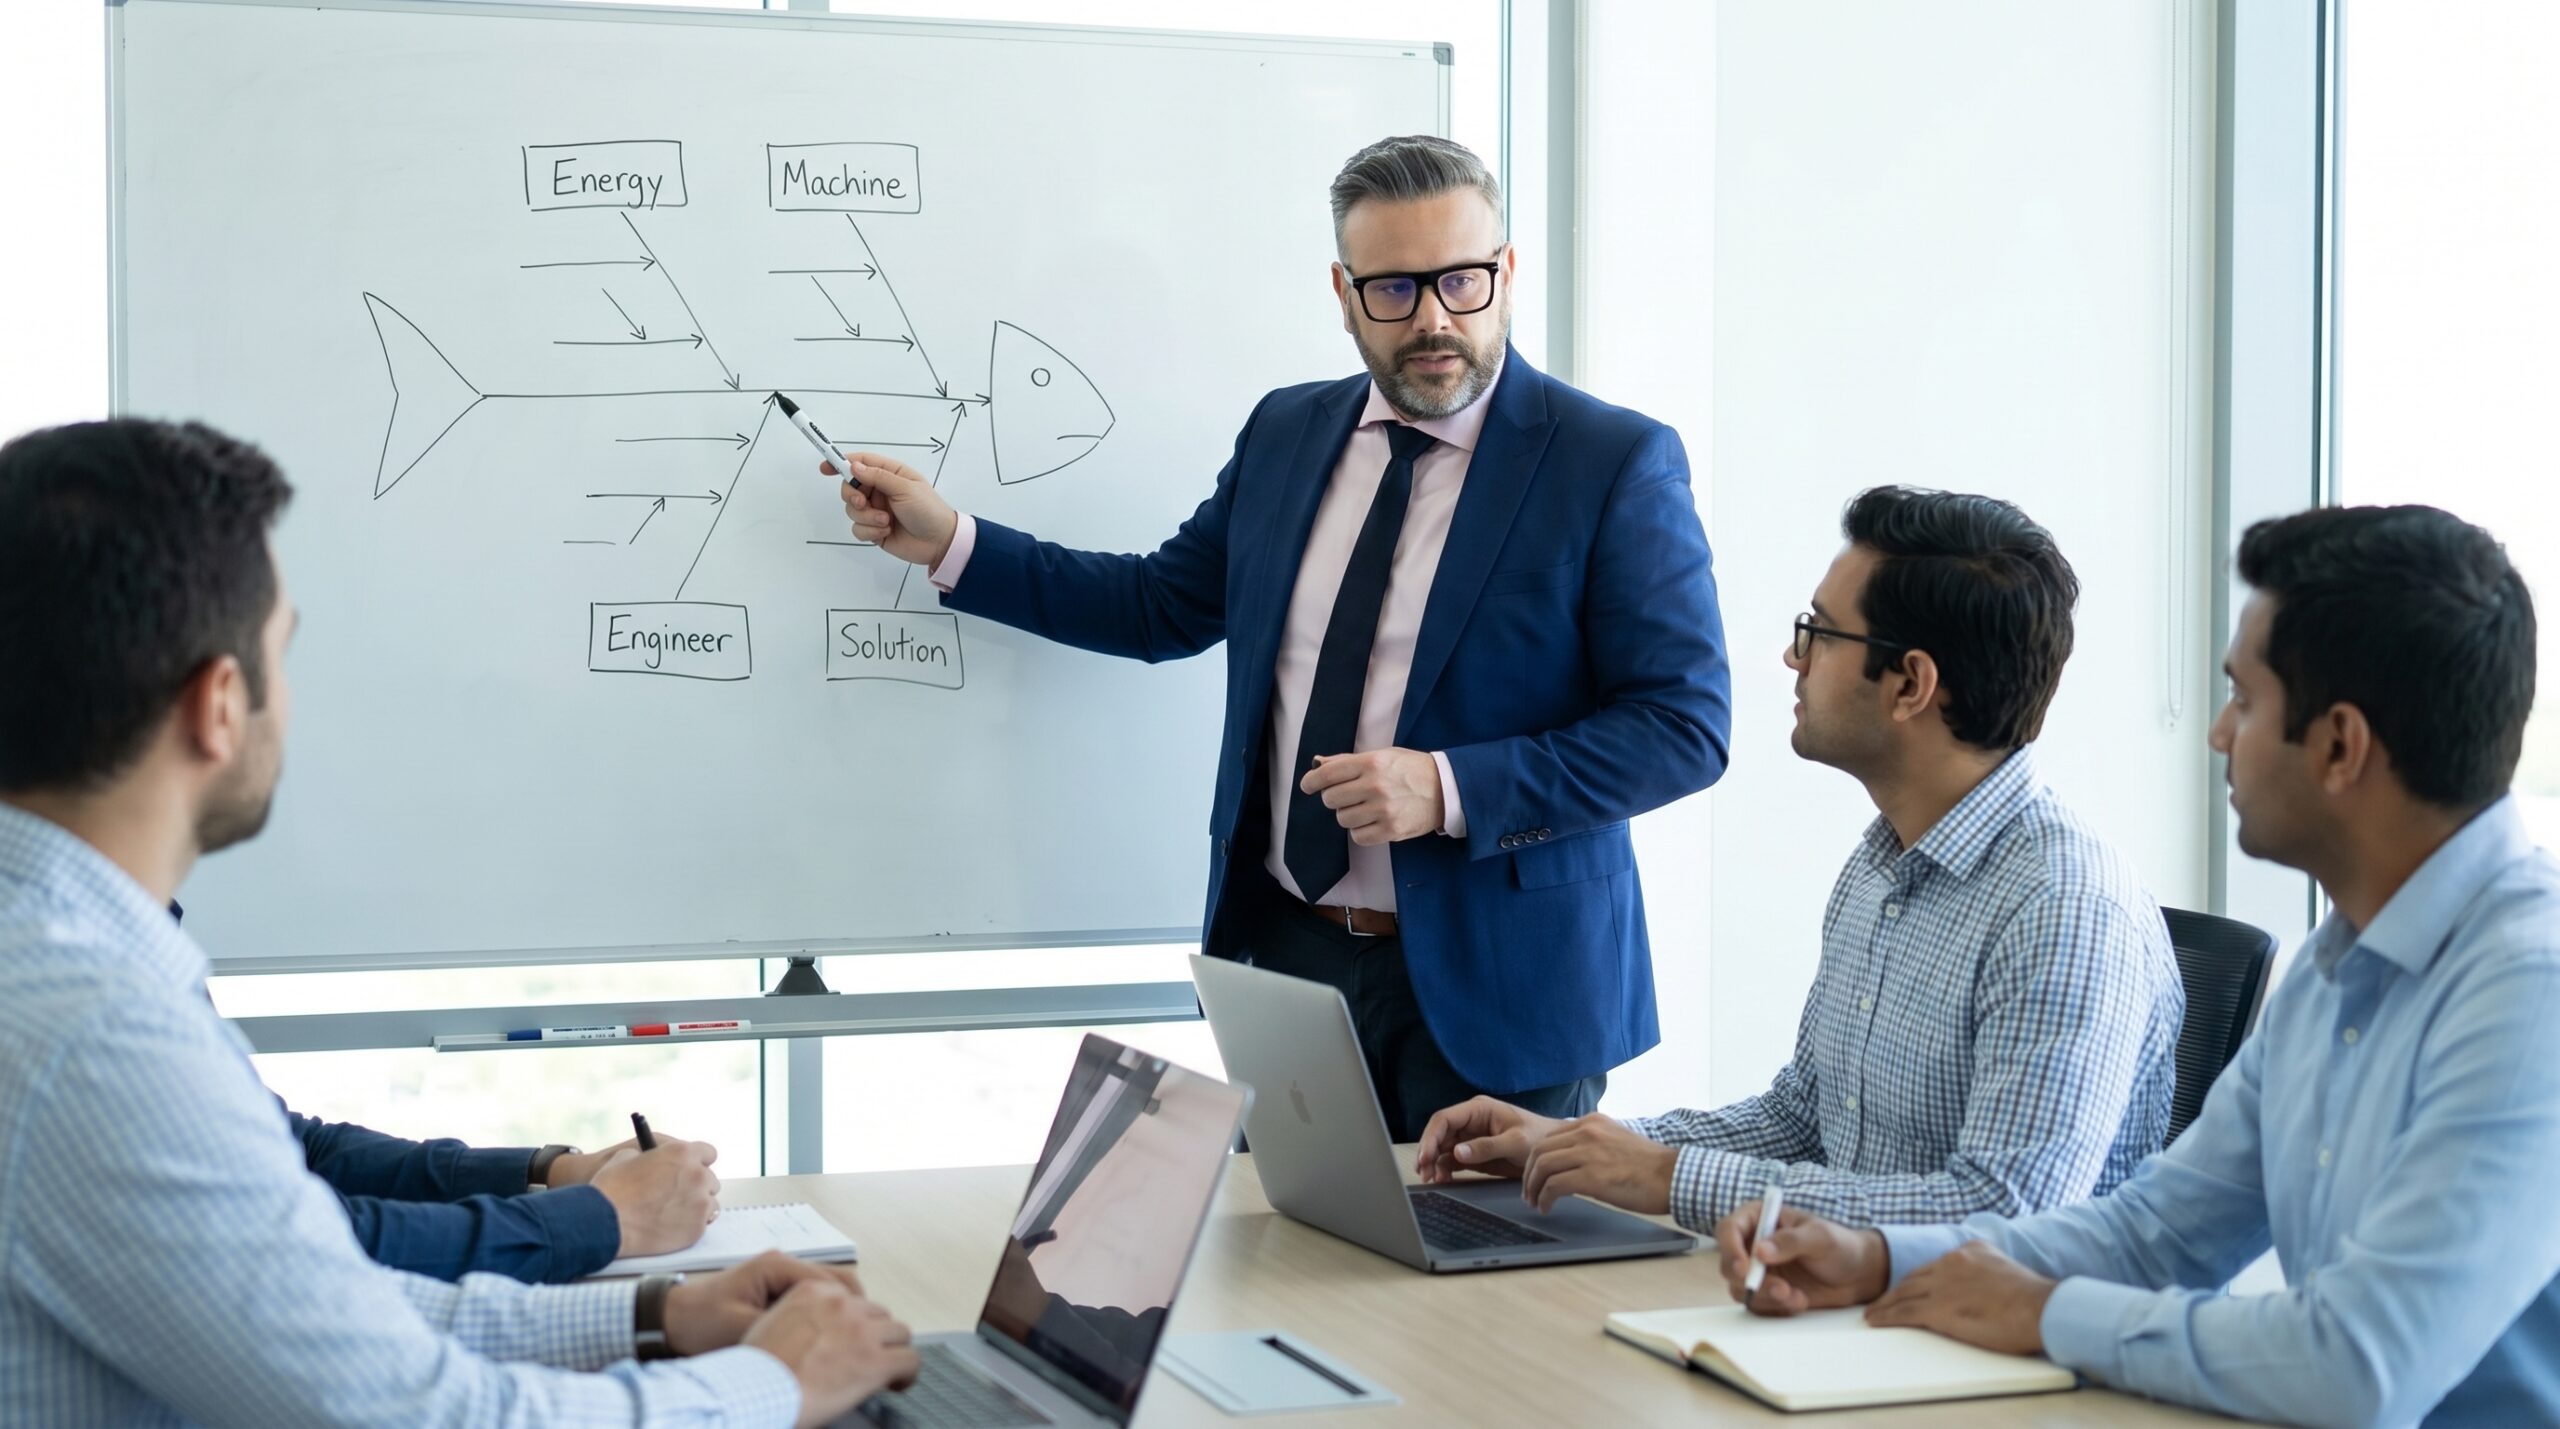
When a defect escapes to the customer, the first instinct in many plants is to escalate. Teams launch Six Sigma projects, call external consultants, and build complex statistical models. I have audited dozens of facilities across automotive and aerospace, and the reality is that eight out of ten manufacturing problems do not require advanced statistical tools. They require discipline.
The Ishikawa diagram, or fishbone diagram, provides the structural framework to map potential causes. The 5 Whys technique provides the drilling mechanism to reach the systemic root cause. Used independently, they often fail. Used together, they form a complete, rapid resolution methodology that satisfies IATF 16949 and AS9100 corrective action requirements without wasting engineering hours.
The failure is rarely in the tools themselves. The failure is in the execution. Engineers write 'operator error' on a fishbone, ask 'why' twice, and close the 8D report with a retraining action. The defect returns within a month because the systemic gap remains untouched.
The Ishikawa Framework: Mapping the Problem Space
The Ishikawa diagram forces a cross-functional team to visually map all plausible causes before selecting a direction. The 'head' of the fish states the problem effect. The major 'bones' categorise the contributing factors. In a manufacturing environment, these categories follow the 6M structure: Man, Method, Machine, Material, Measurement, and Milieu (Environment).
Problem definition is where most root cause analyses fail. A team cannot effectively brainstorm causes against a vague statement like 'we have too much scrap.' The problem head must specify the defect, the location, the magnitude, and the timeframe.
A weak definition produces generic causes. A strong definition forces specificity. Compare these two approaches to framing the same issue before a team even enters the room.
Problem Statement Quality
Weak statement
- Generic symptom with no quantification
- No process or station identified
- No timeframe or trend data referenced
- Leads to broad, unfocused brainstorming
Strong statement
- Specific defect type and dimension named
- Exact operation and machine number cited
- Reject rate quantified against a baseline
- Forces targeted, data-driven cause analysis
For service or administrative processes, the 6M categories shift to 4P: Policy, Procedure, People, and Technology. This ensures the diagram remains relevant whether the process involves machining a turbine blade or processing a purchase order.
Running an Effective Brainstorming Session
The composition of the team matters as much as the structure of the diagram. You need four to eight people maximum. The room must contain the operator who runs the process daily, the process engineer, the maintenance technician, and the quality engineer. A supervisor who only reads reports adds no diagnostic value here.
The facilitator works through each of the 6M categories systematically. For every bone, the team asks what conditions in that category could produce the defined effect. The goal is volume, not immediate validation. A typical session generates twenty to thirty potential causes across the six categories.
Once the diagram is populated, the team applies a reality filter. They narrow twenty potential causes down to the top three to five based on existing data, maintenance logs, and operator knowledge. Only these top candidates move forward to validation.
Validating Causes Before Asking Why
Jumping straight into 5 Whys without validating the Ishikawa shortlist is a common trap. If you pursue a non-causal factor through five layers of questioning, you build a logical chain to the wrong conclusion. Verification must happen first.
If 'uncalibrated micrometer' is listed under Measurement, check the calibration database before running a 5 Whys on it. If the gage was calibrated yesterday, cross it off the list. If the maintenance log shows Machine 3 was down three times last month for spindle issues, that cause moves to the top of the queue.
This filtering step prevents engineering teams from wasting days chasing hypothetical causes. It anchors the subsequent 5 Whys analysis in operational reality rather than speculation, ensuring that the drilling effort targets a genuine process failure.
The 5 Whys: Drilling to Systemic Root Causes
The 5 Whys technique interrogates a validated cause by repeatedly asking 'why' until the team reaches a systemic breakdown. The number five is a guideline, not a rule. Some chains resolve at three; others require seven. The stopping point is the systemic failure, not an arbitrary count.
Consider a customer rejection of 200 parts for a dimensional deviation. The tool was worn. It was not replaced on schedule. The maintenance plan was not updated for a harder material grade. Engineering did not trigger the update when the material changed. The systemic root cause: no formal cross-functional link exists between the Engineering Change Notice process and the maintenance planning system.
The corrective action is not 'retrain the operator' or 'discipline the maintenance planner.' The corrective action is updating the ECN procedure to mandate a maintenance plan review. This closes the systemic gap permanently.
Root cause is always systemic. 'The operator forgot' is a symptom of a process that relies on memory instead of poka-yoke.
A properly executed 5 Whys chain should never terminate at an individual. If the analysis ends with 'the operator was not trained,' ask why the training system allowed an uncertified operator to run the process. The answer always points to a management system, a procedure, or a resource gap that management controls.
Integrating the Tools into a Unified Process
Ishikawa provides the breadth. The 5 Whys provides the depth. Combining them creates a methodology that satisfies the most stringent customer-specific requirements in IATF 16949 environments. The sequence is fixed: map, filter, drill, solve, verify.
The Combined RCA Sequence
- 01MapBuild the Ishikawa diagram to generate all plausible causes across the 6M categories.
- 02FilterNarrow to the top 3 to 5 causes using existing data, maintenance logs, and calibration records.
- 03DrillRun a 5 Whys analysis on each validated top cause to reach the systemic breakdown.
- 04SolveDefine and implement corrective actions that address the systemic root cause directly.
- 05VerifyConfirm effectiveness through monitoring data over a defined production volume.
This sequence works because it separates divergent thinking from convergent analysis. The Ishikawa session expands the problem space, preventing premature fixation on a single explanation. The filtering and 5 Whys stages then contract that space, applying rigorous logic to identify and resolve the actual failure point.
In a customer complaint scenario, this combined approach feeds directly into the 8D methodology. Ishikawa and 5 Whys define the content of D4 (Root Cause). The output of the 5 Whys directly dictates D5 (Corrective Action) and D6 (Implementation). The tools are not standalone exercises; they are the analytical engine of the formal corrective action report.
Selecting the Right Tool for the Failure
Not every problem requires the full combined sequence. For a straightforward failure with an obvious mechanism, running a full Ishikawa session wastes time. A team that understands the failure path can move directly to 5 Whys to confirm the systemic driver.
However, for recurring problems, safety incidents, or complex customer escapes involving multiple variables, the combined approach is mandatory. If a defect has appeared before and the previous 8D closed it, the original analysis missed the root cause. Returning to the Ishikawa diagram with a fresh team often reveals a category that the first investigation ignored entirely.
| Situation | Primary tool | Why |
|---|---|---|
| Recurring customer escape | Ishikawa + 5 Whys | Previous RCA failed; requires full remapping of all 6M categories |
| Clear single-point failure | 5 Whys only | Mechanism is understood; drilling directly to the systemic cause is faster |
| Process improvement initiative | Ishikawa only | Goal is idea generation, not defect resolution or systemic correction |
| Safety or critical quality event | 8D with Ishikawa + 5 Whys | Maximum rigour required for formal documentation and traceability |
The discipline lies in resisting the urge to over-engineer simple problems while refusing to shortcut complex ones. A team that pulls out a flipchart and runs a disciplined Ishikawa session will outperform a team that hides behind statistical software every time.