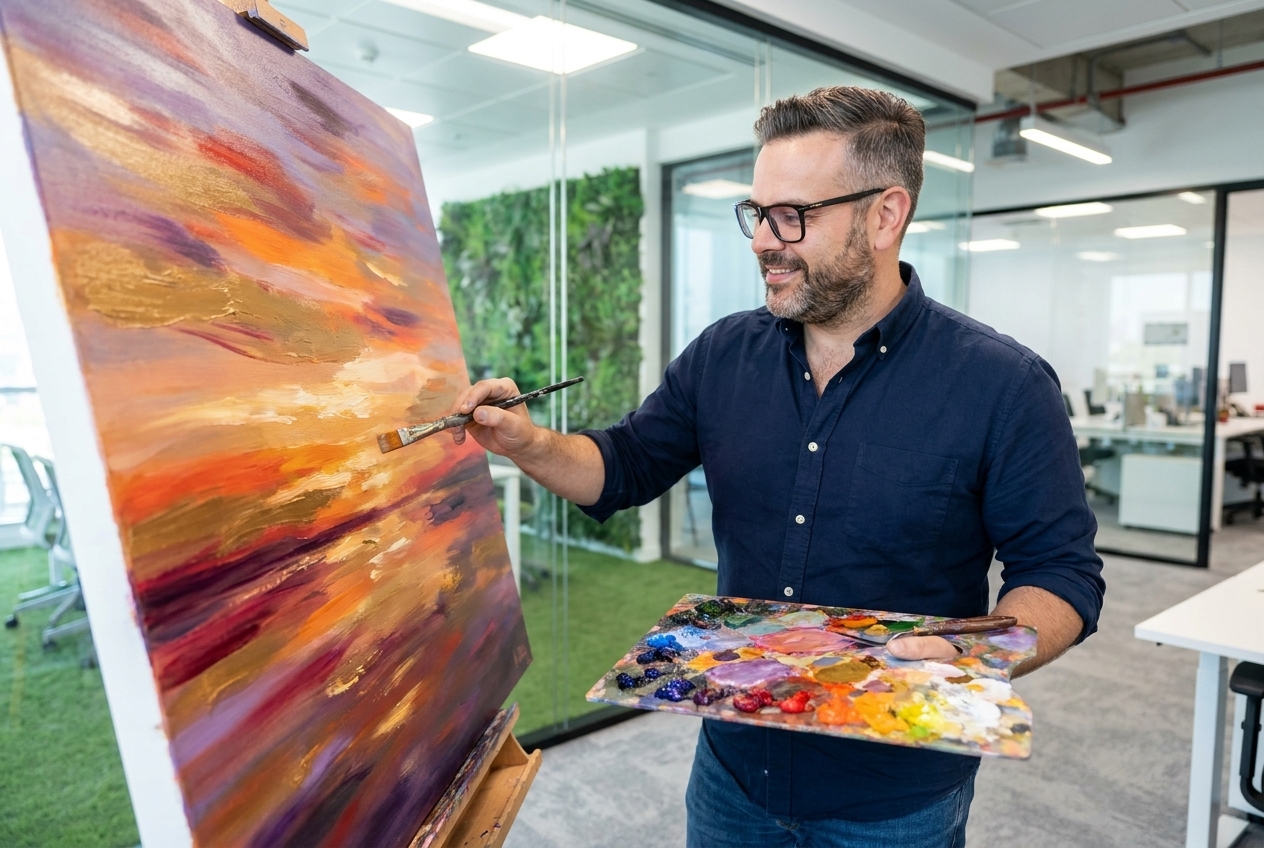
At Mirka s.r.o., I set up a canvas and acrylics in the office to test a hypothesis about team dynamics. The exercise was not about art. It was a diagnostic tool to observe how cross-functional colleagues communicate when the rigid constraints of their daily ISO 9001 routines are removed. What transpired over three hours provided more actionable data on our organisational culture than any internal employee satisfaction survey.
The structured business environment and free-flowing problem solving are not opposites; they are required partners in continuous improvement. In my experience transitioning quality management systems at a major aerospace manufacturer and SNOP, the most dangerous defects occur when operators and office staff become disconnected from the physical reality of the product. An activity that forces shared, tangible observation breaks down these invisible silos.
When people who only interact through ERP systems and emails are forced to make a real-time, collective decision, the cracks in communication become immediately visible. The painting session revealed exactly who initiates, who defers, and who rigidly controls the workflow. For a quality director, these behavioural patterns directly mirror how nonconformances are handled during a live production shift.
Diagnosing Communication Silos Through Shared Observation
I cleared a space near the windows and simply began applying paint to a canvas. Within twenty minutes, colleagues from accounting, logistics, and human resources had spontaneously gathered. This rapid assembly is exceptionally rare in a standard office layout, where departments are physically and procedurally walled off. The speed at which people abandoned their screens indicated a latent desire for shared, physical engagement.
As the composition developed, the cross-functional dynamic shifted. Logistics suggested adding an anchor element to the centre; HR recommended adjusting the colour balance. They were actively applying cross-functional problem-solving skills to a tangible object. In a manufacturing context, this is exactly the collaborative behaviour required during an 8D root cause analysis, yet it rarely emerges organically in a meeting room.
The exercise proved that titles and departmental boundaries dissolve when people are focused on a shared, physical outcome. The accounting team debated spatial logistics with the same intensity they usually reserve for budget variances. By temporarily stripping away the standard reporting structure, we unlocked a communication efficiency that standard matrix management consistently fails to achieve.
Calibrating the Cost of Unstructured Inputs
While the collaborative spirit was impressive, the physical output of the painting exposed a critical quality failure: uncontrolled inputs. Everyone was permitted to add a brushstroke. Because there was no standard procedure or clear acceptance criteria for these additions, the final composition suffered from dimensional and visual defects.
The proportions were visibly distorted, and colour transitions were rough. In quality engineering, this is the exact equivalent of allowing uncontrolled process modifications on a production line. When you permit operator adjustments without updating the PFMEA or control plan, you guarantee process drift. The painting session inadvertently demonstrated why strict management of change is non-negotiable.
There is a direct parallel to nonconformance management. The flaws in the canvas were not caused by a lack of effort; they were caused by a lack of specification. We allowed enthusiastic contributions without defining the tolerance limits. In a plant running IATF 16949, enthusiastic but uncontrolled adjustments on the floor are the primary driver of scrap and rework costs.
Impact of Uncontrolled Process Inputs
The Illusion of Productivity in Unstructured Time
The session required three hours. During this period, standard administrative workflows were entirely suspended. From a strict OEE perspective for the office environment, this looks like catastrophic downtime. However, evaluating this activity purely on lost transactional output misses the long-term systemic value of breaking departmental barriers.
At a major aerospace manufacturer, I implemented Routing Verification KPIs that cut internal lead time by 97%. That success was not achieved by keeping people at their desks processing standard work. It was achieved by fundamentally changing how cross-functional teams interacted with the product flow. Sometimes you must deliberately inject controlled downtime to realign the entire system.
The painting exercise functioned as a system reset. It forced logistics, accounting, and HR to understand the spatial and physical constraints of the value stream. When they return to their digital tools, their decision-making will be calibrated by a shared physical reality. This reduces the friction that causes massive delays in engineering changes and supplier approvals.
Applying First-Pass Yield Logic to Creative Output
The final painting was honest, but it was not a first-pass yield success. The process required significant rework, scraping, and layering to manage the accumulated defects. This mirrors the reality of new product introduction. You rarely achieve zero defects on the first run of a complex assembly. The value lies in how quickly you identify and contain the variation.
I used a palette knife to scrape away and restructure areas where the uncontrolled inputs had caused visual nonconformances. This is manual rework. In a lean manufacturing environment, we want to eliminate rework entirely by building quality into the process at the source. The painting proved that without poka-yoke mechanisms, defect correction becomes the dominant activity.
Quality leaders must recognise this dynamic on their own shop floors. When you see a high volume of rework, you are looking at a process that lacks structural control. The enthusiasm of the operators is not enough to guarantee conformity. You must engineer the workstation and the procedure so that the defect cannot physically occur.
Enthusiastic contributions without defined tolerance limits guarantee process drift.
Translating Behavioural Metrics to the Shop Floor
The most critical takeaway from this exercise was behavioural. Colleagues who never speak on the floor were actively debating geometry and material properties. This level of engagement is the Holy Grail of operational excellence. If you can transfer this specific collaborative energy to the management of your AS9100 or VDA 6.3 systems, your audit performance will transform.
When I built the greenfield QA/QC department at SNOP for a 900+ employee plant, the primary challenge was not writing procedures. The challenge was convincing experienced operators to report near-misses without fear of punishment. The painting session showed me that people will aggressively collaborate on problem-solving if you provide a neutral, non-punitive environment.
The canvas now hangs in the lobby as a visual control. It is a permanent reminder that our systems are only as strong as the human interaction supporting them. Every time a visitor asks about it, the answer is a lesson in collective ownership. It is a physical representation of what happens when a team drops its functional boundaries and focuses purely on the quality of the output.
Engineering the Conditions for Engagement
You cannot simply mandate collaboration and expect improved MSA results or better Cpk values. Engagement must be engineered into the daily work environment. The painting session worked because it provided a clear, tangible objective and removed the fear of failure. Quality directors must replicate these conditions on the production line.
Evaluate your current Gemba walks. Are operators actively discussing process improvements, or are they merely defending their work to the auditor? If your floor lacks the spontaneous collaboration I witnessed around the canvas, your management system is failing. The ISO 9001 standard requires continual improvement, which is impossible without baseline human engagement.
Operational Engagement Maturity
- Siloed ComplianceDepartments work to their own KPIs, passing defects downstream without communication.
- Reactive CollaborationCross-functional teams interact only when a major nonconformance halts production.
- Structured Problem SolvingRegular 8D and kaizen events drive improvement, but participation feels obligatory.
- Integrated OwnershipOperators and support staff spontaneously collaborate on quality the moment variation occurs.