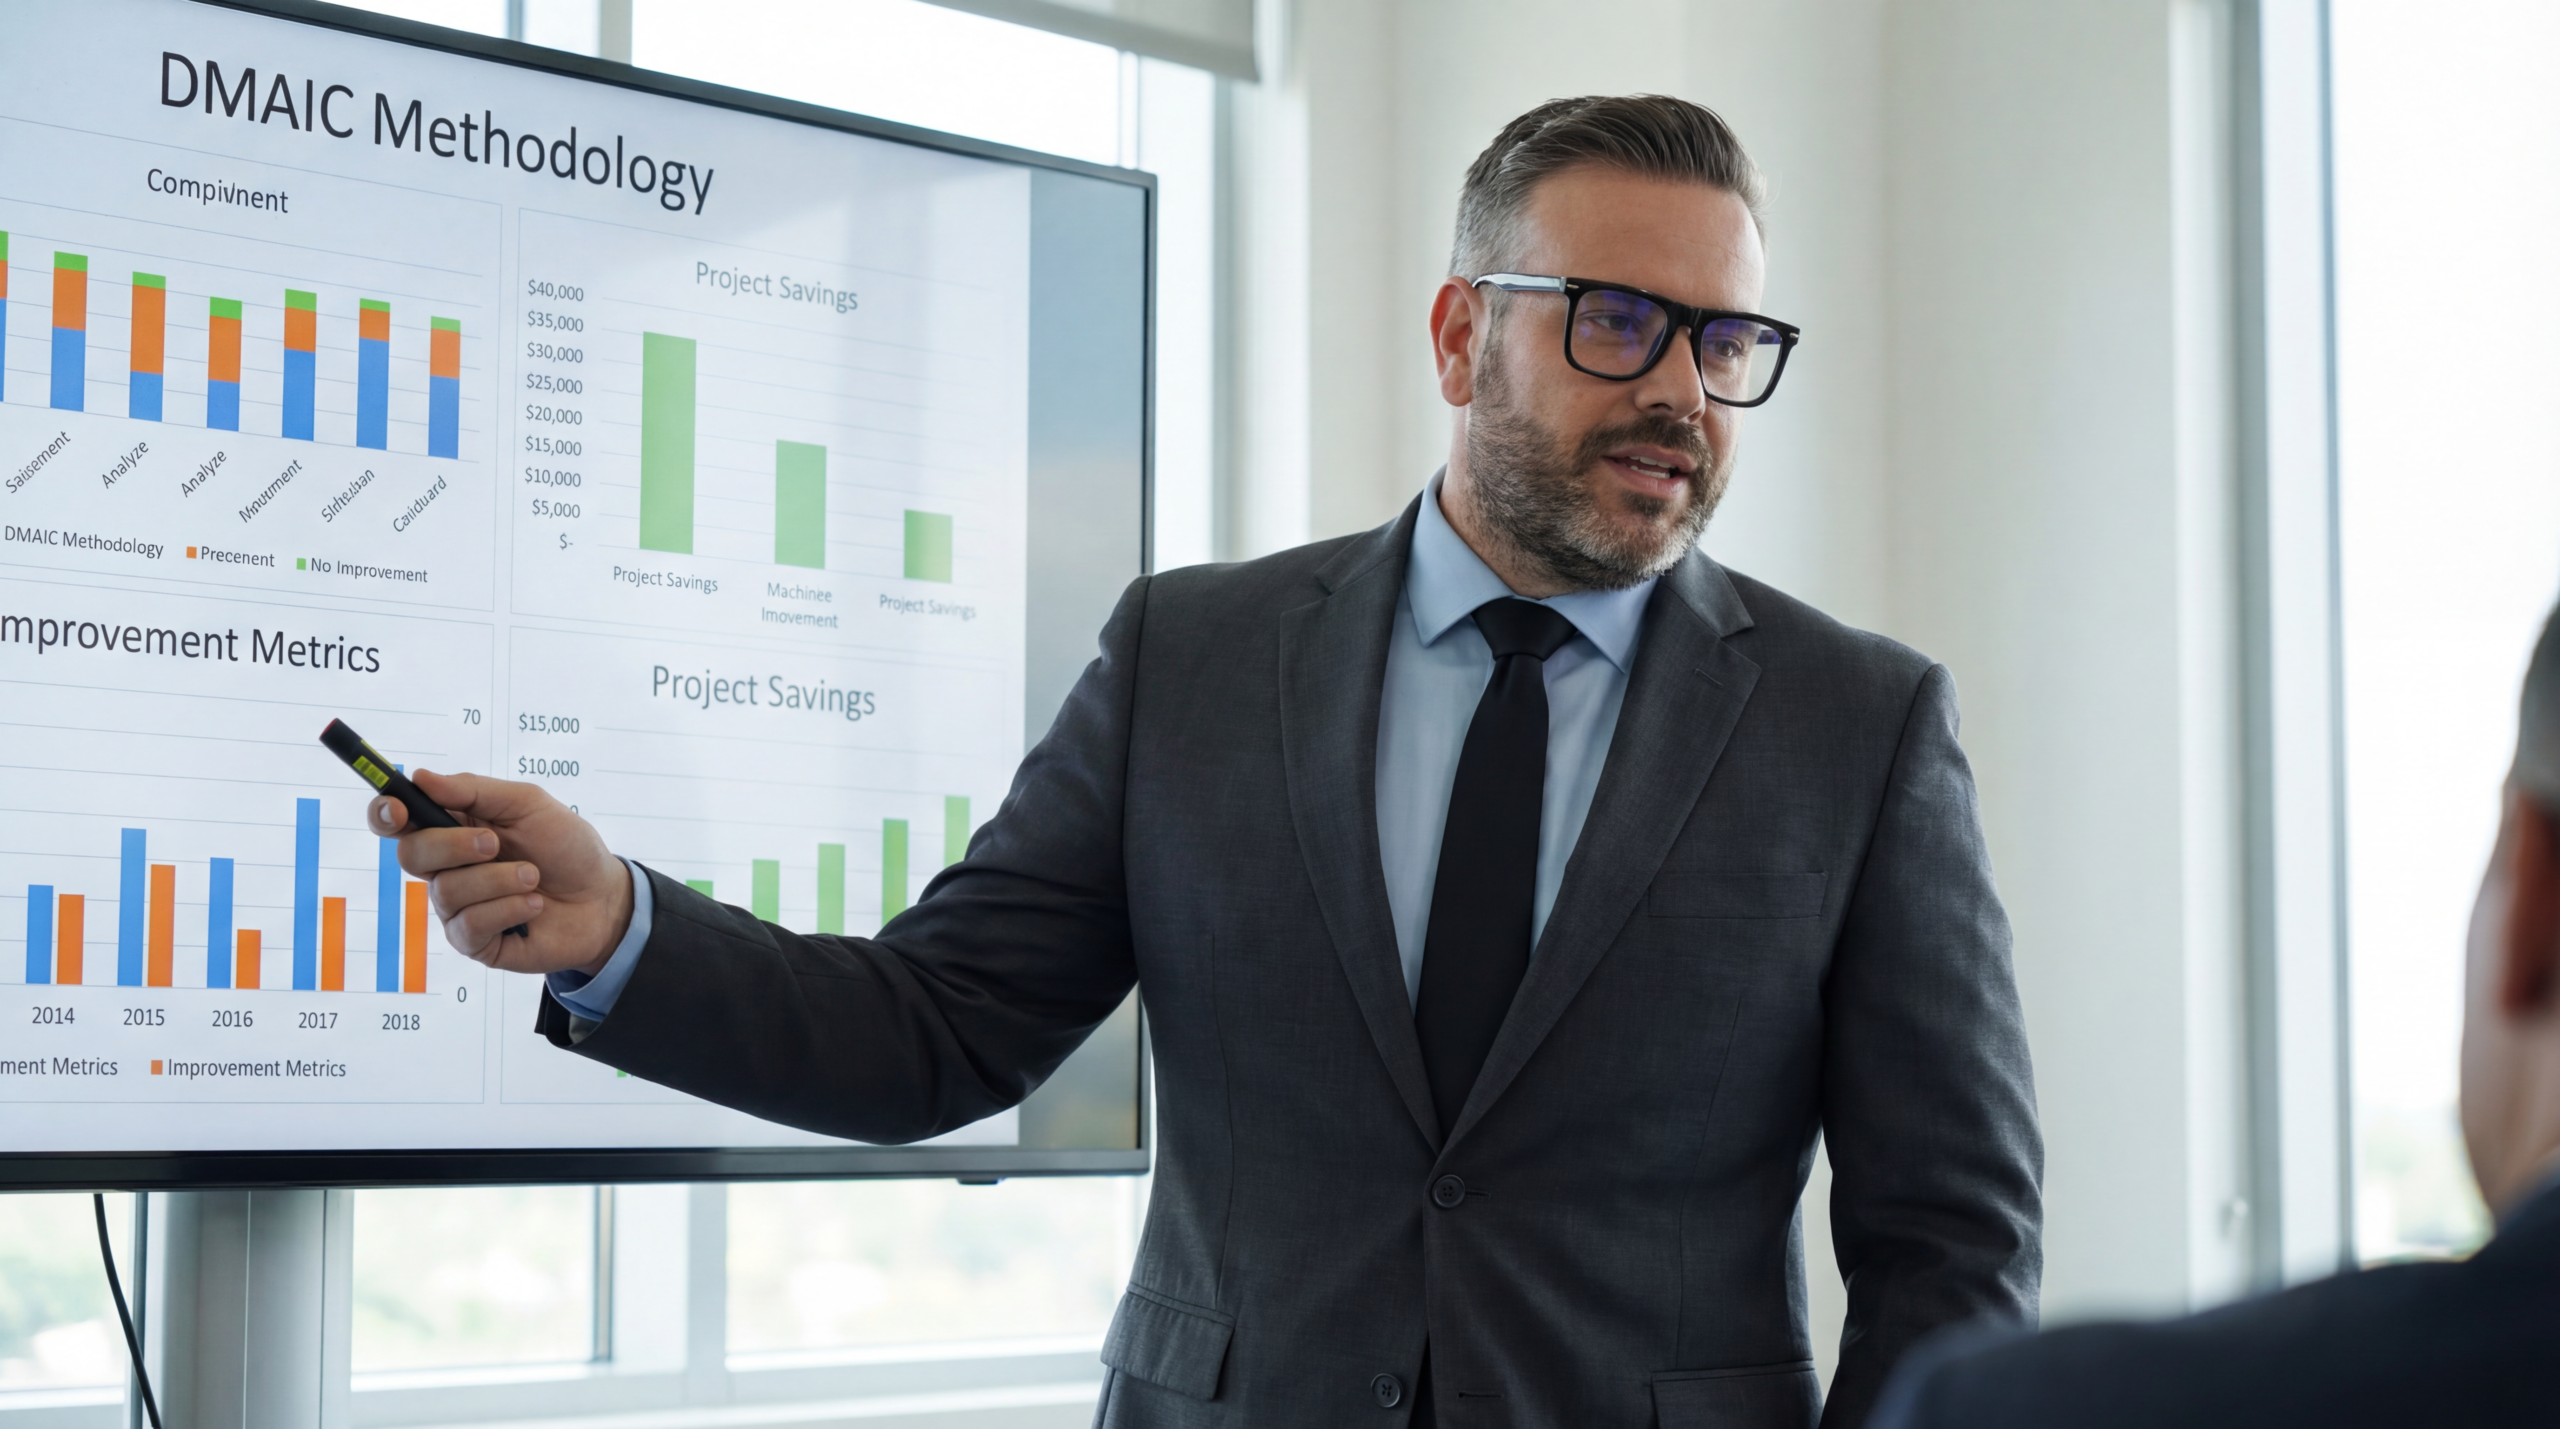
When a production line runs at a 12% defect rate, the reaction is almost always the same: a cascade of unstructured fixes, replaced machine settings, and ad-hoc operator interventions that temporarily mask the symptoms without addressing the cause. I have walked into plants exactly like this. The scrap costs accumulate, customer complaints escalate into formal warnings, and the production team loses confidence in its own measurement systems.
Six Sigma DMAIC — Define, Measure, Analyse, Improve, Control — is the mechanism that breaks this cycle. It forces a manufacturing organisation to replace intuition with measurement, and scattered corrective actions with validated root-cause elimination. It is not a motivational framework; it is a sequential, data-driven protocol that demands evidence at every gate.
The discipline of DMAIC is what separates a controlled process from a chaotic one. Here is how each phase functions in a real manufacturing environment, the specific tools that apply, and the governance required to sustain the gains after the project closes.
Define: Scoping the Problem and Setting the Target
The Define phase establishes the boundaries of the project. Before any data is collected, the team must write a formal problem statement that quantifies the defect rate, ties it to a financial cost, and identifies the specific process or product family affected. A statement like "quality is poor" has no place here. The statement must specify the line, the shift, the defect type, and the annual scrap cost in precise terms.
Stakeholder mapping follows. The project sponsor, line operators, quality engineers, and affected suppliers must be identified and their interests documented. In an IATF 16949 environment, this mirrors the cross-functional approach required for APQP and 8D problem-solving. If the stakeholders are not aligned on the problem definition before the Measure phase begins, the project will fracture when the data reveals uncomfortable truths about specific operations or shifts.
The Define phase concludes with a baseline-to-target gap. For a line running at 12% defects (roughly 2.6 sigma), a realistic six-month target is a reduction to under 3% — a significant shift, but one that moves the process toward an acceptable Cpk threshold. The projected savings, calculated from scrap and rework costs, become the financial mandate for the work that follows.
Measure: Establishing the Baseline with Hard Data
Anecdotes do not survive the Measure phase. The objective here is to instrument the process and collect enough data to calculate a valid capability index. Over a typical four-week collection window, every defect must be categorised by type, timestamped, and mapped to a specific machine, operator, and set of environmental conditions. The granularity matters: without it, the Analyse phase cannot isolate variables.
The critical output of Measure is the process capability study. A Cpk of 0.73 — common on unstable lines — confirms that the process is nowhere near specification and that variation is uncontrolled. A sigma level of 2.6 aligns with the observed defect rate, validating the measurement system itself. If the measurement system analysis (MSA) has not confirmed gauge repeatability and reproducibility, the capability data is invalid and must be retaken.
The Measure data must also expose stratification. In most troubled processes, defects are not uniformly distributed. Typically, 85% of failures cluster on three operations out of twelve, and specific shifts or operators account for a disproportionate share. This concentration is the first evidence that the problem is localised, not systemic — and it directs the analytical effort that follows.
Baseline Metrics from the Measure Phase
Analyse: Isolating the Root Cause Through Validation
Analyse is where hypotheses are structured and tested. The Ishikawa diagram categorises potential causes across Man, Machine, Material, and Method. This is a familiar tool, but its value lies in its completeness — it forces the team to look beyond the obvious machine variables and examine training gaps, supplier material variation, and outdated standard work documents.
The 5 Whys technique drives past the surface symptom to the systemic gap. A geometric mismatch traced through five iterations might reveal not just a calibration error, but a calibration procedure that specifies an annual interval when the process dynamics demand a fortnightly one. Pareto analysis reinforces this: if one machine accounts for 45% of all defects, the corrective action must prioritise that asset before addressing secondary variables.
Crucially, the root cause must be validated empirically, not assumed. In the calibration example, running a controlled experiment — recalibrating at two-week intervals and measuring the resulting defect rate — transforms a hypothesis into confirmed evidence. When the defect rate drops by half during the trial, the root cause is proven. Without that validation step, the Improve phase risks implementing solutions against the wrong variable entirely.
Improve: Structured Implementation with Pilot Validation
The Improve phase deploys solutions in priority order, driven by impact and ease of implementation. The validated root cause determines the primary intervention. In the calibration example, this means rewriting the maintenance procedure to a two-week interval, adding automated system reminders, and training operators to perform pre-shift verification checks on the affected dimensions.
Pilot testing on a single machine or cell is non-negotiable. Rolling an untested change across an entire line risks destabilising the only process that is currently producing. A three-week pilot on the highest-defect machine, with daily defect tracking and operator feedback sessions, provides the evidence needed to justify full-scale deployment. If the pilot reduces the defect rate by 60%, the financial and operational case for rollout is clear.
Full implementation requires coordinated action: deploying the new standard work across all machines, retraining all affected operators, and engaging suppliers to tighten incoming material tolerances. Each action must have an owner and a deadline. Without that accountability, the Improve phase stalls in the gap between engineering and the shop floor.
A process running at 2.6 sigma is not failing everywhere — it is failing at specific points that the data must locate and the team must fix.
Control: Locking in the Gains Through SPC and Governance
Improvement that is not sustained is not improvement. The Control phase institutionalises the new standard through Statistical Process Control (SPC). Control charts on critical dimensions and defect counts, with defined action limits, give operators and supervisors an immediate visual signal when the process drifts. The reaction plan — what to do when a point breaches a control limit — must be documented, trained, and posted at the workstation.
Standard Work documents must be revised to reflect the new procedures. Calibration intervals, material acceptance criteria, and operator verification steps become controlled documents under the QMS. In an AS9100 or IATF 16949 system, these updates are subject to formal change control, ensuring that the process improvements are embedded in the auditable management system rather than held in the memory of the project team.
Dashboards and review cadence close the loop. Real-time defect dashboards give operators immediate feedback; weekly KPI reviews give supervisors trend visibility; monthly management reviews ensure the gains are sustained. The DMAIC project does not end at the Improve presentation — it ends when the control plan is signed off and the process has demonstrated stable capability over a defined validation period.
The DMAIC Phase Sequence
- 01DefineQuantify the defect, map stakeholders, and set the sigma-level target
- 02MeasureCollect baseline data and calculate Cpk to confirm process capability
- 03AnalyseUse Ishikawa and 5 Whys to isolate and empirically validate the root cause
- 04ImprovePilot the corrective action on one cell, then deploy across the line
- 05ControlLock the new standard into SPC, standard work, and the QMS audit cycle
Sustaining the Culture Shift Beyond the Project
The most common failure mode in Six Sigma deployment is not a bad Analyse phase — it is a Control phase that decays within six months of project closeout. Operators revert to old habits, calibration intervals slip, and the SPC charts stop being checked. This happens when the control plan is treated as paperwork rather than as the operating discipline of the line. The quality function must audit the control plan with the same rigour applied to IATF 16949 internal audits.
A successful DMAIC project shifts the organisational mindset. The team that participated in the root-cause analysis, the pilot, and the control-plan development learns to demand data before action. That habit — measured against the requirement of an 8D report, a VDA 6.3 process audit, or a customer complaint investigation — is what transforms the quality culture from reactive firefighting to systematic prevention.
DMAIC is not limited to high-profile crises. It applies to any process where variation drives cost: supplier quality, administrative workflows, machining operations, and assembly cells. The methodology is domain-agnostic because the discipline is universal: define the gap, measure the baseline, validate the cause, pilot the fix, and lock the standard. The tools are well-established; the execution is what determines the result.