Every electronics assembler keeps a reject bin, and nearly every one underestimates what it costs. A joint called out as non-conforming to Class 3 must be documented, quarantined, dispositioned by an engineer, possibly reworked by a certified operator, re-inspected and re-entered into flow. Multiplied across hundreds of borderline calls a month, that administrative and handling chain rivals a full-time headcount. Worse, much of it adds no reliability, because a large share of the rejected joints were fit for service in the first place.
Over-rejection is rarely dramatic. It creeps in one cautious inspector at a time, usually after a customer complaint or an internal scare. Nobody gets blamed for rejecting a marginal joint; the person who passes one that later fails carries the weight. That asymmetry trains entire inspection teams toward conservatism, and once a culture of "when in doubt, reject" takes hold, it is very hard to reverse.
Consider what rework actually does. A lifted pad after a second pass with the iron, a burnt laminate halo around a through-hole, a component stressed by repeated thermal cycling — these are real degradation modes introduced by the response to a cosmetic imperfection. I have seen boards leave rework in worse condition than they entered it, all because an inspector applied a Class 3 reading to a product contracted at Class 2. Reading the criteria correctly is a quality function, not a concession to production.
What Class 2 and Class 3 Actually Mean
IPC-A-610 defines three acceptance classes, and the confusion between the last two is where most of the trouble lives. Class 3 — typical for aerospace, medical and automotive safety electronics — demands continued high reliability in harsh environments, and its criteria reflect that through tighter limits on wetting, fillet formation, hole fill and solder surface condition. Class 2, covering the bulk of commercial and industrial electronics, requires the joint to function over its intended service life but accepts broader cosmetic variation.
Both classes demand a good metallurgical bond; they differ in how much deviation from the ideal they tolerate. The critical point, most often missed on the shop floor, is that the acceptance class is a contractual attribute of the product, not a judgement the inspector makes. If the drawing or customer specification invokes Class 2, applying Class 3 fillet-height expectations is not extra rigour — it is inspecting to the wrong requirement.
The result is the same as rejecting a part for a tolerance tighter than the drawing calls out: a false non-conformance that consumes real money and materials. Where genuine ambiguity exists — an automotive body-control module whose standard references IPC-A-610 without naming a class, for instance — resolve it in writing before building, not at the microscope. A one-line agreement in the quality plan eliminates hundreds of disputed calls later.
Reading the Common Criteria Correctly
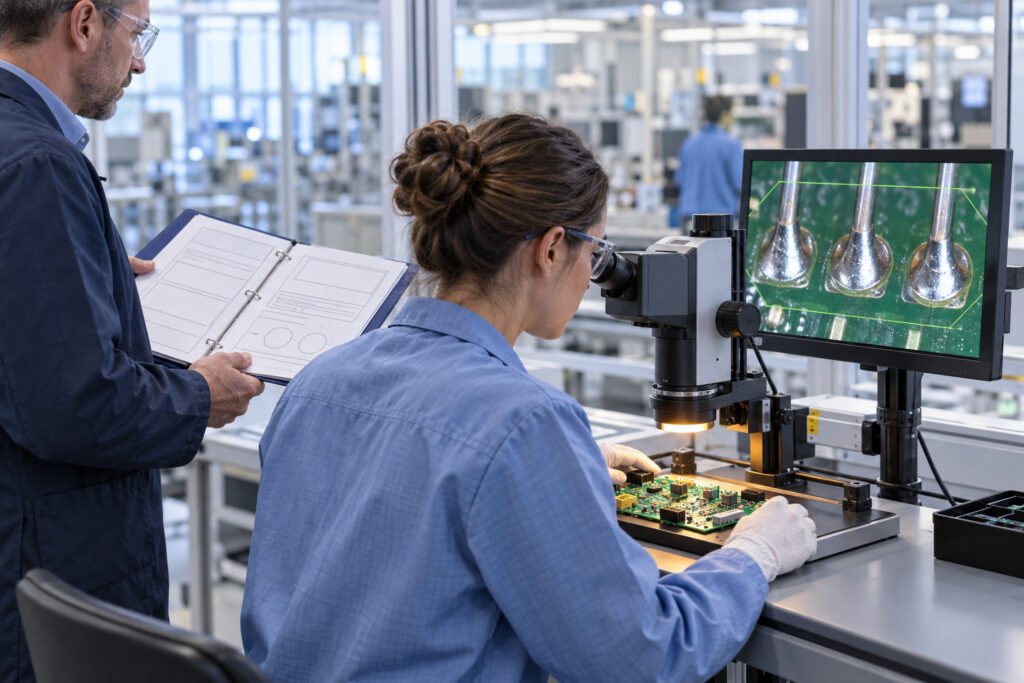
Take wetting first. Class 3 requires wetting over a minimum of 75 per cent of the termination area for most surface-mount criteria, while Class 2 accepts 50 per cent in many cases. An inspector estimating coverage by eye tends to underestimate — the unwetted corner of a gull-wing lead looks worse than it measures. Train people to measure against the stated percentage, with reticle eyepieces or calibrated on-screen measurement on a vision system, rather than eyeballing a vague "mostly wetted" impression.
Hole fill in through-hole joints is another chronic source of over-rejection. Class 3 requires 75 per cent vertical fill of the barrel; Class 2 requires 50 per cent, and both apply the same wetting requirements on the solder side. Inspectors who have only worked aerospace frequently reject 60 per cent fill reflexively, even on Class 2 product where the criterion is comfortably met. Sectioning a sample, or X-raying a board with the fill percentage annotated, calibrates the eye far better than a wall chart ever will.
Note also that the visible fillet on the component side is not the fill measurement. The fill is assessed in the barrel, which may require radiographic methods on assemblies that cannot be cross-sectioned. Lifted or raised leads on J-lead and gull-wing components illustrate the same discipline: both classes share a maximum side overhang tied to lead width and a maximum lifted-lead height. The difference sits in a handful of numbers, not in a blanket "Class 3 tolerates nothing" attitude.
The numbers that separate Class 2 from Class 3
Cosmetic Versus Functional: Where Over-Rejection Lives
Distinguish, in the inspector's mind, between defects that threaten the joint's function and attributes that merely deviate from the ideal. Exposed copper at the edge of a pad, a slightly dull solder surface, non-wetting on a portion of a heat-sink tab outside the electrical path, minor probe disturb marks — many of these are explicitly acceptable or controlled separately under both classes, provided the wetting, fillet and bonding criteria are met. Yet they generate a disproportionate share of rejects because they are visually prominent and easy to spot.
The functional questions are concrete. Does the joint meet minimum fillet formation and wetting coverage? Is the solder connection continuous between termination and land, with no separation or fracture? Is the lead centred within tolerance for its package type? If the answers are yes, a surface blemish does not become a reject because it "looks wrong". Conversely, a hairline crack at the fillet heel, a granular non-wetted interface, or a measling pattern crossing conductors are functional threats regardless of appearance.
I insist on a written distinction exercise during inspector training: photographs of joints that are visually imperfect but fully compliant, placed alongside true defects, with the class and criterion cited for each. The exercise is humbling, including for experienced people. It teaches the habit that every reject must name its criterion — "non-conforming to 8.3.5, wetting less than 75 per cent" — and an inspector who cannot name the criterion cannot defend the reject.
An inspector who cannot name the criterion cannot defend the reject. Criterion-cited rejection cuts false rejects without suppressing a genuine one.
Calibrating the Inspectors Themselves
Inspector calibration is not a one-off certificate; it is a recurring comparison of judgement against evidence. Run periodic attribute studies on a reference board set — known-defect and known-good samples covering the criteria your product actually invokes — and record agreement between inspectors and against the master disposition. Attribute agreement analysis of this kind is standard measurement-systems discipline, no different in principle from an MSA on a gauge.
Where disagreement appears, the cause is almost always one of three: wrong class assumed, criterion misread from the document, or visual estimation drifting without measurement. Each has a different correction, and only the third calls for coaching on technique. The first two are corrected by making the class visible and the criterion explicit — fixes to the system, not the person.
Vision systems and microscopes need the same discipline. Illumination angle changes apparent wetting coverage dramatically; annular ring lights exaggerate reflectivity differences and make marginal wetting look worse. Standardise magnification and lighting per product family, and when an operator challenges a marginal call, have them re-inspect under the standard condition rather than their preferred one. Uncontrolled viewing conditions are a quiet but persistent source of inconsistent calls.
Resolving a disputed joint call with evidence
- 01Capture the callRecord the joint, the criterion cited and the class assumed at the time of rejection
- 02Verify the classConfirm the contractual acceptance class against drawing and quality plan
- 03Measure, do not estimateApply reticle, on-screen measurement, X-ray or cross-section as the criterion requires
- 04Disposition on evidenceEngineering decides against the measured result, not against the risk of the discussion
- 05Feed the reference setAdd the board and outcome to the calibration library so the next call is fast
Building the Discipline Into the Process
Sustained control requires the acceptance class to be visible at the point of inspection. Put it on the router, the work instruction and the inspection station display — anywhere the person making the call can see it without hunting. When the class changes between products running on the same line, this visibility prevents the single most common error: an inspector carrying Class 3 habits from the morning build onto the Class 2 job after lunch.
Rework authority deserves explicit limits. Not every reject should go to rework automatically; the disposition process should first ask whether the finding was valid. A recurring pattern of overturned rejects by product, criterion or inspector is a signal to investigate, not to absorb. Track rejects by criterion number, not just by board.
A spike in one criterion usually means either a genuine process shift — paste printing, reflow profile, component oxidation — or a misreading of that criterion, and a Pareto of reject reasons separates the two quickly. Cross-functional review closes the loop: resolve disputes with cross-sections, X-ray or dye-and-pry where warranted, and feed the answer back into the reference set. What you must avoid is the engineer defaulting to rejection to avoid the discussion; that simply moves over-rejection up one level and teaches inspectors that escalation is pointless.
The Standard Cuts Both Ways
IPC-A-610 is a visual acceptance standard, a shared language between assembler and customer intended to make calls consistent and defensible in both directions. Used properly, it protects the customer from genuinely unreliable joints and the producer from unfounded rejects. Used as a blunt instrument, applied one class above contract out of vague caution, it quietly taxes every board that leaves the line.
Across two decades in automotive and aerospace quality, I have seen the same pattern repeatedly: the plants with the lowest defect costs are not the ones that reject the most, but the ones whose rejects can all name their criterion. Precision at the inspection bench is not the opposite of rigour — it is what rigour actually looks like when money and reliability are both on the line.
Reading the document accurately is not a compromise of quality standards. It is the standard. The assembler who can cite the clause, measure against the stated threshold and defend every disposition is delivering more quality than the one who rejects out of caution — and doing it at a fraction of the cost.