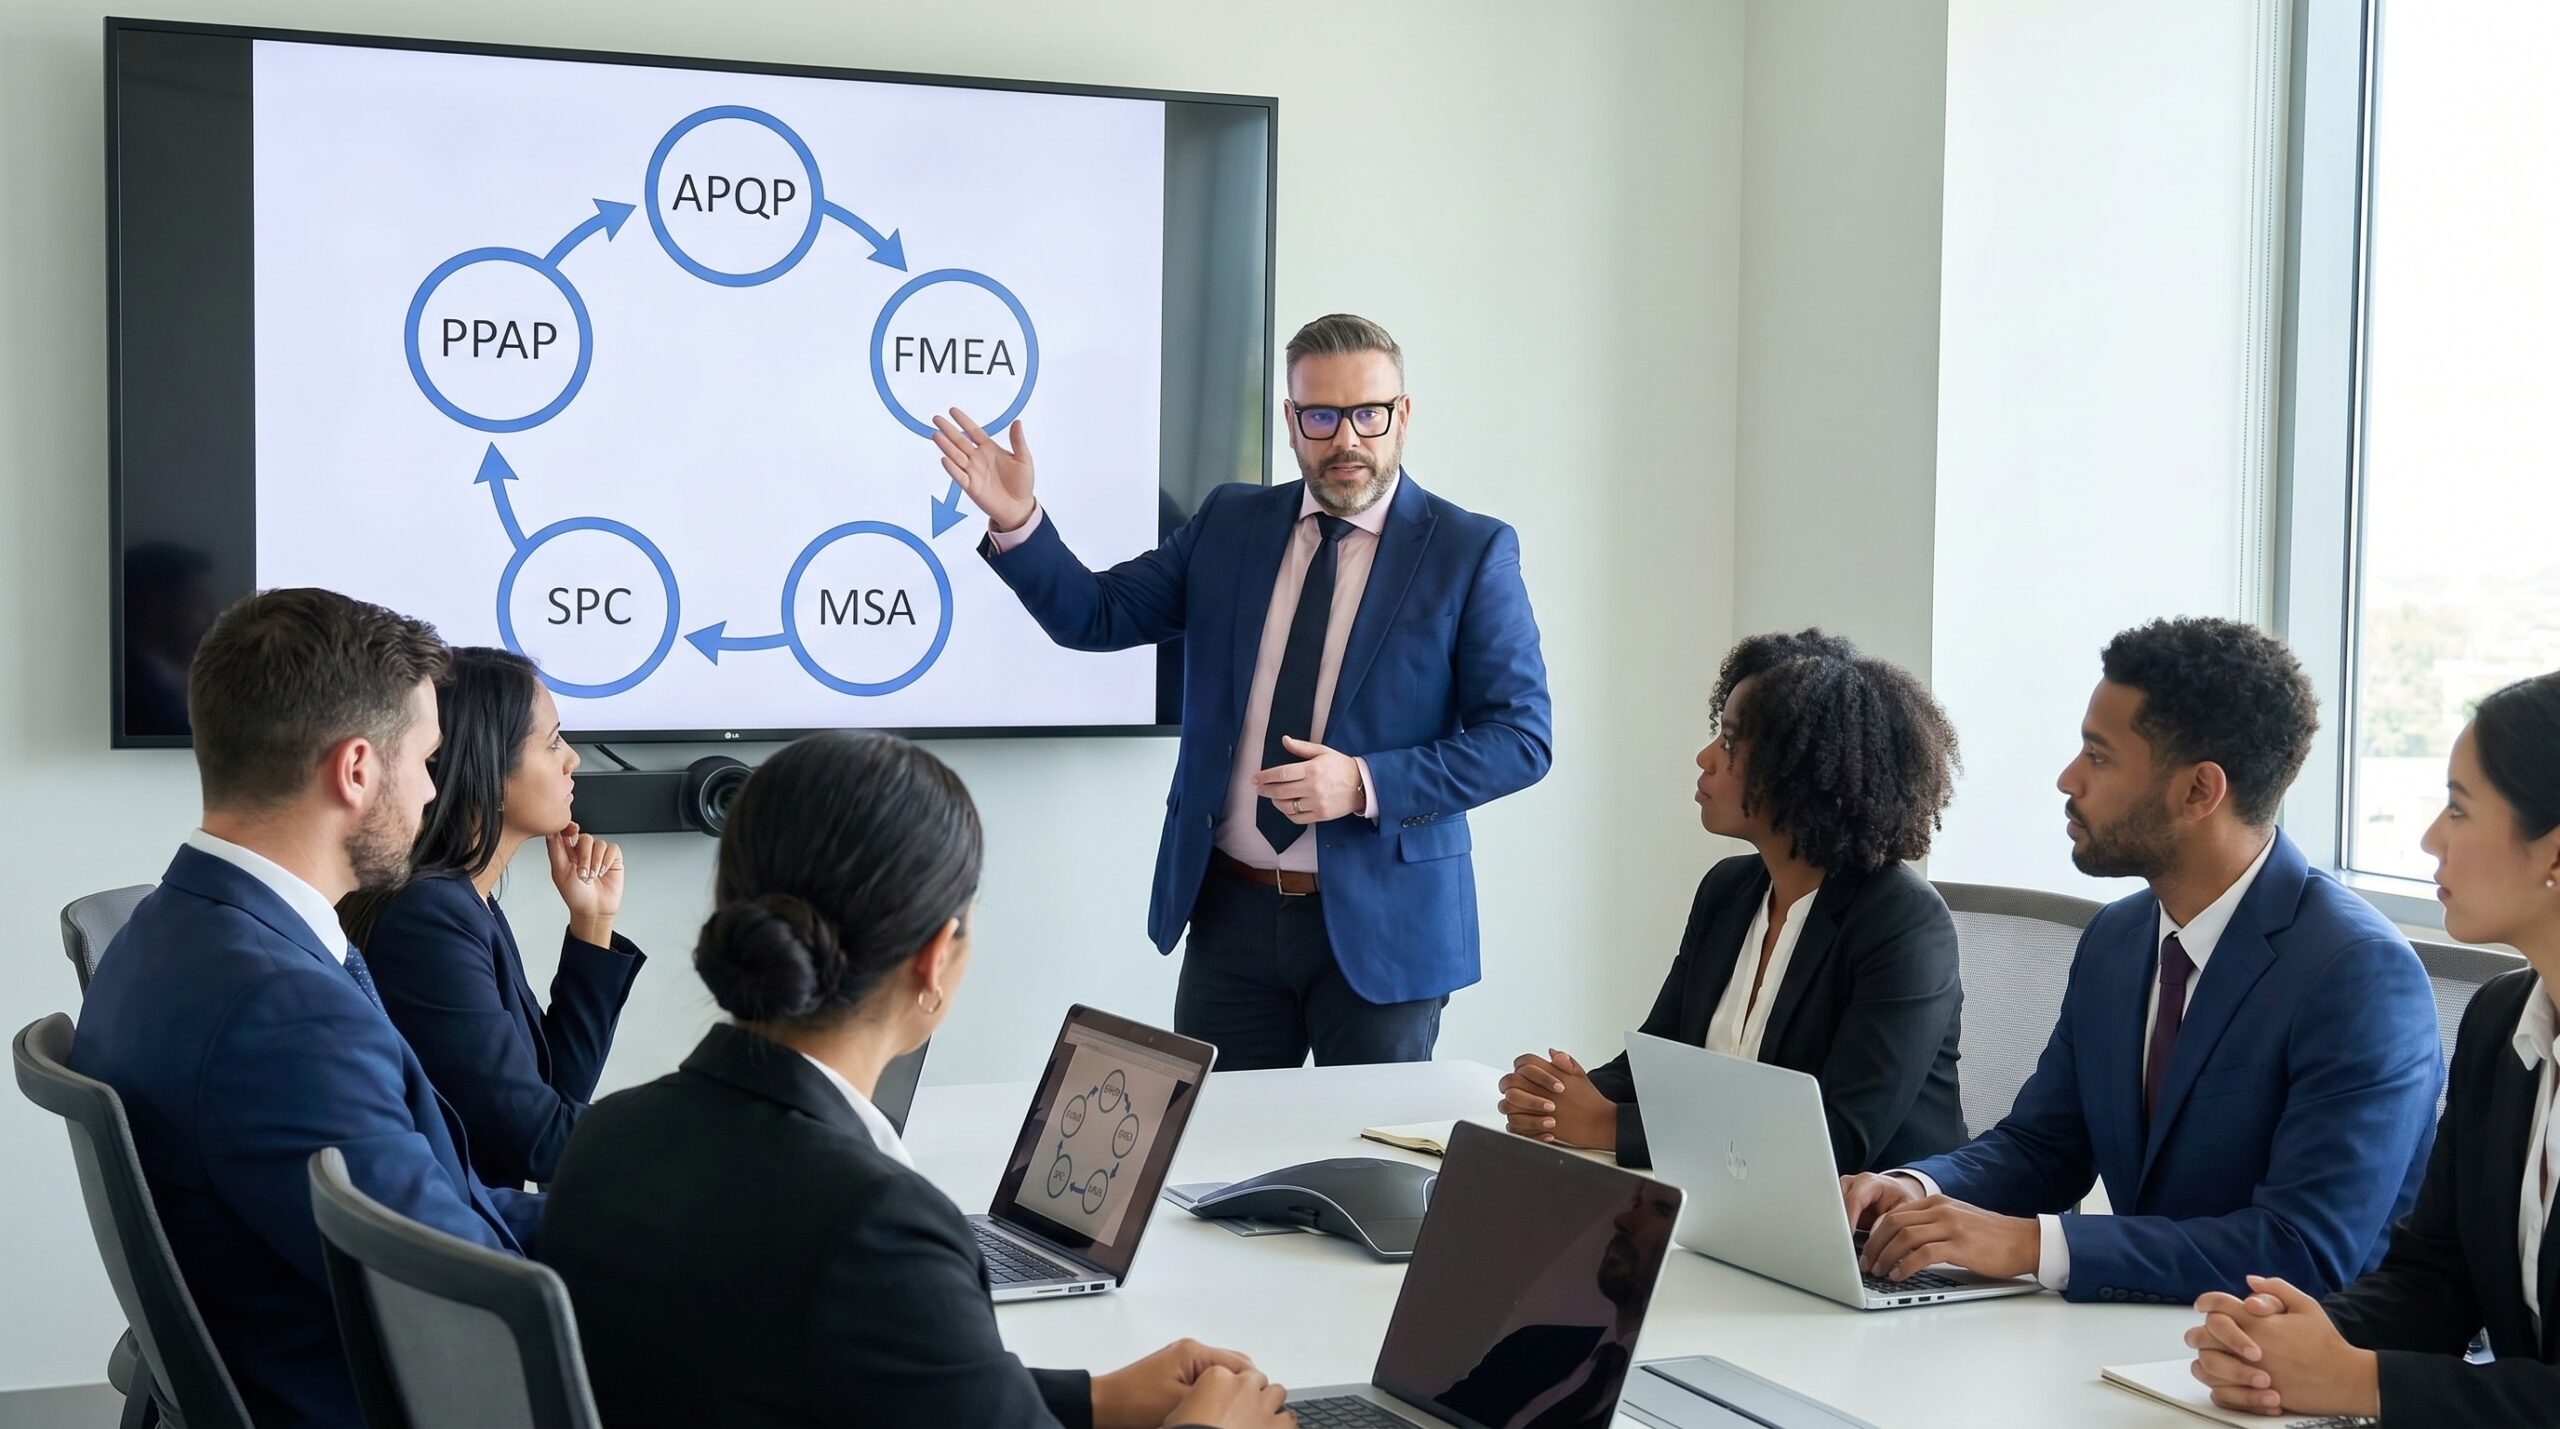
Most organisations treat Core Tools as standalone compliance deliverables. The FMEA is written to meet a deadline, the PPAP is submitted to close a project milestone, and the MSA is dusted off once a year to satisfy an auditor. The result is five isolated documents that fail to reflect manufacturing reality.
When these tools are disconnected, the entire quality system degrades. The FMEA ignores actual SPC scrap data. The MSA validates a gauge sitting in a lab rather than the one used on the shop floor. The Control Plan becomes a copy-paste artefact from a previous product line. You generate paper, but you do not control the process.
IATF 16949 and AS9100 demand an integrated approach because Core Tools are not five separate tools. They are one interconnected system with five working parts. When they fail to communicate, your defect prevention capability collapses.
The Architecture of an Integrated Quality System
Advanced Product Quality Planning (APQP) is the architect of the system. It dictates the timeline and establishes when data must flow between the other four tools. Without this rigid temporal framework, engineering teams execute tasks opportunistically, missing the critical intersections where validation must occur.
The Failure Mode and Effects Analysis (FMEA) acts as the predictor. It defines what might fail and drives the selection of Critical Characteristics (CC) and Significant Characteristics (SC). These identified risks dictate exactly what the Measurement System Analysis (MSA) must verify and what Statistical Process Control (SPC) must monitor.
The Production Part Approval Process (PPAP) serves as the final proof. It packages the verified MSA data, the capable SPC results, the updated FMEA, and the active Control Plan. If any upstream tool contains a flaw, the PPAP submission will expose it to the customer.
Compliance Documentation vs. Integrated System
Disconnected Documents
- FMEA copied from a previous platform without cross-functional input
- MSA performed on a master gauge rather than the actual shop-floor equipment
- Control Plan ignores the failure modes identified during risk assessment
- PPAP submitted with out-of-date data to hit a customer milestone
Integrated System
- Process FMEA drives the selection of CCs and SCs directly
- Gauge R&R strictly verifies the specific instruments monitoring identified risks
- Control Plan dictates SPC application and reaction rules
- PPAP serves as a comprehensive validation package for process capability
Data Flow Across the Five APQP Phases
Information must flow chronologically through the five APQP phases. Phase 1 defines customer requirements. Phase 2 executes the Product Design FMEA, which isolates key product characteristics that must be carried over to the process planning stage.
Phase 3 maps the Process FMEA, flow diagram, and the draft Control Plan. Phase 4 is where the heavy validation occurs: executing the MSA on specified gauges, running the initial SPC process study, and submitting the complete PPAP package. Phase 5 feeds actual production data back into the FMEA and Control Plan.
The critical mechanism here is bidirectional data flow. If SPC reveals an unstable process, that signal must travel back to the Process FMEA for reassessment. If MSA yields a %GRR exceeding 30%, you cannot trust your SPC data, and the Control Plan must be suspended until the measurement system is fixed.
Case Study: Validating a Safety-Critical Component
Consider a new OEM project for a critical brake component with a strict 32-week timeline and zero tolerance for error. In the planning phase, the team defined fourteen Critical and Significant Characteristics, isolating three safety-critical dimensions for rigorous monitoring.
During the Process FMEA, the team identified forty-five failure modes. The highest risk involved inadequate cooling during heat treatment. This specific risk drove the creation of a Control Plan with thirty-eight control points, mandating 100% inspection or active SPC with a Cpk target of 1.67 for critical areas.
During Phase 4 validation, the team executed a Gauge R&R on six measurement systems. A micrometer for a key dimension passed at 8.2% GRR. However, the surface roughness tester failed at 34% GRR. The team refused to ignore the data. They revised the Control Plan, replaced the measurement method, and re-ran the MSA, achieving a passing 9.8% GRR before proceeding.
Submitting a PPAP with an out-of-spec measurement system is not process capability; it is a calculated risk.
Because the measurement system was fixed, the SPC initial process study yielded reliable data. One characteristic initially fell short at Cpk 1.45. The team executed a process adjustment, re-ran the study, and achieved Cpk 1.89. The PPAP Level 3 submission was approved by the customer without waivers, resulting in zero warranty claims over the first year of production.
Common Failures in Core Tools Application
The most frequent failure is the copy-paste approach. Engineers take a previous FMEA, change the project name, and submit it. This completely ignores the unique variables of the new process, rendering the risk assessment useless. Every project demands a ground-up analysis of its specific failure modes.
Another systemic breakdown is unidirectional communication. Production records SPC data showing a trend, but nobody updates the FMEA to reflect this newly discovered failure mode. MSA fails, but the Control Plan continues to mandate the use of the flawed gauge. Data must flow backwards just as freely as it flows forward.
Organisations also fail when they treat Core Tools as project milestones rather than living documents. PPAP submission is not the finish line. Volume production generates new data that must drive continuous updates to SPC control limits, the FMEA, and the Control Plan. When departments operate in silos—Quality owns the FMEA, Engineering owns APQP—these critical updates never happen.
Gatekeeper Metrics for Tool Integration
Establishing Cross-Functional Ownership
Fixing a broken Core Tools system requires mapping the information flow across a cross-functional team. Quality, Engineering, and Production must jointly trace how a failure mode identified in the FMEA translates into a measurement requirement in the Control Plan, an MSA study, and a specific SPC control chart.
Begin with a four-week audit of your existing documentation. Gather all current FMEAs, Control Plans, and PPAP packages. Look for the gaps. If a Control Plan specifies a characteristic that the FMEA completely missed, or if the SPC charts monitor parameters unrelated to actual failure modes, you have found your systemic breakdown.
Implement this integrated approach on a single pilot project before rolling it out across the plant. Force the team to prove that information is actively moving between the tools. When the MSA data changes, verify that the Control Plan is updated accordingly.
Sustaining the System in Serial Production
An integrated system requires maintenance. Establish a strict quarterly review cycle. Examine the SPC data for emerging trends. If scrap rates rise on a specific machine, pull the Process FMEA, evaluate whether the failure mode was anticipated, and update the risk scoring accordingly.
Layered Process Audits (LPA) must verify that operators are actually following the Control Plan. If the Control Plan dictates a specific gauge and sampling frequency, the audit must confirm it. A documented process that is ignored on the shop floor provides zero quality assurance.
When integrated correctly, APQP drives the timeline, FMEA predicts the risks, MSA guarantees measurement integrity, SPC monitors stability, and PPAP proves the capability. Treat them as isolated tasks, and you are simply generating paper. In aerospace and automotive manufacturing, a paper trail without process control is a liability.