I was auditing a automotive plant recently when the production director proudly showed me a newly commissioned ERP system. The software cost a significant six-figure sum, yet the assembly line had been stationary for three hours waiting for a standard fastener. When I asked why the line was down, the answer was familiar: the system had not triggered the delivery.
This scenario highlights a fundamental disconnect in modern manufacturing. Companies invest heavily in digital planning tools while ignoring the physical reality of the shop floor. Material flow remains chaotic, WIP accumulates, and operators are left scrambling. Quality inevitably suffers under these conditions, regardless of the sophistication of the MRP system generating the production orders.
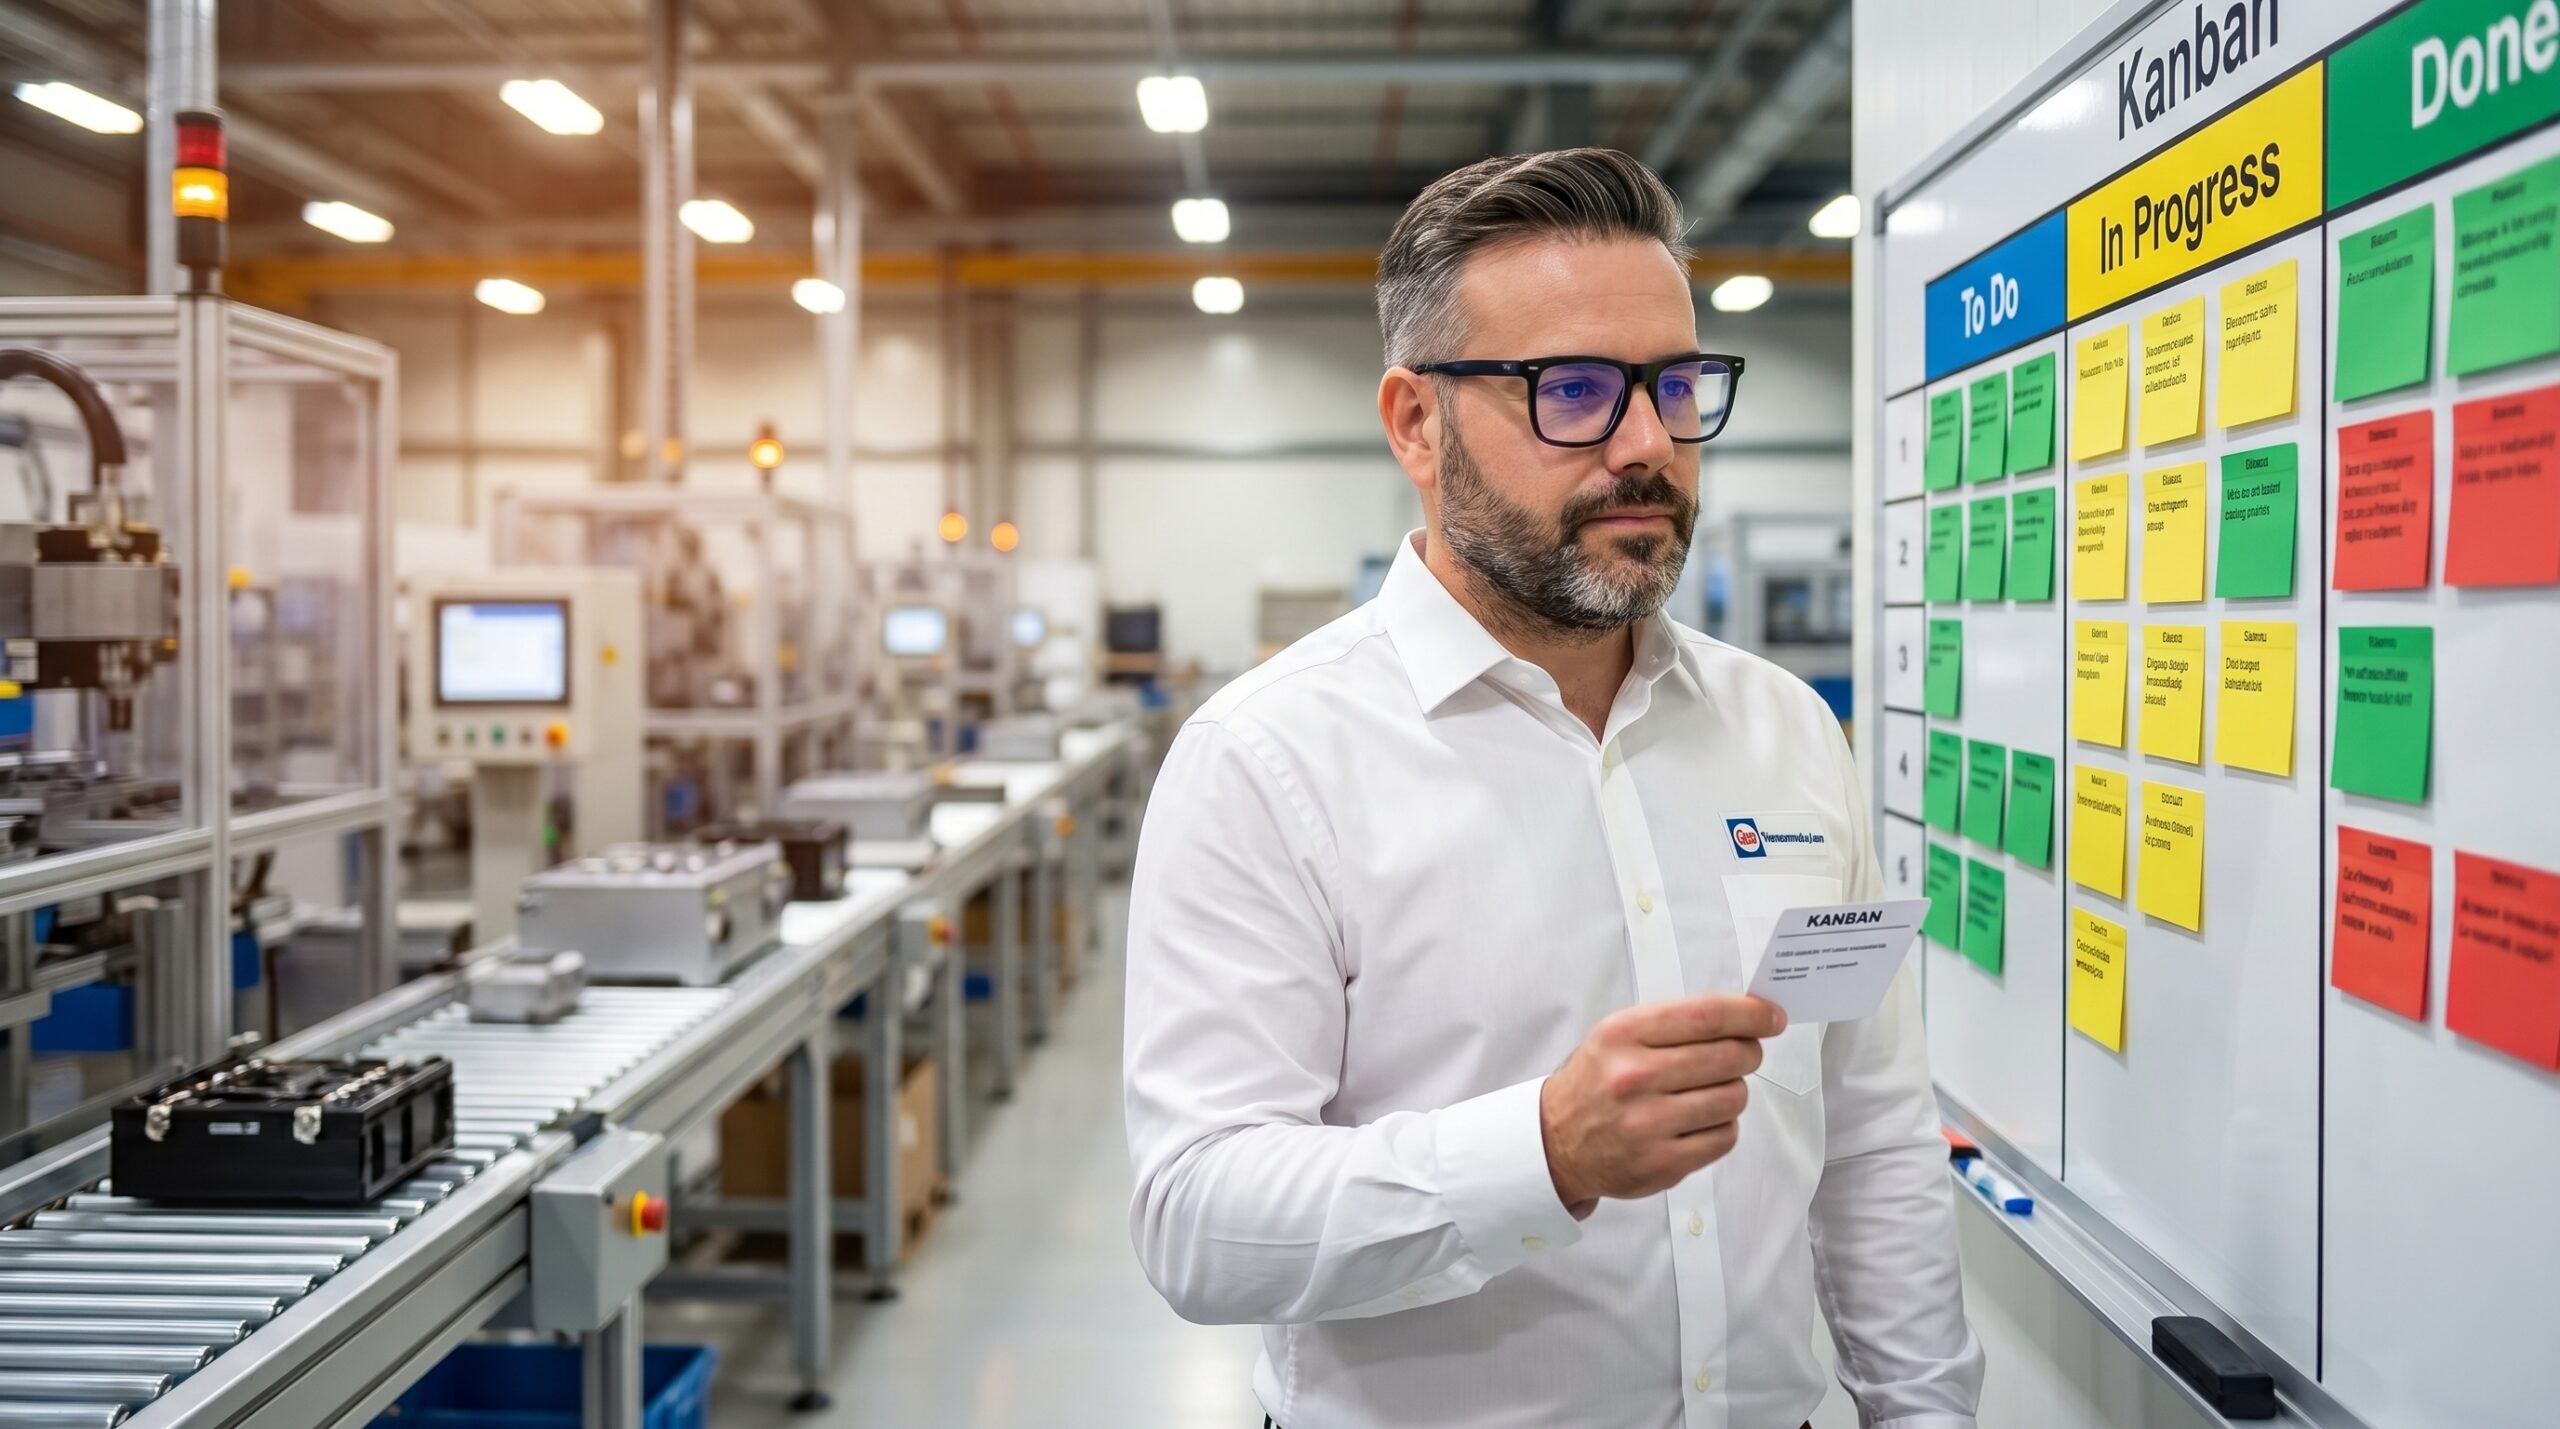
Kanban solves this disconnect. Originating from Taiichi Ohno's observations of American supermarkets in the 1950s, the system translates simple visual signals into a precise replenishment mechanism. It is not a management buzzword. It is a visual nervous system that ensures the right part reaches the right place at the exact moment of demand, stabilising the process for the operator.
Material Flow Chaos Directly Generates Defects
Quality professionals frequently treat material handling as a logistical concern rather than a quality variable. This is a critical oversight. When material arrives late or in the wrong sequence, operators rush. Rushing leads to skipped steps, improper torque application, and assembly errors. The operator is no longer following Standard Work; they are firefighting.
Kanban breaks this cycle at the source. By guaranteeing material availability through controlled buffers, the operator is freed to focus entirely on executing the process correctly. In my experience auditing and implementing systems at WITTE Automotive and SNOP, the most immediate quality improvement often comes not from better inspection, but from removing the logistical stress that causes human error in the first place.
The reduction of Work in Progress (WIP) is where Kanban most directly impacts defect containment. High WIP levels act as a buffer that hides defects. If you hold 2,000 units between Operation 3 and Operation 4, and a dimensional drift occurs at Operation 3, the defect is not discovered until the entire batch moves downstream. You now have a massive scrap event or a costly rework quarantine.
Push vs Pull: The Mechanics of Quality Containment
Most manufacturing facilities operate on a push system. The MRP generates orders based on forecasts, and production builds regardless of downstream readiness. The result is overproduction, congested aisles, and parts sitting in intermediate storage where they can degrade, sustain damage, or become mixed with non-conforming product.
A pull system, driven by Kanban, reverses this logic. Each downstream operation withdraws material from the preceding operation only when actual consumption creates demand. The signal — whether a physical card, an empty container, or an electronic trigger — governs the movement of goods. Nothing is produced until a legitimate, downstream requirement exists.
| Parameter | Push System (MRP-driven) | Pull System (Kanban) |
|---|---|---|
| WIP Inventory | High | Low and controlled |
| Defect Detection Time | Long; defects hidden in queue | Short; defects surface immediately |
| Containment Scope | Large batches at risk | Limited to single Kanban quantity |
| Floor Space Required | Extensive storage needed | Minimised |
Calculating and Implementing the Kanban Signal
Implementing Kanban requires discipline, not advanced software. The calculation for Kanban quantity is straightforward: multiply average daily consumption by the replenishment lead time, apply a safety factor for variability, and divide by the container capacity. This yields the exact number of containers or signals required to sustain the loop.
For a part with a daily usage of 500 units, a half-day replenishment time, a 20% safety margin (1.2 factor), and a container size of 100 units, the calculation demands exactly three Kanban containers. One container sits at the line, one is in transit, and one is at the supplier or warehouse. This visual, physical constraint prevents both stockouts and overstocking.
I strongly recommend starting with physical cards and containers rather than jumping to e-Kanban. Digital systems can mask underlying process instabilities with automated workarounds. A lost physical card immediately exposes a broken link in the material flow, forcing the team to address the root cause rather than relying on an IT workaround. Once the physical system stabilises, digital integration is straightforward.
Physical Kanban Replenishment Loop
- 01Consumption at lineOperator empties the container during standard production.
- 02Signal generationEmpty container and Kanban card are moved to the designated return area.
- 03Material withdrawalMaterial handler collects the signal and retrieves a full container from the supermarket.
- 04Replenishment triggerEmpty container triggers the warehouse or supplier to replenish the consumed stock.
Integrating Kanban with IATF 16949 Core Tools
Kanban cannot exist in isolation from your quality management system. During the Process Design phase of APQP (Advanced Product Quality Planning), the material replenishment strategy must be explicitly defined. The Process Flow Diagram should identify where Kanban loops will operate, and these constraints must be respected during PFMEA (Process Failure Mode and Effects Analysis).
When constructing the PFMEA, treat Kanban failure as a legitimate failure mode. What happens if the card goes missing? What is the risk if the supplier delays? How does the system respond if a container is damaged? Establishing detection controls and recovery plans for these logistical failures is just as critical as addressing dimensional tolerances or torque specifications.
A Kanban system without rules is just a suggestion box; the rules must be absolute.
The Control Plan must also reflect the Kanban parameters. The verification of Kanban levels should be integrated into standard layered process audits (LPA). If Kanban limits are routinely exceeded, it indicates a process instability that requires immediate escalation, similar to an SPC chart hitting its control limits.
Standard Kanban System Metrics
Management Discipline and Common Implementation Failures
The most frequent point of failure in Kanban implementation is the unauthorised addition of containers. A supervisor facing a minor stockout will inevitably request "just one extra container" to smooth the flow. This action instantly destroys the system's ability to signal true demand. The rule must be absolute: no material moves without a legitimate Kanban signal, and limits are never breached without formal root cause analysis.
Another common error is attempting to apply Kanban to processes with extreme demand variability without first stabilising the process. Kanban relies on predictable consumption rates. If upstream operations or customer demand fluctuates wildly, a simple pull system will fail. In these cases, buffer management and demand smoothing must precede Kanban deployment.
Finally, Kanban systems degrade without active management recalibration. Demand shifts, suppliers change lead times, and product mixes evolve. A Kanban calculation performed twelve months ago is almost certainly inaccurate today. The system must be reviewed monthly against actual usage data, and container quantities must be adjusted to reflect the new reality of the process.
Achieving System Stability Through Visual Control
When I build greenfield QA/QC departments, I insist on visualising the entire material flow. Kanban transforms the abstract numbers in an ERP system into physical, undeniable facts on the shop floor. When an empty container appears, it demands immediate action. It replaces the excuse that "the system did not tell us" with a clear, visual imperative that everyone from the operator to the plant manager can understand.
This visibility directly enforces Standard Work and stabilises the environment. By strictly limiting WIP, you reduce the surface area for defects, shorten lead times, and isolate quality issues before they compound. The discipline required to maintain the system forces an organisation to confront its underlying instabilities rather than hiding them behind excess inventory.
Kanban is not a logistical tool; it is a fundamental quality mechanism. It ensures that the operator has the time, the parts, and the stability required to execute the process exactly as defined in the Control Plan. By respecting the limits of the pull system, you build a culture that prioritises process integrity over blind output, which is the foundation of zero-defect manufacturing.