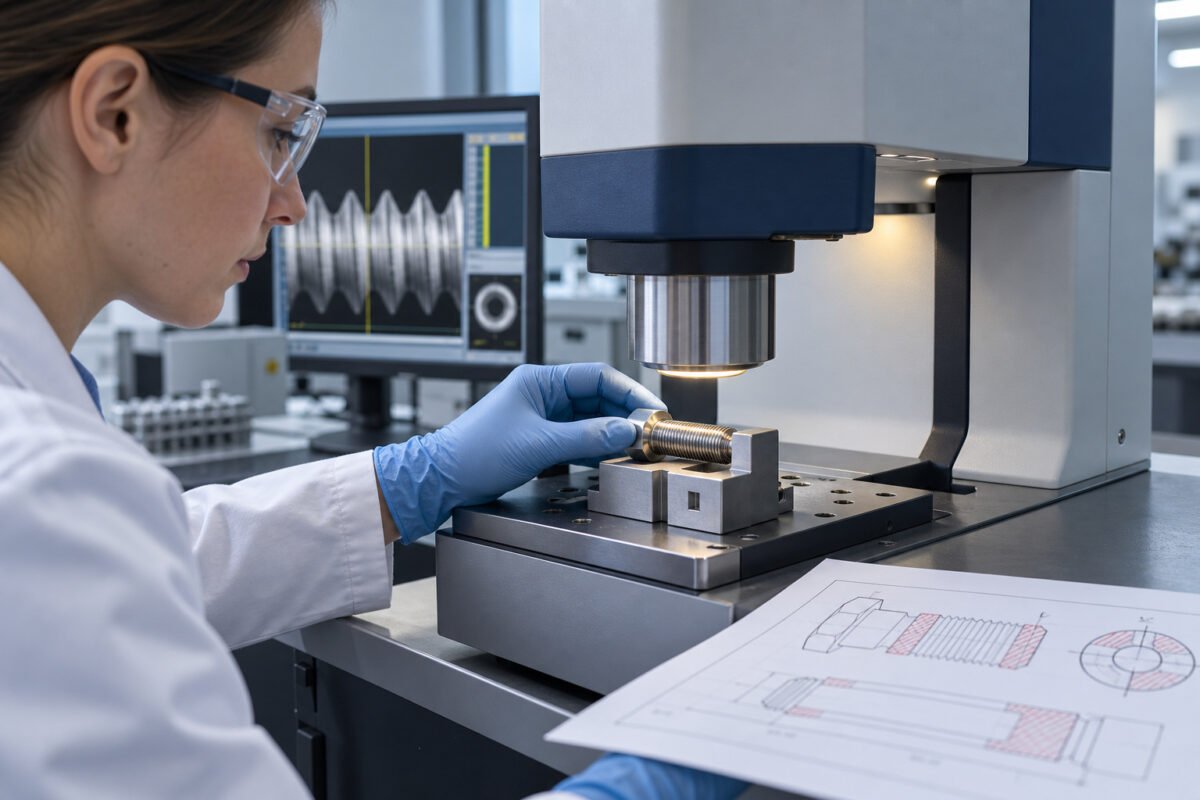
Every plating and coating specification I have worked to carries the same hidden clause, written or not: thickness applies to the significant surface. Not the whole part, not an average of the part, not wherever the probe happens to sit comfortably. The significant surface is the functional region — the contact zone, the sealing face, the threaded engagement, the area exposed to corrosion in service. Everything outside it tolerates thin deposits, burning, or rack marks, provided the function survives.
Across two decades in automotive and aerospace quality, I have seen that most thickness disputes between supplier and customer are not disputes about the process. They are disputes about which region of the part the specification governs. A supplier measures on a large flat area near the edge of a stamping; the customer measures on a radius where the deposit runs thin, because that radius is the wetted surface in the assembly. Both parties hold valid readings from the same part and reach opposite conclusions on conformity.
The fix happens before parts are plated. Get the significant surface defined on the drawing — shaded, hatched, or called out in a note — and agree the measurement points with the customer in writing. A five-minute conversation at design stage saves weeks of concession requests later, and it prevents the worst outcome: a part that passes at the point of measurement and fails in the field at the point of use.
What Specifications Say — and What They Leave Out
Read a typical callout such as "Zn-Ni 8 µm min, per the relevant material standard" and you will find it says less than it appears to. Does the minimum apply to every point on the significant surface, or to the average across it? Is a spot reading permitted to dip below the minimum on edges, corners and recesses, which everyone in plating knows deposit differently? Material standards for metallic coatings commonly acknowledge that sharp edges, holes and deep recesses cannot hold the same thickness as flat areas, and they carve out exemptions. The customer's incoming inspector may not have read that far.
Averaging is the classic ambiguity. Some specifications permit an average of several readings per surface; others demand a point-by-point minimum. XRF instruments happily report a single integrated measurement over an aperture of a few millimetres, which is effectively an average whether you intended one or not. Cross-section metallography gives you point values at precisely located positions — but only at those positions. If the supplier certifies an average and the customer rejects on a point minimum, the argument is about the contract, not the coating.
Thickness distribution over complex geometry makes this worse. Current density concentrates at edges and peaks; recesses and the far side of through-holes see low current and thin deposits. A barrel-plated fastener shows thickness variation from crest to flank to root of the thread, and the specification may be silent on which of those three locations governs. When a drawing gives you a thickness without location, treat the drawing as incomplete and raise the query formally. Silence is not an agreement; it is a deferred argument.
XRF: Fast, Non-Destructive, and Location-Sensitive
X-ray fluorescence is the workhorse of coating thickness measurement in electroplating shops, and rightly so. It is non-destructive, takes seconds, needs no consumables, and can resolve multi-layer systems such as zinc-nickel over steel with a chromate top layer, layer by layer. Modern instruments give composition alongside thickness, which matters enormously for zinc-nickel where nickel content is part of the specification, not incidental information.
But XRF has physical limits that feed the location argument directly. The measurement integrates over the beam aperture — commonly a collimator of a few millimetres, or a spot well under a millimetre on small features. The reading is thickness weighted over that footprint. On a thread flank, a radius, or a small terminal pin, you are measuring a shape the calibration did not anticipate: convex surfaces can read thin, concave surfaces can read thick, and edge effects distort both.
Substrate and interlayer complications follow. XRF assumes the layer structure it was calibrated for; unexpected phosphorus content in an electroless nickel underlayer, or a zinc diffusion layer from processing, shifts the answer. Rough surfaces scatter the signal and bias low. Reposition the part by a millimetre on a part with real thickness gradients — which is every real plated part — and you get a different number, not because the coating changed but because you measured a different place.
The discipline with XRF is therefore fixture discipline. Build a holder that locates the part repeatably under the collimator at the agreed measurement points. Record the collimator size and the point identifiers on the certificate. When a customer re-measures, they must be able to put their instrument on the same locations; if they cannot, the disagreement is location, not coating, and arguing about chemistry is wasted breath.
Cross-Section Metallography: The Referee Method
Metallographic cross-sectioning remains the referee. You mount the part, section through a defined plane, polish, etch if needed, and measure the deposit directly under a calibrated microscope or SEM. What you see is actual local thickness at that exact position, layer by layer, including porosity, inclusions and interface condition. Where XRF reports an integrated average over a spot, the cross-section tells you the truth along one line — and destroys the part to do it.
The catch is representativeness. A cross-section shows one plane through one location on one part. Section the same fastener through the crest of the thread and through the root and you get two different thicknesses, both correct. Sectioning angle matters as well: if the cut is not perpendicular to the surface, the measured width overstates true thickness by the secant of the tilt error. A few degrees is negligible; ten or fifteen is not, and I have seen disputes dissolve the moment someone checked the sectioning jig.
Preparation artefacts are the other trap. Smearing of a soft deposit — cadmium, tin, zinc — during grinding can blur the interface in either direction. Rounding of edges during polishing thins the apparent coating at corners, precisely where people want to check edge coverage. A poorly prepared mount produces confident, precise, wrong numbers, which is worse than no numbers at all.
Used properly, cross-sectioning validates the XRF programme: section parts at the points measured by XRF, compare, and correct for geometry bias. It is also how you characterise the thickness distribution across the significant surface once, at qualification, so routine control can monitor the best-correlated single point. Cross-section the referee; XRF the routine; never confuse the two roles.
Correlating XRF routine control to cross-section truth
- 01Define significant surfaceAgree the functional region and measurement points with the customer, in writing, before plating.
- 02Cross-section surveySection several parts across the significant surface to map the true thickness distribution.
- 03Select control pointsChoose the worst-confirmed location plus one or two stability points, and a flat that tracks them.
- 04Correlate XRFMeasure the same parts by XRF, quantify geometry bias, and document the margin.
- 05Lock the routineFix the fixture, collimator and point IDs in the control documentation.
Sampling the Significant Surface Properly
Once the significant surface is defined, you need a defensible set of measurement points. The principle I apply: locate points where the process predicts thickness will be lowest on the significant surface, plus one or two typical points for stability monitoring. Low-current-density recesses, the root of deep threads, the far side of blind holes within the significant region — these decide conformity, not the proud flat area the operator favours because the probe sits nicely there.
For fasteners, standard practice in most plating houses is to measure on the shank or body flat for routine control and to verify thread flanks periodically by cross-section, because flank thickness governs fit and crevice corrosion behaviour but is nearly impossible to hit reliably with an XRF spot. For stamped contacts and terminals, the functional contact zone usually sits at a formed radius — awkward geometry, but it must be measured there or correlated to a flat that tracks it. Correlation is legitimate, but it must be demonstrated with data, not assumed.
Part-to-part variation adds a second layer. Rack position in the bath, gas shadowing, and part orientation in barrel plating all shift the distribution. A scheme that samples only the first part off a rack bar tells you about that bar. Sample across the rack — top, middle, bottom, inner and outer positions — at least during initial capability work, then lock the routine sample to the worst-confirmed position.
An undocumented measurement location is tribal memory, and tribal memory fails precisely during the audit or the dispute when you need it most.
Document the points. Photographs with circled locations, fixture IDs, collimator sizes — attach them to the control documentation so the scheme survives personnel changes. When an auditor asks why you measure where you measure, the answer should be a document, not an opinion.
Fighting the Conformity Argument — and Preventing the Next One
When the rejection letter arrives with a low thickness reading, resist the urge to argue chemistry first. Establish three facts before anything else: where exactly the reading was taken, with what method and aperture, and what point of the specification that location belongs to. A surprising share of rejections collapse at step one — the customer's inspector measured on a non-significant surface, or used a spot size that averaged across a gradient the specification treats point-by-point.
Where the disagreement is genuine — their point reads low, yours reads compliant — propose the cross-section as referee, sectioned at the disputed location, prepared properly, measured perpendicular. Get the method agreed before the parts are cut, because a destroyed sample cannot be re-measured. Insist on sectioning a location both parties accept as within the significant surface; a referee test at an ambiguous location settles nothing.
Prevention is cheaper and mostly clerical. Put measurement locations on the drawing or in an agreed annex. State point-minimum versus average explicitly. Define edge and recess exemptions where the standard allows them, so the inspector on both sides applies the same rule. Review this at every new part introduction and every drawing revision, because engineers revise geometry more often than they revise coating notes, and a moved radius can silently move your worst-case measurement point.
What teams argue about versus what settles it
What losing teams do
- Argue bath chemistry and process capability first
- Measure wherever the probe sits conveniently
- Certify a single number with no point identifiers
- Treat a silent drawing as agreement
- Keep the location scheme in one operator's head
What settles it
- Establish location, method and aperture before anything else
- Measure defined points on the significant surface, on a fixture
- List point IDs, collimator size and individual readings on certificates
- Raise a formal query on any drawing silent about location
- Document the scheme with photos, fixture IDs and correlation data
Building Location Into the Control Routine
Routine control should be designed backwards from the specification's location requirement. If the spec is a point minimum on defined significant surfaces, your XRF routine measures those defined points, on a fixture, with the collimator matched to the feature size, and the certificate lists the points. If the spec permits averaging, say so on the certificate and show the individual readings, so nobody has to reconstruct your arithmetic from a single number.
Correlation work belongs in the file: the cross-section study that showed flank thickness runs below shank thickness by a known margin, the rack-position study that identified the weak corner of the plating line. These are not one-time paperwork; they are the technical basis for why your chosen measurement point protects the customer's functional requirement. That file is what separates a control scheme from a habit.
Finally, watch the drift. Coating thickness distributions move as baths age, anodes deplete and fixtures wear. A location that was worst-case at launch may no longer be. Re-run the distribution check periodically — cross-section a handful of parts across the significant surface and confirm your control point still tracks the minimum. Measurement location is not a decision you make once; it is an assumption you re-test, and the parts you ship in the meantime are only as good as the last time you checked it.