Equipment that left the factory within tolerance and passed every outgoing inspection still arrives at sites unprepared to receive it. The defects found at handover are rarely manufacturing defects. They are created by untrained hands, uncontrolled environments and paperwork nobody reads until something fails.
If your quality system ends at the loading bay, you do not have a quality system. You have a warranty budget with a delay attached. Installation is a manufacturing process and deserves the same discipline applied to machining or assembly: torque values, alignment tolerances, environmental limits, calibration of site instrumentation.
Across two decades in automotive and aerospace, I have audited installation processes on four continents, and the pattern is consistent. This article sets out what to check at a customer site, what fails most often, and what a defensible handover record actually contains.
The Site Itself Is a Process Input
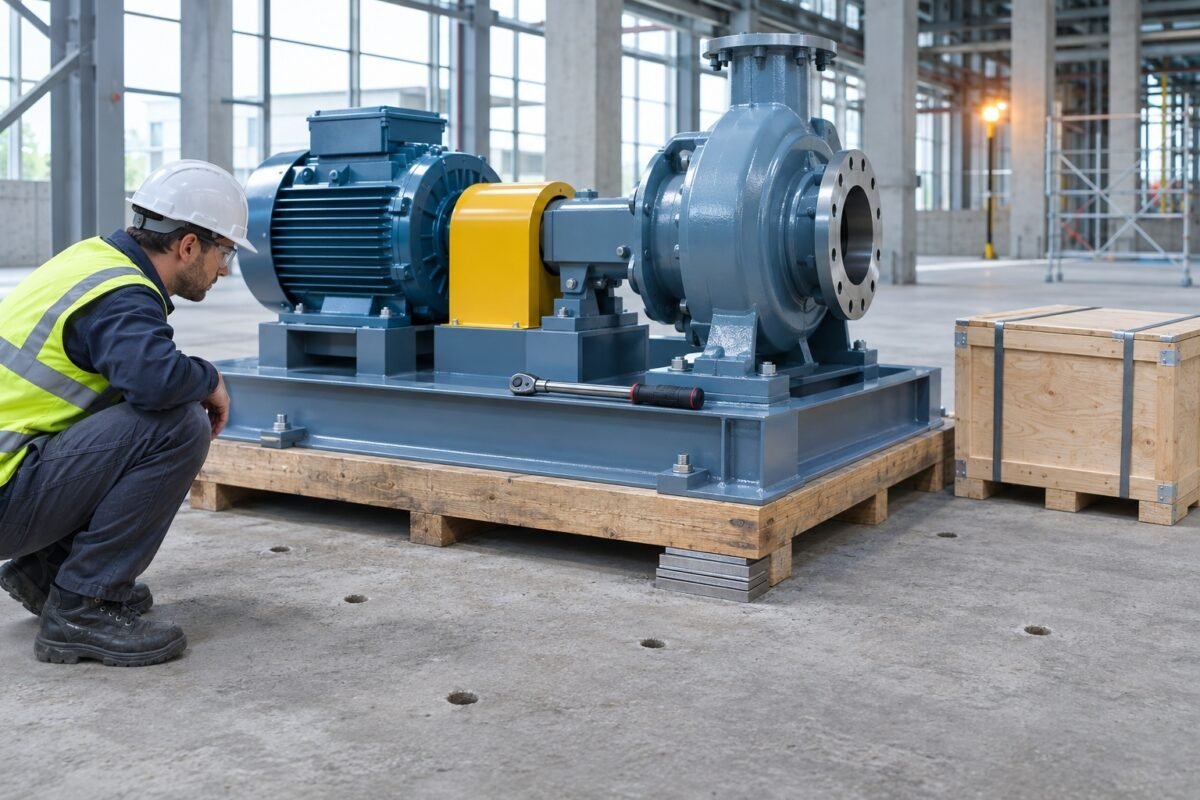
Treat the installation environment as incoming material, because it behaves like one. Foundations are the classic failure: a machine base poured to a drawing the civil contractor never saw, flatness out by millimetres, anchor bolt positions transferred by tape measure rather than template. Before anything is uncrated, demand a foundation survey — levels on a grid, surface profile recorded, concrete curing certificates checked against specification.
A press frame bolted to an uneven base will twist the moment you torque it down. You have just built distortion into a structure that was flat when it shipped. That defect did not exist at outgoing inspection, and no amount of factory process control would have caught it.
Power quality and utilities belong on the same checklist. I have seen drives destroyed in the first week because the site supply had unmeasured harmonics, earthing was daisy-chained through conduit, or phase imbalance exceeded what the transformer tapping could absorb. Compressed air is equally guilty: moisture, particulate, oil carryover. Pneumatics flushed and capped at the factory, then connected to a rusty site airline, put the first contamination straight into your valve block.
Measure before you connect anything you care about: dew point, pressure at the point of use under flow, a particle sample. Temperature and humidity swings matter more than most commissioning plans admit — laser-aligned spindle assemblies drift as the hall heats, and adhesives have cure windows a draughty building will violate. Record ambient conditions daily during commissioning. When I review a dispute about a machine that "was never right from day one", the site logs are usually silent, and silence is evidence against you.
Installer Competence: The Weakest Link
Field installation is frequently subcontracted, sometimes twice removed from the OEM, and the person turning the wrench may hold a generic mechanical qualification with nothing specific to your product. Ask to see the training matrix for the actual crew on site, not the company's. When did they last install this model? Who assessed them? Is there a witnessed practical sign-off, or only a classroom attendance record? If the answer is a laminated wallet card, the competence system is decorative.
The specific failures are depressingly consistent. Hydraulic fittings overtightened because the installer applied steel-pipe torque habits to stainless, stripping the flare. Gearboxes filled with whatever oil was in the site store because the commissioning spares kit never arrived. Lifting points ignored in favour of "we always sling it like this", bending a frame that then passes every geometric check except the one that matters under load. Each is a training and instruction failure, not a craftsmanship mystery.
Site work instructions must differ from factory instructions. They cannot assume tooling, fixtures or a controlled environment, and they must state what to do when conditions are out of range: stop, or proceed with a defined alternative. Insist on hold points requiring a signature from a named, competent person before the next stage — base grouted and cured, services terminated and tested, first power-up, dry cycle, load test. Without hold points, nobody can later say what was actually done, only what was supposed to be done.
Special processes follow you to site. If welding is required — guard brackets, pipe supports, earthing straps — the welder needs a valid qualification for the process and position. Adhesive bonding and torque-controlled anchoring are the same category. Keep the site weld procedure and installer certificates in the commissioning file, because when a bracket cracks two years later, the first question from every party's lawyer is whether the welder was qualified. If your records cannot answer that, you own the failure regardless of who held the torch.
Variation the Factory Never Saw
Every site introduces variability your factory capability study never accounted for. At the works, joints are torqued with calibrated DC tools and logged per joint. On site, the same joint sees a click wrench last calibrated years ago, operated at an angle that breaks the torque-versus-tension relationship, in freezing conditions that change friction coefficients. The result is a bolted structure with scatter the designer never imagined.
My rule: any structural or safety-critical fastener on site gets a calibrated tool, a marked joint and a signature in the torque log. Anything less replaces engineering with folklore.
Interfaces are the second source. When your equipment connects to existing plant — legacy conveyors, a customer's SCADA, third-party safety circuits — you inherit their degradation and their undocumented modifications. Cable schedules from a decade ago do not match what is in the trunking; signal levels sit at the edge of specification. Run an interface verification test before integration: every signal, every interlock, proved end to end with actual measurements, not a nod from the site electrician who "knows this plant". The defects created here are insidious because the machine appears to run and fails only under conditions nobody tested.
Site modification deserves its own warning. A bracket that does not fit gets drilled, a duct gets trimmed, a sensor gets relocated "temporarily" — each change made without the assessment the design change process would have demanded in the factory. When I audit a failed installation, I list every field modification and check each against a documented concession. The ones without paperwork are, almost without exception, the ones that caused the problem.
A field change without an engineering disposition is an uncontrolled design change wearing overalls.
Commissioning: Prove It, Don't Demonstrate It
There is a difference between showing a machine running and commissioning it. A demonstration is theatre for the customer's management; commissioning is a defined test programme with acceptance criteria, executed against a signed procedure, with results recorded by serial number and test stage. Sequence it deliberately: dry cycle, loaded cycle, endurance at rated duty, then interruption tests — power loss mid-cycle, emergency stop under load, safety interlock violation.
Measure what the specification actually states: cycle time, positioning repeatability, temperature rise at bearings, vibration signatures against baseline readings, leak rates on hydraulics held at pressure for a defined soak. Anything the specification does not state is not tested, and therefore not defended — write acceptance criteria before the test, not after the result.
A defensible commissioning sequence
- 01Dry cycleMechanical function without load; interlocks proven
- 02Loaded cycleRated duty, measured cycle time and repeatability
- 03EnduranceSustained rated duty; thermal and vibration trending
- 04Interruption testsPower loss, e-stop under load, interlock violation
- 05Baseline captureVibration spectra, motor current, thermal images, geometry under load
Baseline data taken at commissioning is the most underused asset in this industry. Vibration spectra, motor current signatures, thermal images, geometry checks under load — capture them while the machine is new and healthy, and every subsequent condition-monitoring decision has a reference. When a bearing fails in year two and parties argue about whether it was defective at handover, the commissioning baseline answers in minutes. Without it, you argue opinion against opinion, and the customer owns the narrative.
Incomplete commissioning signed off "to keep the programme moving" is the most expensive kindness in this business. Partial tests deferred until after handover, punch-list items closed on a promise, a note that commissioning will be "completed at first planned shutdown" — I have watched each become a warranty claim with the manufacturer holding the burden of proof. The handover certificate lists open items with named owners, dates and consequences, or it does not get signed.
Handover Records: Evidence Written in Advance
A handover pack is not administration; it is the manufacturer's defence and the customer's baseline, written at the only moment both parties are present and objective. As a minimum it contains: the installation record with hold-point signatures, torque logs for critical joints, calibration certificates for every tool and instrument used on site, as-found site condition photographs, commissioning results against acceptance criteria, baseline condition data, all field modifications with engineering dispositions, and the open-items list with owners and dates.
Training the customer's people is part of handover, not a courtesy. Record who was trained, on what, to what depth, and what they acknowledged understanding. I have seen disputes sour because the operator routine the customer adopted in week three would have horrified the design team, and nobody could show what had actually been communicated at handover. A signed training record with a syllabus turns that argument into a fact.
Retention matters as much as content. The handover pack should exist as a controlled document set, versioned, distributed to named recipients, master held under your document control. Loose PDFs in a site manager's inbox are not records. When the claim arrives in year four and the site engineer has left, your ability to produce the exact torque log, the exact vibration baseline, the exact training register separates a defensible position from a settlement.
Handover pack: obligation versus defence
What teams typically do
- Signed certificate with no open-items register
- Photos on a phone, not in a controlled file
- Training delivered but not recorded by name
- Torque values asserted, not logged
- Baseline deferred to first service visit
What survives a claim
- Open items with owners, dates, consequences
- As-found photographs in the controlled pack
- Signed syllabus and attendance register
- Calibrated tool, marked joint, signature per joint
- Baseline captured at commissioning, versioned
Closing the Loop Back to Design
Every site failure is free design intelligence, if you route it. Field modifications especially: when installers across three continents all drill the same bracket, the bracket is wrong, and the installation instruction that failed to anticipate it is wrong too. Feed installation-related nonconformities and field concessions into design reviews and procedure revisions on a fixed cycle, with the site instruction pack reissued and version-controlled.
The alternative is paying for the same defect at every site, forever, and calling it "site conditions". That phrase is where installation quality goes to die, and it is almost always a design-process gap in disguise.
In my experience, products that install badly are rarely designed badly — they are designed by people who have never watched one being installed. Send designers to commissioning, at least occasionally. They will come back with a different drawing, and the quality function will spend far less time explaining how a perfect product ended up as a defective installation.
That is the real lesson of installation quality: the last hundred metres belong to your system or to nobody. Control the site as a process, verify the people as a resource, prove the machine against criteria, and write the evidence before you need it. The manufacturer who does this keeps both the margin and the customer.