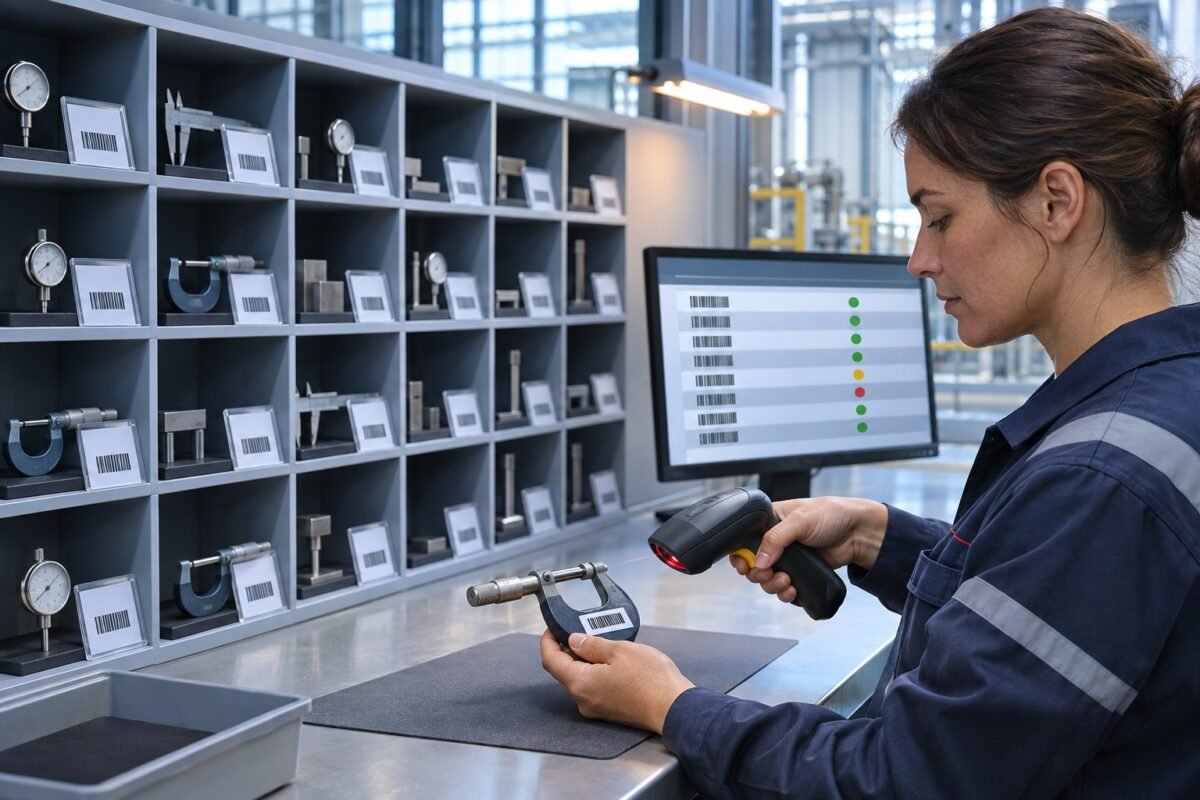
Somewhere in every quality manager's career comes the phone call that begins: a gauge has been found out of tolerance, and it has been used on shipped product. Everything that follows depends on how the gauge management system was designed long before that call. A calibration sticker tells an operator the gauge was good on a given date. It says nothing about who owns the instrument, where it has been, what it measured, or what happens when it fails.
The failure itself is rarely the crisis. The crisis is ignorance: not knowing which parts the gauge touched, which characteristics it verified, and whether the error was large enough to matter. Organisations that survive an out-of-tolerance event with minimal disruption treat gauge management as a traceability system, not a calibration scheduling chore. The sticker is the visible tip; the substance lies underneath, in records that can answer questions within hours rather than weeks of digging.
The machinery that answers those questions has four parts: ownership of each instrument, control of its location, disciplined recall logic, and quantitative impact assessment. Each part is cheap to build and expensive to lack. This article sets out how each works on the shop floor, not in the quality manual.
Ownership: Someone Must Answer for Each Instrument
Every gauge in the plant must have a named owner, and by owner I mean a person or a defined function, not a department in the abstract. When a bore gauge fails its annual check, the first question is who decided it was acceptable to buy, issue and use at that station. If the answer is "quality, probably, or maybe tooling," you have a governance gap that will cost you dearly during an investigation.
Ownership determines the escalation path. In well-run systems, each instrument carries an asset record linking it to a custodian — typically the supervisor of the cell where it lives, or the metrology function for laboratory instruments. The custodian is responsible for routine checks between calibrations, for reporting damage, and for ensuring the gauge is not borrowed informally across shifts. Personal-issue gauges, such as micrometers assigned to individual machinists, carry the individual's name in the system.
I have audited plants where hundreds of hand tools sat in communal drawers with no assignment whatsoever. When one torque wrench failed, the recall scope had to cover every assembly line in the building because nobody could say whose hands it had passed through. Clear custody would have confined the problem to a single cell and a single day of production. Ownership is cheap; the absence of it is not.
Location Control: Knowing Where the Gauge Actually Is
A gauge that cannot be found cannot be calibrated, and a gauge that wanders cannot be recalled. Location control means the system of record reflects physical reality: which crib, which cell, which machine, which toolbox the instrument currently occupies. Check-out logs, crib custody with signed issue, and electronic tracking through barcodes or RFID all serve the same purpose — an audit trail of movement.
The common failure mode is the informal loan. A setter walks to another line, borrows a height gauge, uses it for an hour, and returns it — or doesn't. Six months later the gauge fails calibration, and the recall team must assume it touched work at both locations, doubling or tripling the affected population. Worse is the gauge that leaves the plant entirely, travelling with a field service technician or to a supplier for trial tooling, and returns with unknown history.
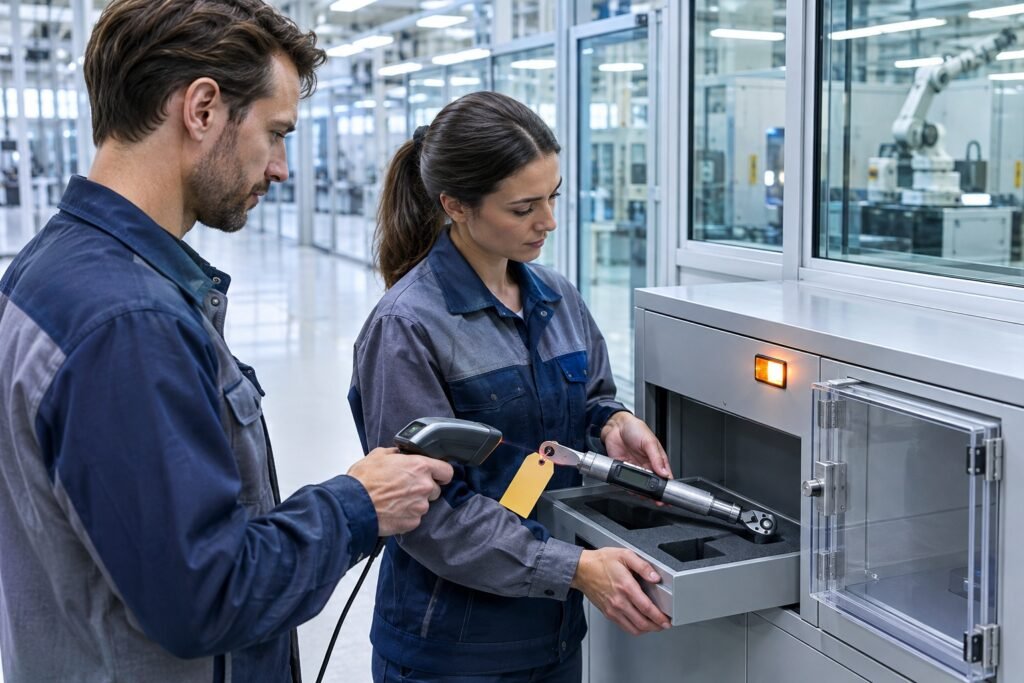
Practical control does not require exotic technology. A gauge crib with disciplined issue and return, movement logged at the point of transfer, and periodic physical audits against the database will catch most drift between records and reality. What matters is that someone reconciles the list against the shop floor on a schedule, and that discrepancies are treated as findings rather than clerical noise. An unaccounted-for gauge is a live recall risk sitting in a drawer.
What Out of Tolerance Actually Means
When a calibration lab reports a failure, the first engineering task is interpreting it, because out of tolerance is not a binary fact. The lab reports the as-found condition: the deviation of the gauge against a reference standard at specific points. A micrometer reading five microns high at the twenty-five millimetre point is a different problem from one reading twenty microns low across its range, and both differ from a gauge with a worn anvil that reads inconsistently.
Direction and magnitude of error drive the impact assessment. If a gauge reads oversize and was used to accept outer diameters, the accepted parts are actually smaller than recorded — the error works against you. If the same gauge verified inner diameters, the error works in your favour. You must reconstruct the sign of the error against each characteristic the gauge checked, in the orientation it was used; assuming the worst case in every direction wastes margin you actually have.
Then there is tolerance consumption. A gauge with a known error of five microns measuring a feature with a fifty-micron tolerance leaves real margin; the same error against a ten-micron tolerance means the verification was meaningless. This is where records of which part numbers and characteristics each gauge verified become decisive. Without that linkage, every reading the gauge ever took must be treated as invalid — the difference between reviewing a day's production and quarantining three months of it.
Recall Logic: Building the Affected Population
Recall logic is the disciplined construction of the set of parts the failed gauge could have touched. Start with the calibration history: the gauge last passed on a known date, so the exposure window runs from that date to the discovery date. Within that window, you need the usage record. Best practice is that the gauge identifier appears on inspection records, first-off reports, or in the measurement data system, so the population can be extracted by query rather than reconstructed by memory.
Constructing the exposure population
- 01Establish the windowFrom last passing calibration or intermediate check to discovery date.
- 02Extract usageQuery gauge ID against inspection records; fall back to station-level records if unlogged.
- 03Tier by criticalityRank part numbers by characteristic severity: cosmetic, functional, safety or flight-critical.
- 04Rank by error magnitudeScore gauge error against each tolerance, with sign and direction of use.
- 05Sequence re-inspectionHighest risk first; decide whether the event is a nuisance or a reportable escape.
Reality is messier. Hand gauges are often used without logging the gauge ID against each check, and you fall back on the station: everything produced at that cell during the exposure window that required the characteristic in question. This is where location control pays for itself. A wandering gauge forces conservative assumptions that balloon the population, and conservative assumptions in recall mean re-inspection, containment, and sometimes customer notification on a scale the actual risk never justified.
Recall must also consider severity tiering. A cosmetic dimension verified by the failed gauge warrants a different response than a safety-critical torque or a flight-critical fit. Rank the affected part numbers by characteristic criticality, then by the magnitude and direction of the gauge error against each tolerance. That ranking drives the sequence of re-inspection and tells you quickly whether the event is a nuisance or a reportable escape.
Impact Assessment: Deciding What Actually Needs Doing
Once the population is defined, the assessment turns quantitative. The core question for each characteristic: given the gauge's known error, could a part outside specification have been accepted? Where the error was small relative to the tolerance and worked in the safe direction, you may conclude with documented engineering rationale that no nonconforming product could have passed. That justification must be in writing with the as-found data attached, because your customer's quality representative will ask for exactly that.
Where doubt remains, re-measure. Sample retained parts from the window — covering the beginning, middle and end of the exposure period — using a calibrated reference instrument with adequate resolution, typically a rule of ten to one for the tolerance being verified. If retained samples are unavailable, fall back on finished-goods stock and, in the worst case, field product. The re-measurement results either close the event or confirm an escape; that decision point, re-verify versus notify, is the heart of the assessment.
An undocumented impact assessment is worth nothing in an audit three years later — the rationale, the data and the names must exist on paper.
Do not skip review of the verification process itself. Check whether the gauge was zeroed or set against a master at each use, because a setting-master check may bound the error more tightly than the calibration interval suggests. Conversely, look for signs of in-service damage — a drop, a crash against a fixture — which can shift the failure point well before the scheduled calibration. And document everything: rationale, data, decision, and the names of those who made it.
Hardening the System After the Event
Every out-of-tolerance finding should shorten the next one's exposure window. The most direct lever is calibration interval adjustment: a gauge that passed with wide margin for years may justify extension, while one that failed warrants shortening until it demonstrates stability. Interval adjustment should be driven by as-found results across the gauge population, not by a fixed calendar someone chose a decade ago.
The second lever is between-calibration verification. Daily or weekly checks against a setting ring, a gauge block or a reference master — logged, with limits — catch developing wear and damage long before annual calibration does. These intermediate checks must themselves be controlled: the master needs its own calibration, and the check limits must be tighter than the gauge tolerance so the check has meaning. Where a gauge verifies tight tolerances continuously, consider redundancy: two gauges cross-checked against each other, so a single failure is caught by disagreement.
Sticker-driven versus traceability-driven gauge management
Calibration scheduling mindset
- Gauge list with due dates and stickers
- Ownership dissolved into a department
- Movement informal and unlogged
- Recall scope set by worst-case assumption
Traceability mindset
- Asset record with named custodian per gauge
- Crib issue, return and physical audit reconciled
- Gauge ID captured on inspection records
- Exposure window bounded by usage data, not memory
Finally, close the loop on systemic causes. Was the gauge used outside its intended range? Was it stored where temperature swings or coolant mist could affect it? Did the purchase specification match the tolerance it was asked to verify? An out-of-tolerance gauge is a symptom; the durable fix usually lies in how the instrument was selected, stationed and handled.
Treat each event as free tuition about your measurement system. A plant that adjusts intervals, adds intermediate checks and fixes custody gaps after every finding will find that the next phone call — and there will be a next one — is a manageable engineering exercise rather than a crisis of ignorance.