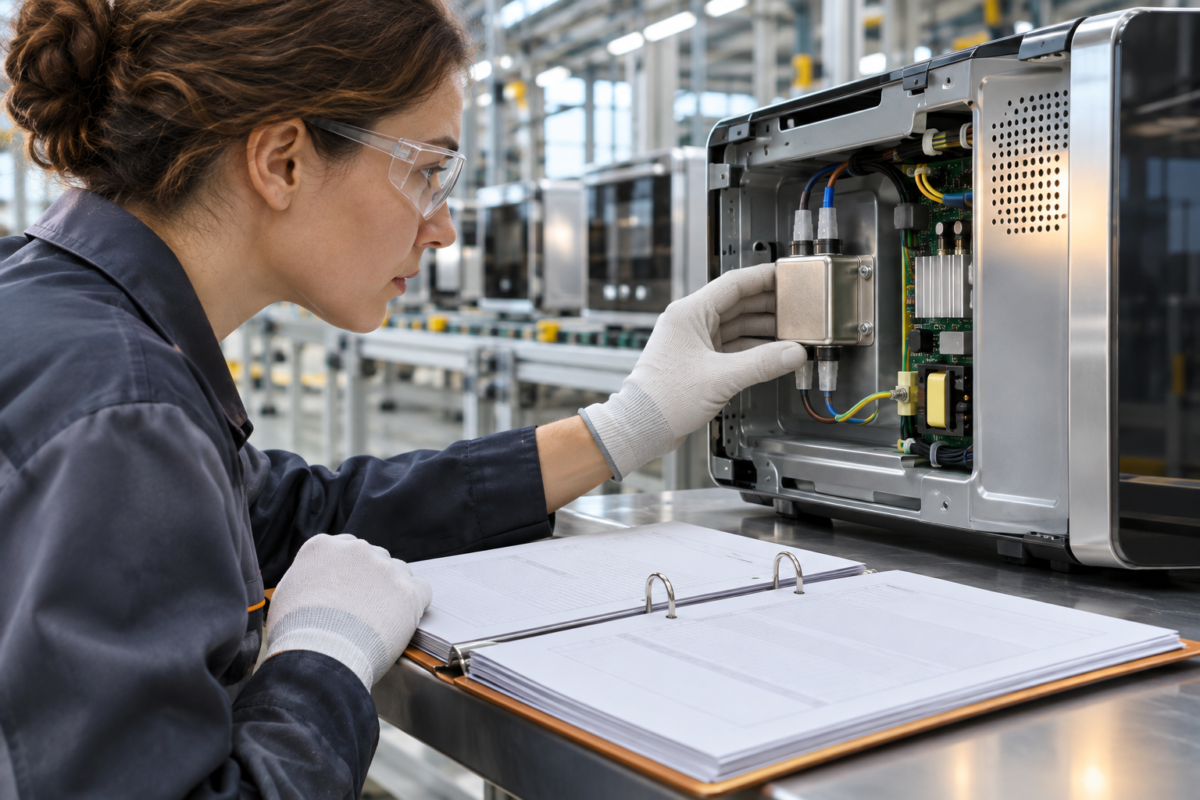
I have sat through certification body audits where everything was in order — the file, the tests, the factory — until the auditor picked up a production unit, compared it against the certified construction file, and found a different component inside. Nobody had done anything malicious. A purchasing manager had approved a substitution during a supply shortage, engineering had signed it off as form, fit, function equivalent, and the certificate had, in effect, ceased to cover the product being shipped.
That is the quiet failure mode of product safety certification: it does not lapse loudly, it erodes one undocumented change at a time. The certificate is evidence about a specific construction, produced at a specific site, at a specific time. Every change that touches that construction without passing through the certification body weakens the evidential chain that the whole scheme rests on.
This article covers the mechanics of keeping a certificate alive through design change: what the certificate actually certifies, how to build a notification process that holds, what follow-up inspectors really examine, the problem of unauthorised modification after delivery, firmware as a moving target, and recovery when compliance has already slipped. I assume you have dealt with a notified body or certification body and know the basics of a conformity assessment scheme.
What the Certificate Actually Certifies
Be precise about the object of certification. A product safety certificate — whether issued under a European directive, a North American scheme, or a sector-specific regime — covers a defined construction: a specific bill of materials, specific safety-critical components, specific drawings, and a specific manufacturing location, each documented in the certification file. The type tests that underpin the certificate were performed on that construction.
Change any element the tests depended upon and the evidential chain breaks, even if the product still works and looks identical from the outside. Most schemes therefore define categories of change. Non-safety-relevant cosmetic changes may need no notification. A change to a safety component — a fuse rating, an insulation barrier, a locking mechanism, a pressure-bearing wall thickness, a firmware safety routine — normally requires notification to the certification body before implementation, sometimes with re-testing or an engineering assessment.
The critical word is before. Implement first and notify later is, in the eyes of most schemes, placing an uncertified product on the market. The failure I see repeatedly is optimistic classification: a mains filter swapped for a different manufacturer's part with identical electrical ratings is treated as trivial. But the filter's creepage distances, flammability rating, and fault behaviour were part of the certified construction. Whether the substitution is acceptable is the certification body's judgement, not the design engineer's. Your internal equivalence assessment is an input to that judgement, not a substitute for it.
Building a Change Notification Process That Holds
The notification obligation fails in predictable places. The most common is the boundary between engineering and purchasing. Engineering owns the certified bill of materials, but purchasing executes substitutions, often under delivery pressure, through channels that never touch the certification file. Unless the engineering change process has a mandatory gate — a signed determination of whether the change touches the certified construction — substitutions will leak through.
That gate must be hard: no purchase order release for a certified part number's replacement until the determination is recorded. And the determination needs competence behind it. Someone must map each proposed change against the certification file: does it affect a listed safety component, a tested parameter, a declared rating, or a critical process at the certified site? In my experience this works best as a named certification coordinator per product family, not a committee. Committees diffuse responsibility; a named person with access to the file and authority to hold a change carries it.
Then track the notification itself. Log the submission date, the reference, the body's response, and any conditions attached. I have audited files where notifications were sent, responses arrived demanding additional documentation, and the responses were filed without action. The product kept shipping on the strength of the original certificate while the change was still under review. That gap — notified but not approved — is where many enforcement actions originate, because it demonstrates the company knew the change required assessment and shipped anyway.
The change control gate for certified constructions
- 01Change proposedEngineering modification or purchasing substitution — both enter here.
- 02Certification impact determinationNamed coordinator maps the change against the certification file.
- 03Not certified-relevantProceed through normal engineering change process.
- 04Certified-relevantNotify the body before implementation; hold the purchase order.
- 05Assessment and releaseRe-test, engineering assessment, or acceptance recorded; construction file updated.
Follow-Up Inspections: What the Inspector Actually Examines
Follow-up inspections — annual factory inspections under a mark scheme, or surveillance visits under a directive module — share one structure: the inspector verifies that production at the certified site still matches the certified documentation. Expect the inspector to walk the line with the construction file in hand, checking safety-critical components against the listed part numbers, manufacturers, and ratings. Label checks follow: markings, warnings, rating plates, and the certification mark itself, including format and file numbers. Random sampling from finished stock, not your prepared showcase samples, is standard practice.
Production consistency tests are usually part of the visit. Depending on the product category, the inspector may witness routine tests — dielectric strength, earth continuity, torque on safety fasteners, functional checks of protective interlocks — against the routine test procedure recorded in the file. If the routine test records show gaps, or the test equipment has no calibration evidence, that is a finding regardless of whether the product itself is compliant. The inspection examines your ability to demonstrate conformity, not merely the fact of it.
Prepare by doing the inspection to yourself first. Pull finished units from stock at random, dismantle them, and compare every safety-critical component against the file. Do this quarterly rather than annually, because it catches drift — the resistor that changed value when old stock ran out, the enclosure moulding that shifted tool shops. Drift is rarely deliberate. It accumulates through expediters, deviations, and verbal approvals, and self-audit is the only reliable way to find it before the inspector does.
When findings occur, respond with evidence, not intent. A nonconformity about an unlisted component is closed by restoring the certified component or completing the notification and assessment. A records nonconformity is closed by implementing the missing control and demonstrating it over a period. What escalates a routine finding into suspension is usually the discovery that the change was known, undocumented, and repeated — a pattern rather than an event.
The inspection examines your ability to demonstrate conformity, not merely the fact of it.
Unauthorised Modifications After Delivery
The certificate covers the product as placed on the market. What happens afterwards is a grey zone manufacturers ignore at their peril. Installers, service technicians, and end users modify products: higher-rating fuses fitted to stop nuisance tripping, interlocks bypassed to speed maintenance, firmware reflashed with regional variants, load-bearing brackets drilled for convenience. If a modification causes an incident, the investigation will examine whether the manufacturer took reasonable steps to make modification difficult, detectable, or clearly prohibited.
Practical controls exist on several levels. Physical: security screws, tamper-evident labels over joint lines, potting or encapsulation where the scheme permits, firmware with signed images that reject unauthorised code. Documentary: explicit prohibitions in the instructions for use, with the safety rationale stated plainly rather than in legalese — people bypass interlocks when they do not understand what the interlock protects against. Contractual: for professional channels, terms that void certification status upon modification and require returned units to be inspected for tampering before service or resale.
Service and repair deserve particular attention. If you authorise repair through a network, repairs must restore the certified construction — original part numbers or approved equivalents that have themselves been through the change process. A repair operation fitting compatible third-party components is creating unauthorised modifications under your brand name. Audit the service network the way you audit production: sample repaired units, dismantle them, compare against the file. Incidents traced to repaired units reflect on the name on the mark, whatever the contract says.
Firmware and the Moving Target Problem
Software introduces a complication older schemes handled poorly: the certified product can change after shipment without anyone opening the case. An over-the-air update or a service-visit reflash can alter safety-relevant behaviour — thermal cutoff thresholds, motor torque limits, fault reaction times — while the physical construction stays identical. Most modern schemes now require that safety-relevant software versions be declared and that changes follow the same notification pathway as hardware.
Internally, this means the software release process must be connected to the certification process, and in many organisations it simply is not. Firmware teams work on continuous delivery cadences; certification operates on assessment cycles. The bridge is a defined classification of software changes: which modules and parameters are safety-relevant per the certification file, and therefore gated, versus which are free to update. That classification must live in the build system as an enforced control, not in a document nobody in the firmware team has read. Where I have seen this done well, the build pipeline physically blocks release of a changed safety module until the certification coordinator clears it.
Verification on the ground matters too. During follow-up inspections and service audits, check installed firmware versions against approved versions. A unit in the field running an unapproved safety-relevant build is an unauthorised modification, even if you shipped it that way by accident. Keep records of which serial numbers received which versions: when an update changes safety behaviour, you may be obliged to notify the authority or initiate field action, and you cannot do either without traceability.
Recovery When Compliance Has Already Slipped
Suppose an inspection or internal audit reveals that products shipped for months contain changes never notified to the certification body. The temptation is to quietly fix the construction going forward and hope nobody connects the shipped population to the file. Resist it. Certified products in the field with undeclared safety-relevant changes are a potential safety exposure, and most schemes require — and all regulators prefer — proactive disclosure. A voluntary notification with a structured assessment of the change's safety impact is treated very differently from concealment discovered by the authority.
The recovery sequence is straightforward in outline: freeze further shipments of the affected construction; assess the change against the original type tests to determine whether engineering analysis can show equivalence or retesting is required; notify the body with a complete package — change description, affected serial ranges or date codes, your assessment, your proposed disposition; then decide with the body whether field action is needed, from none through documentation update and customer notice to recall in the serious case.
Concealment versus voluntary disclosure
Quietly fix forward
- Change corrected without notification
- Shipped population left unassessed
- Finding repeated at next inspection
- Escalation risk: suspension and market action
Disclose and assess
- Shipments frozen pending assessment
- Safety impact evaluated against type tests
- Body notified with serial ranges and disposition
- Systemic cause corrected with the rigour of an 8D
Finally, close the systemic hole. The individual change is a symptom; the finding you should expect from your own investigation is that the classification gate failed, the certification coordinator role was vacant, or purchasing had a substitution path that bypassed engineering. Fix the process with the same rigour you would apply to a production nonconformity, because in certification terms that is exactly what it is. A certificate is not a trophy for passing a test once — it is a standing claim that today's product, from today's line, is the one that was tested. Keeping that claim honest is daily work, done one change at a time.