Foreign object damage is the only quality failure mode I know where the root cause is almost never technical. The missing socket, the wire offcut left inside a wing rib, the swarf beneath a fixture: each traces back to a person deciding, in a moment of fatigue or hurry, that the control in place was optional just this once. That is why FOD prevention cannot be delegated. You can assign tool cribs, audits and clean-as-you-go duties to supervisors, but the moment the plant manager stops asking about FOD, the programme begins to die.
It dies quietly, over months, and the first evidence is rarely a crash or a rejected engine. It is a shadow board with a gap nobody has chased for three days. Across two decades in automotive and aerospace quality, running FOD programmes in engine assembly, transmission machining and aerostructure build, I have watched the same pattern everywhere: launched with energy after an incident or a customer escape, plateauing for a year or two, then decaying into paperwork while the audits still happen and the forms still get signed.
This article is about what that erosion looks like, how to catch it, and what genuinely works at the bench. The mechanics are unglamorous — boards, logs, bins, boundaries — but each one closes a specific physical question: is every object accounted for, or is one of them inside your product?
Tool control as the foundation
Everything begins with knowing, at any moment, exactly which tools exist and where they are. The cheapest reliable method is still the shadow board: a silhouette or outline for each tool, and a rule that an empty silhouette at end of shift means the tool is accounted for before anyone goes home. The board only works if the silhouette is unique per tool, including size variants. Two 13 mm sockets from different sets must not be interchangeable on the board, because the moment they are, the board stops telling you whether a tool is missing or merely replaced by its twin.
Etching or engraving tools with a location code is the discipline most plants skip and most regret. A foreign object recovered during inspection is nearly useless as evidence unless you can trace it to a station, a shift and a person. Engrave the station code and tool number into the tool itself — laser marking survives solvents; paint pens do not. Calibrated tools, torque wrenches and gauges need a second layer: a check-out log or, better, an electronic cabinet that records who took what and when. The cabinet is optional; the traceability is not. A paper log nobody reviews is worse than none, because it manufactures false confidence.
Audit tool control by hunting its obvious failure modes. Look for tools that have migrated into drawers, toolboxes and coat pockets — the personal toolbox is the classic leak in any controlled area. Look for borrowed maintenance tools that entered the line and never left. Check that broken tools are swapped through a formal concession: the broken half goes into quarantine, the replacement is logged, and the scrap piece is physically matched. A fractured drill bit where only seven of eight fragments are recovered should stop the job until someone finds the eighth.
Shadow boards that actually get used
A shadow board fails in predictable ways, and most are visible from five metres if you know what to look for. Silhouettes painted around tools that have since been replaced with different sizes. Tools hanging on nails because the proper clip broke months ago. Boards positioned behind machinery where nobody sees them during shift handover. The board must sit in the line of sight of the person working the station — if the operator has to walk to check it, the check will not happen under production pressure.
Colour-coding by area or product family earns its keep in plants running multiple programmes. Tools used only on a high-cleanliness assembly — a hydraulic module, a fuel system — can be marked in a distinct colour so a stray tool from general machining is immediately conspicuous among them. The same logic applies to consumables: cutters, inserts, deburring blades and scribers need a defined home and a defined count. I insist on consumable counts at every shift change in FOD-critical zones. A missing craft knife blade is as dangerous as a missing socket, and considerably harder to find.
The audit evidence is straightforward. Photograph the board in its approved state, keep the photo at the station, and audit against the photo rather than memory. Record the result on a log at the board itself: date, auditor, discrepancies found, and critically, the date each discrepancy was closed. A board log with open items older than a week tells you the escalation path is dead. When I walk a line, I read those logs before I look at anything else; they tell me whether FOD is managed or merely monitored.
The board audit loop
- 01PhotographCapture the board in its approved state and post the photo at the station.
- 02CountVerify every silhouette against the physical tool by count, not by glance.
- 03RecordLog date, auditor and each discrepancy on the sheet at the board.
- 04CloseEscalate any finding open past seven days to the plant manager personally.
Clean-as-you-go and the rhythm of removal
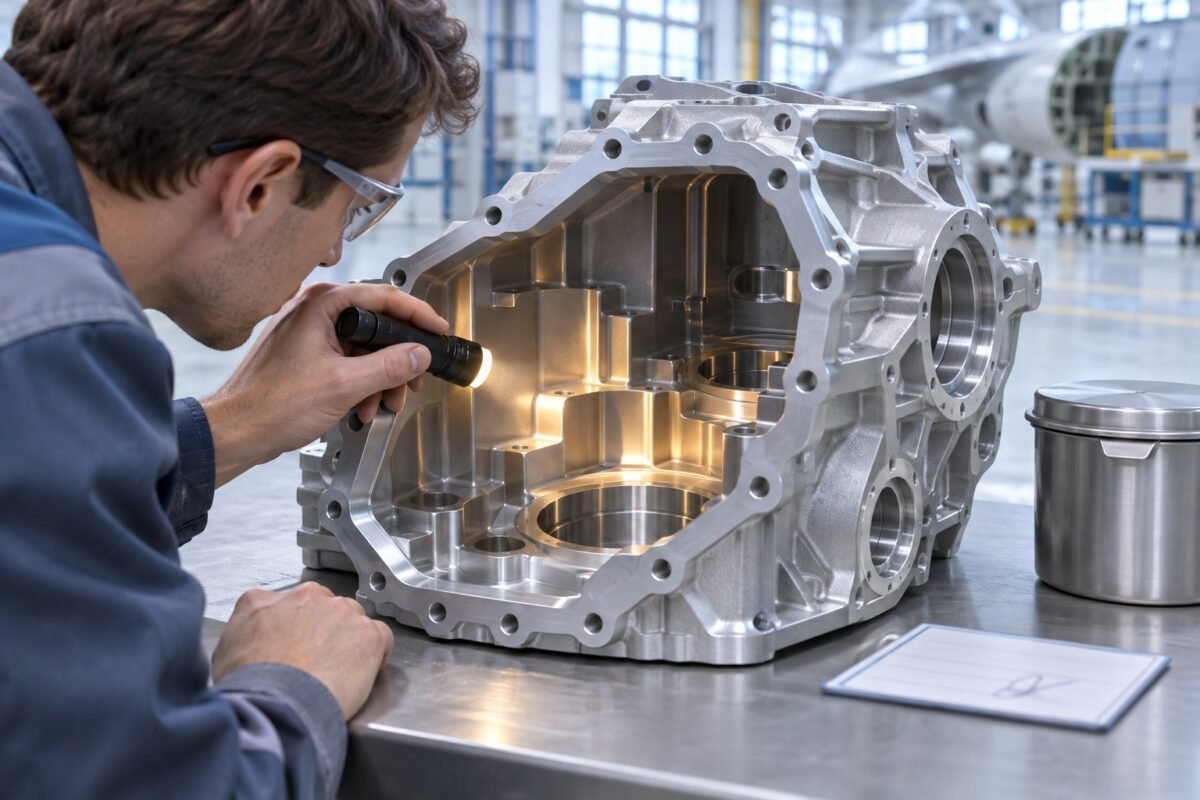
Clean-as-you-go is not a slogan; it is a defined sequence of removal operations built into the work instructions. Deburring an aluminium housing? The instruction should specify where the swarf goes — a magnetic tray for ferrous offcuts, a lidded bin for slivers — and when the tray is emptied. Trimming tie-wrap ends or safety wire? Specify a pouch, and specify that the pouch is emptied at a fixed point in the cycle, not when it is full. Every intervention on an open assembly — a gearbox casing, a wing box, an engine module — should end with a documented visual inspection of the cavity before closure, signed by the person performing it.
The closure inspection deserves particular attention because it is the last line of defence. Teach a repeatable pattern: inspect with a torch at an angle rather than dead-on, because glinting metal catches light obliquely; check ledges, corners and blind pockets where gravity deposits debris; use a mirror or borescope where the eye cannot reach. Require positive confirmation, not a glance. In one plant I ran, we printed the closure check as a separate card per assembly rather than burying it in the routing — the physical act of signing a dedicated card changed behaviour more than any training course had.
Scheduling matters as much as method. End-of-shift cleaning that leaves the last hour's debris overnight simply moves the risk to the morning crew, who now work around yesterday's offcuts. Build removal points into the takt of the job itself: after drilling, after deburring, after fitting. Housekeeping intervals for FOD-critical zones should be defined in minutes or operations, not shifts. And provide the hardware — brushes that shed no bristles, non-shedding wipes, trays with lips, bins with lids. A bristle from a cheap brush is itself foreign object debris; I have seen plenty.
Zone discipline and physical barriers
Cleanliness regimes only function inside a defined boundary. A FOD zone needs a physical perimeter — taped floor at minimum, ideally railed or walled for critical assembly — and a rule that nothing crosses the line unaccounted for. That applies to people as much as tools: personal items, pens, coins, lanyards and badges stay outside or stay secured. I favour the classic pocket-emptying station at the entrance: a rack of small lockers where staff deposit loose items, with clear pockets for anything they must carry in and a count check at exit. Gloves, sleeves and overshoes worn only inside the zone make the boundary visible and self-policing.
Wind, overhead cranes and shared transport are the enemies of zone integrity. Open doors, blown dust and parts trolleys routed through dirty corridors all carry debris into controlled areas. Check the airflow: if extraction pulls air from a machining bay through an assembly bay, you have a systemic contamination path that no amount of sweeping will fix. Incoming parts should be cleaned and verified at the zone boundary, not trusted because they arrived in packaging. I have found machining chips inside sealed supplier bags more than once; sealed does not mean clean.
If a visitor can walk into the zone carrying a biro and nobody says anything, the zone is decorative.
Empower everyone in the zone to stop work over a suspected foreign object, and make sure they have seen that authority exercised in practice. A stopped line over a missing drill bit, resolved and praised, buys years of vigilance. The first time a supervisor overrides a stop because the schedule was tight, you have taught the entire floor what the programme really values. Zone discipline survives on visible consequences, not on the tape on the floor.
Audit evidence: proving the programme is alive
Audits for FOD should follow the object, not the paperwork. Walk the process from goods-in to closure and ask at each stage: what enters, what leaves, what proves it? At goods-in, check the cleanliness verification records against the actual parts. On the line, compare shadow board logs, consumable counts and closure cards against physical reality — pick three boards at random and hunt for every tool by count, not by glance. In finished stock, review the findings from cavity inspections and any foreign objects recovered downstream, including at test. Each recovered object should have a trace record: what it was, where found, likely origin, and the action taken.
The health indicator I trust most is the age of open findings. A FOD audit that produces the same three findings month after month — board gaps, personal tools in the zone, dirty trays — is not an audit; it is a diary of neglect. Require closure dates, escalate anything past seven days to the plant manager personally, and publish the closure performance where the teams can see it. Equally, track the trend in foreign objects found internally versus escapes found by customers or test. Internal finds going up is usually good news: people are looking. Internal finds trending to zero while occasional escapes continue is the clearest possible sign that looking has stopped.
Do not confuse frequency with rigour. A daily checklist ticked in thirty seconds by a harassed supervisor is worth less than a weekly audit done properly with findings escalated. I run light daily checks — board counts, zone boundary, bin lids — and a heavier weekly audit covering tool trace, closure card sampling and consumable reconciliation, with different auditors rotating through, because auditors who always audit the same line stop seeing it. Evidence should also include the negatives: records of tools deliberately out for calibration, broken-tool concessions with both fragments accounted for, and quarantine actions with dates.
A managed programme vs a monitored one
Programme on autopilot
- Audits on the same day, same stations, same auditor
- Boards checked by glance, not by count
- Closure cards signed from memory
- Open findings repeat month after month
Programme alive
- Rotating auditors, varied timing, injected-object exercises
- Counts reconciled against a photo of the approved state
- Dedicated closure card signed at the assembly
- Findings closed within seven days or escalated
The decay curve and how to fight it
FOD programmes die of routine, and the death follows a sequence I have watched several times. First the audits become predictable — same day, same auditor, same stations — and the floor prepares for them. Then the boards are checked against the board rather than against the count, then the closure card is signed from memory, then the programme exists only in the monthly report. Nobody decides this; it happens through a hundred small exemptions granted under delivery pressure. The final stage is a foreign object found at test or, worse, at a customer, and everyone declaring the programme was in place all along, with the paperwork to prove it.
Fighting the decay requires deliberate friction. Rotate auditors, vary timing, and occasionally run an injected-object exercise: place a marked, inert item — a numbered washer from your own crib, logged beforehand — into a cavity or on a fixture and see whether the process finds it before closure. Do this rarely and honestly; the objective is calibration, not entrapment, and the results feed the training review, not the disciplinary file. Management visibility is the other lever. When the plant director picks up a foreign object at test and carries it to the morning meeting, the programme gets more attention than any procedure revision ever generated.
Above all, keep the connection between the small controls and the large consequence visible. The socket missing from board fourteen is not a housekeeping issue; it is an unaccounted metal object somewhere in your product or your building, and you will not know which until something finds it for you. Every audit, every count, every closure check exists to close that question before the customer does. That is the discipline — sustained, unglamorous, and incapable of surviving on autopilot. It cannot be delegated to a form, and it cannot be delegated to a department. It can only be kept alive by people who keep asking.