A tier-one supplier receives a PPAP approval and a letter of expectation: reduce PPM by 40% next year, or lose the business. The quality manager translates this into an internal defect-reduction programme. Six months later, PPM has not moved. The reason is rarely the quality system itself. The reason is that the strategic target was never deployed past the supplier's own receiving dock.
In automotive and aerospace supply chains, the critical breakdown in strategy deployment happens at the boundary between two companies. The OEM or tier-one sets a goal. The tier-two nods. Neither party builds a shared mechanism to translate that goal into sub-tier process changes. Hoshin Kanri, deployed across the supplier interface, closes this specific gap.
The methodology forces both organisations to agree on three to five measurable priorities, cascade them through a structured catchball dialogue, and govern execution with monthly PDCA reviews. Applied to the supplier boundary, it replaces the annual question — 'why did you miss your targets?' — with a shared X-Matrix that both parties actively manage.
The Supplier-Boundary Translation Breakdown
Traditional supplier management relies on the quality agreement and the scorecard. The agreement states the maximum acceptable PPM. The scorecard reports monthly performance against it. Both documents are necessary, but neither deploys strategy. They report lagging outcomes after the defective parts have already shipped.
The first mechanical failure is translation. An OEM target to reduce warranty claims by 25% is a financial metric. It means nothing to a sub-tier stamping operator. That operator needs to know the process parameter that must change at their press to prevent a dimensional drift. The translation chain from OEM warranty data to sub-tier machine settings is where most strategy dies.
The second failure is the assumption of unilateral capability. The tier-one assumes the tier-two has the engineering resources to independently decode a vague quality directive. Most sub-tier suppliers, especially in lower tiers, do not have dedicated advanced quality engineering teams. They need the target broken down into specific process-level actions, not a letter demanding improvement.
The third failure is feedback. Without a structured joint-review cycle, there is no PDCA across the boundary. The tier-two encounters a technical barrier — a worn tool, a material inconsistency — and silently absorbs the deviation. By the time the tier-one's scorecard catches it, the strategic window has closed.
Structuring Cross-Company Catchball
Catchball across the supplier interface requires a fundamental shift in posture. The tier-one does not throw a target over the wall. The tier-one presents the strategic priority and the underlying business case, then asks the tier-two a direct question: what would it take to achieve this in your process? The dialogue must involve the technical leaders from both sides, not just commercial buyers and sales managers.
The ball throws back up. The sub-tier supplier reports operational realities that the customer never considered. A PPM target of 50 requires a new inline gauge, a capital expenditure the supplier cannot fund alone. A cycle-time expectation conflicts with the Cpk requirement on a critical characteristic. This pushback is the entire point. Catchball calibrates the strategy against shop-floor physics.
In my experience auditing supplier quality systems across aerospace and automotive, the organisations that hit their improvement targets are the ones where the customer's SQE sat with the supplier's process engineer and rebuilt the PFMEA together. That collaborative PFMEA review is catchball in practice. It translates a customer-level metric into a prioritised list of process controls.
Cross-Boundary Catchball Sequence
- 01Priority and case presentedTier-one shares the business driver behind the target, not just the number.
- 02Technical constraint mappingSub-tier identifies process limitations, equipment gaps, and resource needs.
- 03Target and timeline calibratedBoth parties adjust the goal based on validated shop-floor reality and capex constraints.
- 04Joint X-Matrix builtCustomer and supplier agree on specific actions, owners, and deadlines.
- 05Shared monthly PDCAJoint review of barriers and progress, not a unidirectional performance report.
The Shared X-Matrix at the Interface
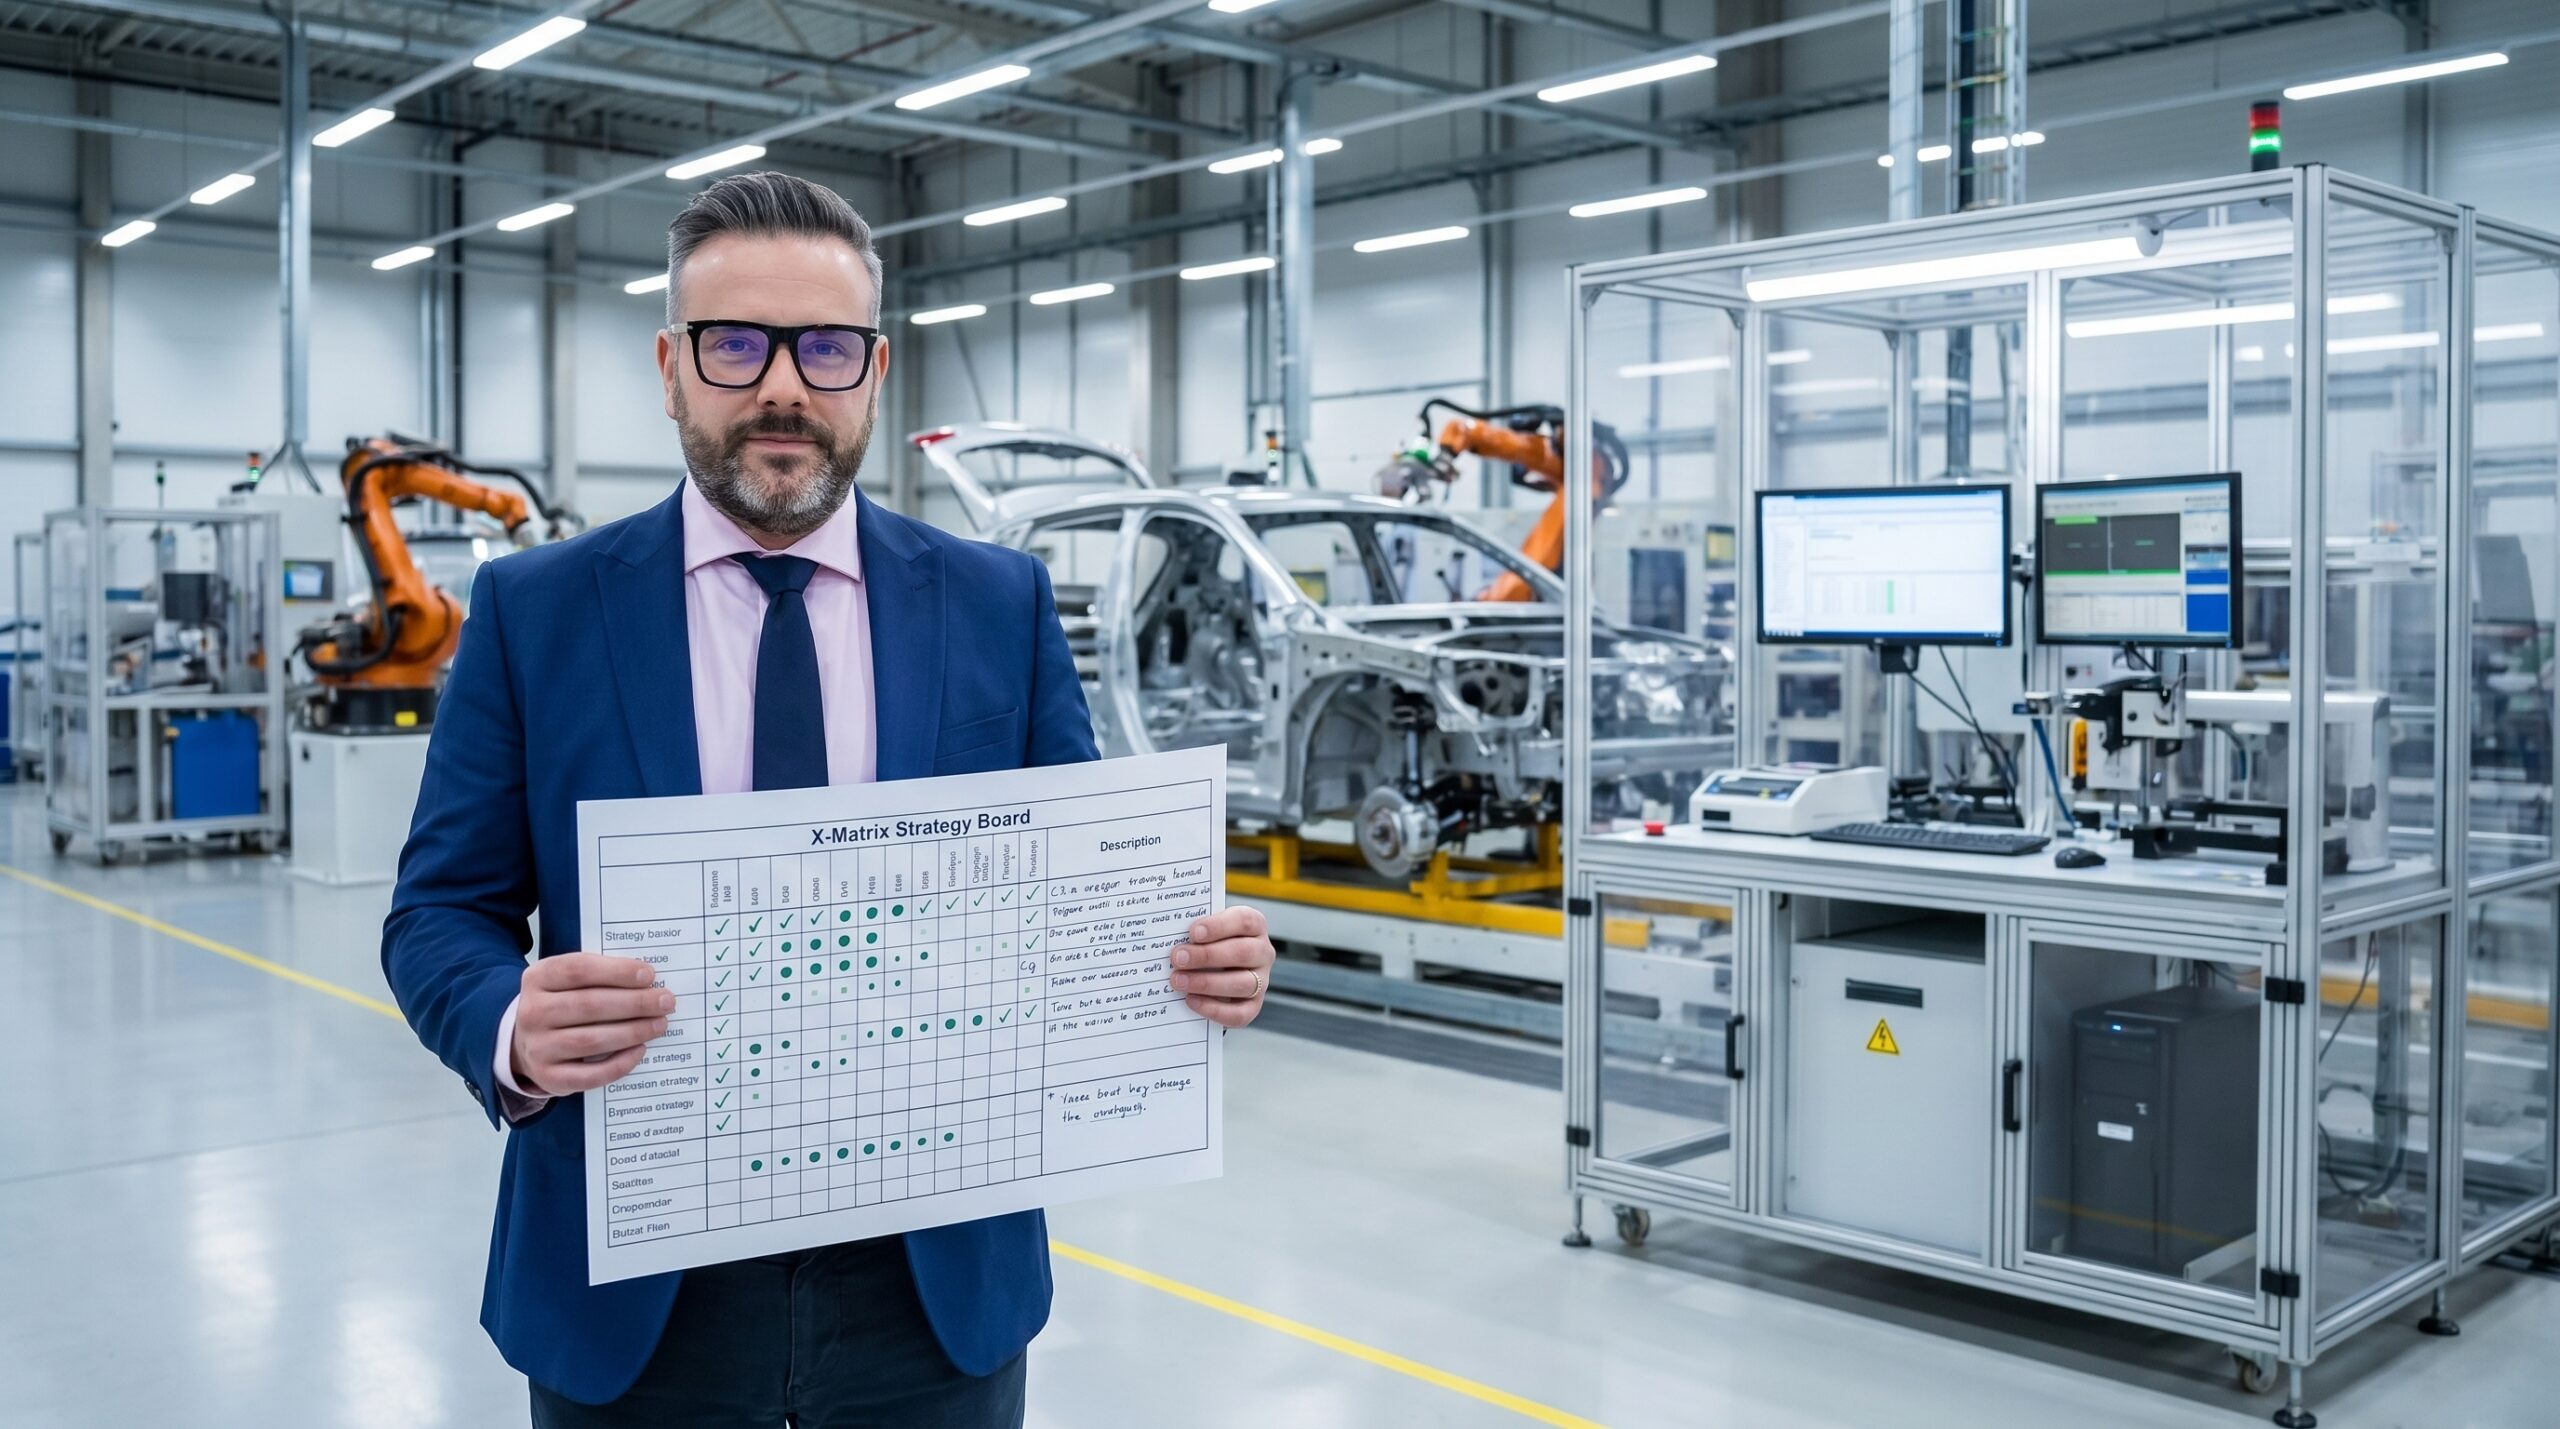
The X-Matrix is a single-page A3 document that forces explicit alignment. South quadrant holds the three to five strategic priorities agreed for the year. West lists the specific improvement targets. North captures the quantified metrics. East defines the action plans. The centre maps the relationships. At the supplier interface, this document is co-authored.
A shared X-Matrix eliminates the ambiguity that plagues supplier quality agreements. The tier-one commits specific resources: engineering support, tooling funding, a capacity reservation. The tier-two commits specific process changes: tightening a temperature tolerance, implementing SPC on a previously unmonitored station, running a DOE to optimise a weld parameter.
The filtering function of the X-Matrix is its most underused feature. If a proposed supplier activity has no dot connecting it to a customer-driven strategic goal, it triggers a question: why are we investing engineering hours in this? The matrix becomes a prioritisation tool that disciplines both the customer's escalation requests and the supplier's internal projects.
This document replaces the traditional corrective-action theatre. Instead of waiting for a nonconformance and issuing an 8D, both parties manage the leading indicators on the matrix. The 8D still exists for containment, but the X-Matrix prevents the systemic drift that leads to the nonconformance in the first place.
Governing the Boundary With Monthly PDCA
A shared X-Matrix without monthly governance is decorative. The monthly PDCA review is where strategy deployment survives or collapses. This review is not the standard supplier business review, where the SQE presents a scorecard and demands explanations for red metrics. It is a structured problem-solving session focused on barriers.
Both parties bring data. The supplier reports progress on the committed process changes. The customer reports on their own commitments: did the engineering support arrive on time? Did the tooling funding clear? If the customer's actions are delayed, the supplier's dependent actions slip. The PDCA cycle exposes these dependencies early.
If the customer's own actions are delayed, the supplier's dependent actions slip. Joint PDCA exposes this before the target month arrives.
The review follows the standard PDCA logic. Plan: verify the action plan for the next 30 days. Do: confirm what was executed since the last review. Check: analyse the gap between expected and actual metric movement. Act: adjust the plan, escalate resource needs, or re-sequence activities. The output is an updated X-Matrix, not a set of meeting minutes.
Annual reflection closes the loop. At year-end, the review shifts from tactical barrier removal to systemic evaluation. Did the catchball process produce realistic targets? Did the shared X-Matrix drive the right behaviours? The goal is to improve the joint deployment mechanism itself, strengthening the partnership for the next strategic cycle.
Interface Failures and Misapplications
The most destructive failure is simulated catchball. The tier-one presents a target, schedules a meeting, and dictates the terms. The tier-two nods silently, fearing commercial consequences. No constraints are raised. No resources are negotiated. The resulting plan is a fiction that guarantees a Q4 miss. Real catchball requires the customer to accept pushback without penalising the supplier for honesty.
A second failure is overloading the matrix. In an attempt to be thorough, the joint team lists twenty improvement priorities. The X-Matrix becomes unmanageable, review meetings exceed three hours, and engineering effort fragments across too many fronts. Hoshin Kanri demands three to five priorities. The discipline of saying no to secondary objectives is what makes the methodology work.
Scorecard Management vs. Boundary Hoshin
Scorecard and quality agreement
- Lagging PPM metrics reported monthly
- Unilateral target dictated by customer
- Reactive 8D cycle for each nonconformance
- Transactional relationship with penalties
Boundary Hoshin Kanri
- Leading process indicators reviewed jointly
- Targets calibrated through technical catchball
- Proactive barrier removal via shared PDCA
- Co-authored X-Matrix with reciprocal commitments
A third failure is confusing Hoshin with daily supplier management. The X-Matrix targets the critical breakthroughs — reducing a specific failure mode, qualifying a new material, achieving Cpk 1.67 on a safety characteristic. It does not replace routine incoming inspection, dock audits, or standard logistics calls. The two systems operate side-by-side, serving different purposes.
Deploying Across the First Interface
Start with one critical supplier and one strategic target. Do not attempt to deploy Hoshin across the entire supply base simultaneously. Select a supplier where the relationship has enough depth to support transparent dialogue — typically a single-source tier-two or a long-term partner producing a high-impact component. Define the goal concretely: reduce scrap on the critical-to-safety dimension by 30% before the next IATF 16949 surveillance audit.
Run the catchball process physically, not over email. The customer's quality engineer and the supplier's process engineer must stand at the machine, review the PFMEA, and identify the true process levers. Build a single-page X-Matrix together. Commit reciprocal actions. Review monthly. At the end of the quarter, measure the result and refine the mechanism.
When this works, the supplier interface stops being a transactional boundary policed by scorecards. It becomes a shared deployment surface where customer strategy translates directly into supplier process control. That is where quality ceases to be a department and becomes the operational mechanism connecting two organisations.