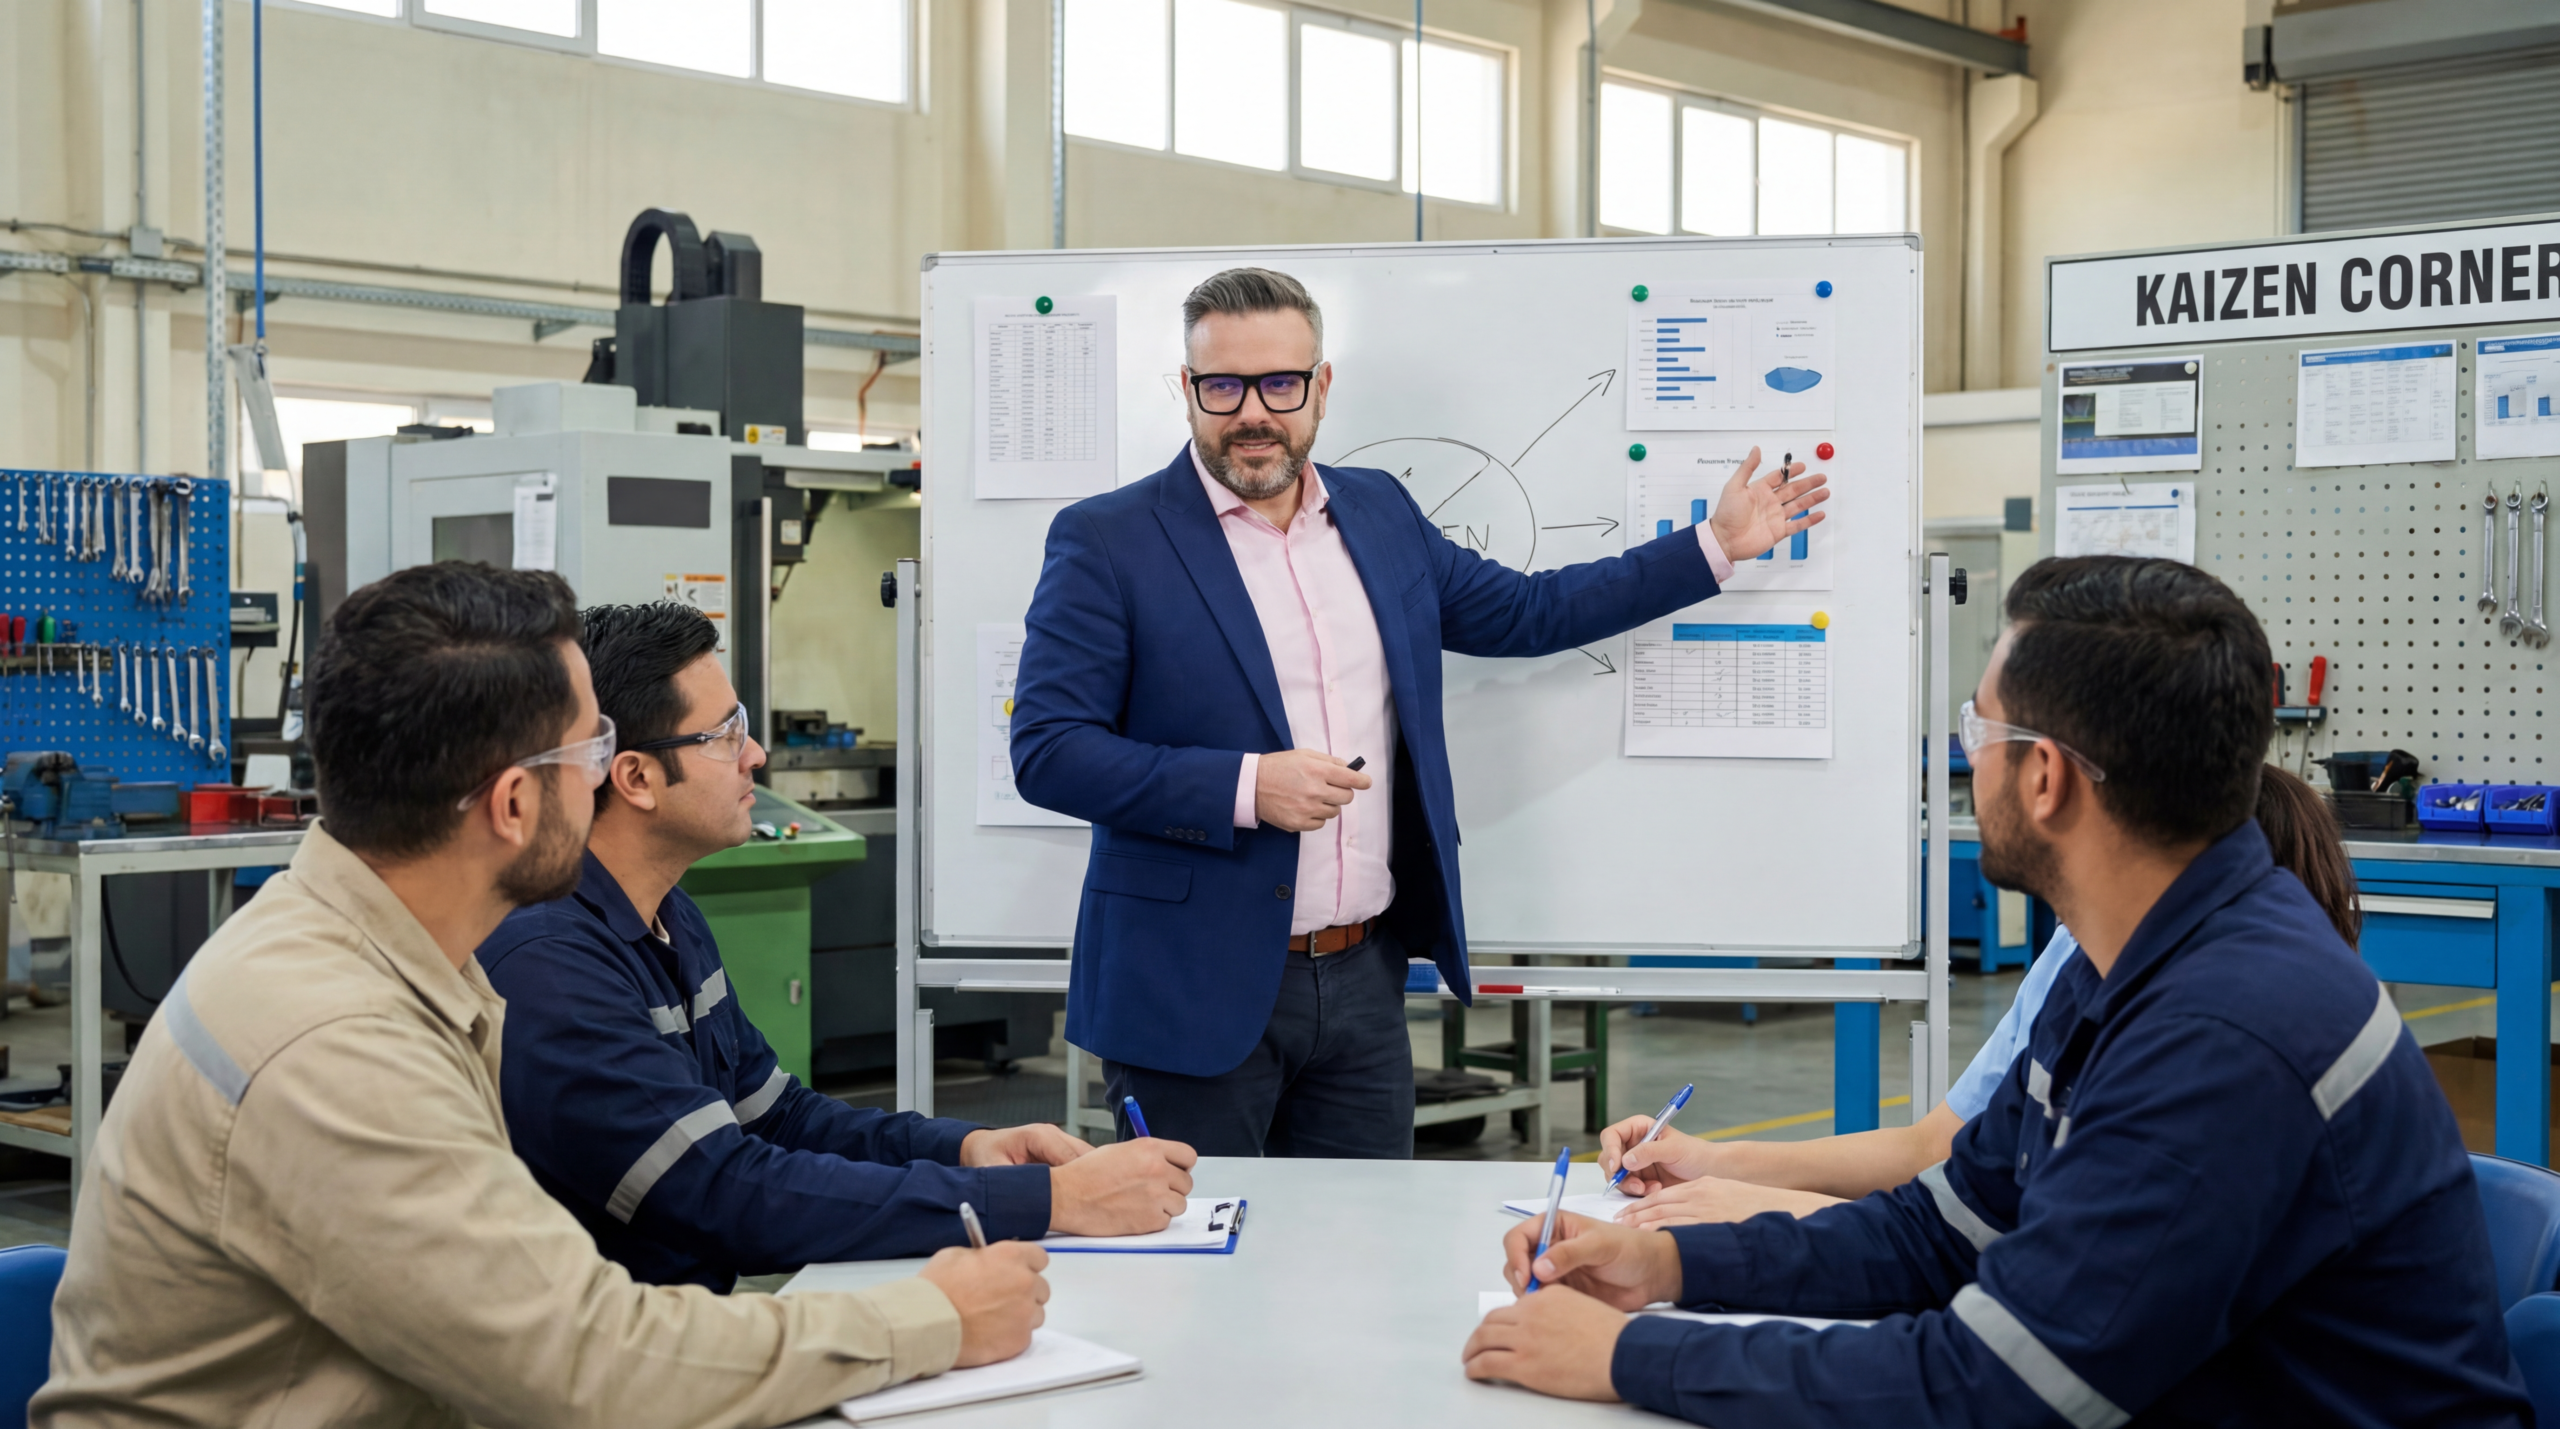
During a plant audit in Nagoya, a quality manager showed me how a single operator's suggestion to reposition a tool saved two seconds per cycle. Individually, two seconds is negligible. Multiplied across a thousand parts per shift, three shifts, and 250 working days, it yields 150,000 seconds. That is roughly forty-two days of liberated production capacity from a single, minor workstation adjustment.
This is the fundamental mechanism of Kaizen. It is not a motivational philosophy or a secondary project tier. It is an operational system designed to capture, evaluate, and implement micro-efficiencies continuously. When properly structured, these minor adjustments push overall equipment effectiveness (OEE) upward without requiring capital expenditure on new machinery.
In my experience implementing IATF 16949 and AS9100 systems, the companies that sustain compliance are those that build improvement mechanisms into the daily routine. They treat standard work as a baseline to be challenged, not a permanent restriction. Kaizen provides the structural framework for operators to challenge that baseline every single day.
Systematic Improvement Versus Point Kaizen
A functioning continuous improvement programme operates on two distinct tracks. The first is Kaizen Teian, or systematic improvement. These are structured, cross-functional projects designed to eliminate major waste (Muda) over one to three months. They require formal root cause analysis, tracked through 8D methodology, and involve engineers, quality technicians, and management.
The second track is Point Kaizen. These are rapid, individual suggestions generated by operators on the shop floor. Implementation takes hours or days, not months. Point Kaizen targets the friction operators feel daily: a tool positioned thirty centimetres too far away, a material delay, or an unnecessarily repetitive motion.
Both tracks must be governed by the same quality rigour. A Point Kaizen that alters a process step still requires an updated Standard Operating Procedure (SOP) and validation under your PFMEA framework. The distinction is the scale of the change, not the absence of quality control.
Improvement Scope: Teian vs. Point Kaizen
Kaizen Teian (Systematic)
- Cross-functional engineering teams
- Timeline of 1 to 3 months
- Targets systemic waste (Muda)
- Requires formal DMAIC or 8D tracking
Point Kaizen (Individual)
- Single operator suggestions
- Implementation within 24 to 48 hours
- Targets micro-friction and motion waste
- Requires rapid review and SOP updates
Extracting Data from the Gemba
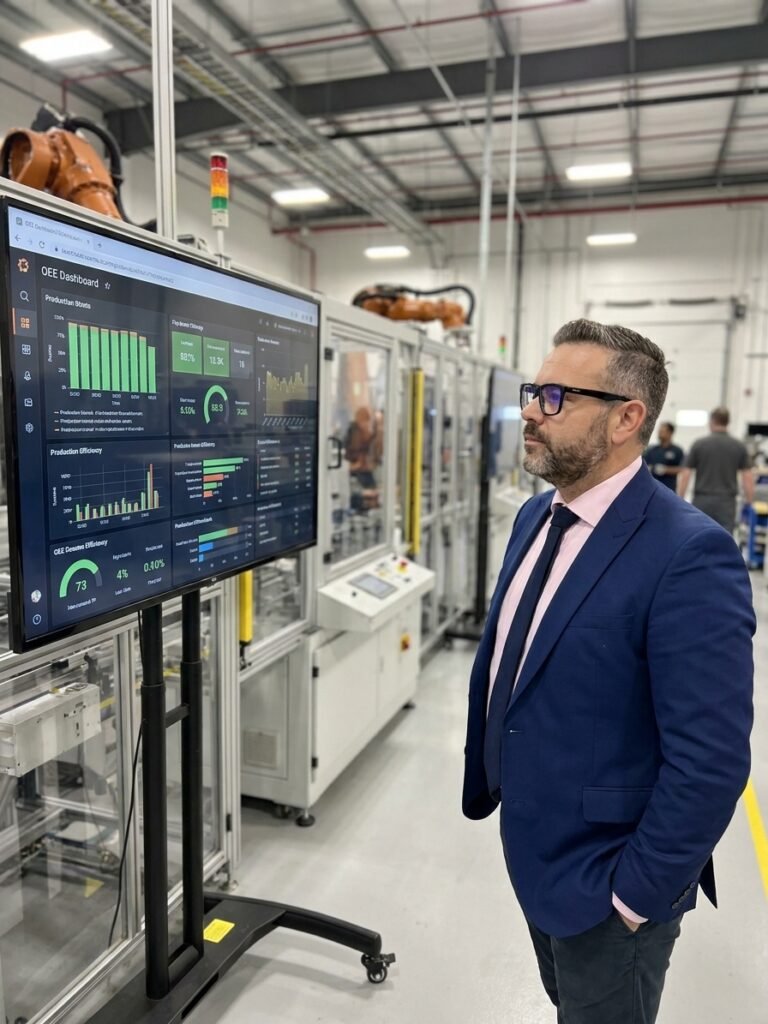
Effective Kaizen relies on direct observation. During the Nagoya audit, I stood at the line and documented the specific friction points. Operator one reached for a tool two metres away three times per cycle. Operator two stood idle for five minutes waiting for the conveyor. Operator three repeated a hand motion ten times per minute unnecessarily.
Engineers frequently design workstations from CAD models rather than physical reality. When you conduct a Gemba walk, you find the realities of the process. A sensor relocated during a breakdown months ago permanently increased reaching distance. The operator compensates for this poor layout thousands of times per week, degrading cycle time and increasing ergonomic risk.
The objective is to train your supervisors to see these micro-stoppages and motion wastes as data. Every unnecessary reach, wait, or adjustment is a deviation from standard work. When operators are empowered to flag these deviations, the shop floor becomes your most accurate data collection network.
The Operator Feedback Mechanism
Management does not dictate Point Kaizen suggestions; it facilitates them. The operator knows the tool is poorly placed because they feel the strain eight hours a day. The engineering task is to ask why the friction exists and authorize the physical change. In Nagoya, relocating a tool rack by thirty centimetres saved half a second per operation.
This requires a formalised submission mechanism. A basic Kaizen card captures the problem, the proposed solution, and the baseline cycle time. Management must review these cards within twenty-four hours. If the suggestion is rejected, the operator receives a clear engineering explanation. If approved, implementation occurs immediately.
Slow approval cycles kill continuous improvement cultures. If an operator submits a card and hears nothing for three weeks, the programme is dead. Speed is the critical metric for management. A fast rejection with technical reasoning builds more trust than a delayed approval.
Slow approval cycles kill continuous improvement cultures. Speed is the critical metric for management.
Validating and Measuring the Impact
Every Point Kaizen must be measured before and after implementation to validate the actual impact. Estimates are insufficient. When the tool rack was moved, the cycle time was re-timed physically. The half-second saving per operation was verified, multiplied by three operations, and locked into the revised SOP for the station.
Aggregating these micro-savings reveals substantial operational capacity. In the Nagoya example, three individual operator suggestions reduced the total cycle time by 3.3 seconds. Across three shifts over a full year, this compounded into an extra eighty-six days of production capacity, achieved with a total hardware investment of roughly three hundred and fifty dollars.
These savings must be reflected in your KPI dashboards. When Cpk improves because a workstation change reduced operator fatigue and variation, document the correlation. This proves to executive management that operator-driven Kaizen directly supports quality compliance and IATF 16949 requirements, not just production speed.
| Operator Change | Per-Cycle Saving | Annual Time Recovered |
|---|---|---|
| Tool rack repositioned 30 cm | 1.5 seconds | 31.25 days |
| Conveyor low-level sensor added | Eliminated 5 min wait | 26.04 days |
| Redundant hand motions engineered out | 1.8 seconds | 28.71 days |
| Total Aggregated Capacity | 3.3 seconds / cycle | 86 days |
Sustaining the Kaizen Framework
Continuous improvement fails when it is treated as a temporary initiative. It must become an integrated routine governed by visible metrics. Establish a physical Kaizen board directly on the shop floor. Track the number of submissions, approval rates, implementation speed, and verified time savings. This visibility drives competition and engagement across shifts.
Recognition is mandatory. Publicly acknowledge the operator on the board, present the financial or efficiency impact, and provide a tangible reward. This proves to the workforce that management values their technical expertise. Without this feedback loop, the submission rate will drop to zero within a quarter.
Finally, integrate Kaizen into your internal audit schedule. During ISO 9001 surveillance audits, be prepared to demonstrate not just your SOPs, but the revision history of those SOPs driven by operator suggestions. An auditor wants to see a living quality management system. A documented trail of Point Kaizen improvements is the strongest evidence of a functioning, compliant system.
Implementation Timeline and Rollout
Do not launch a Kaizen programme with a mandate to implement everything at once. Structured rollout prevents operational chaos. The first week is preparation: establish the boards, print the submission cards, and train management on the twenty-four-hour review mandate. The engineering team must understand that their role shifts from initiator to rapid responder.
Weeks two and three are the launch phase. Target easy wins to build momentum. Relocate a tool, adjust a workbench height, or clarify a visual instruction. When the shop floor sees a suggestion turn into a physical change within forty-eight hours, the volume of submissions will increase organically.
By the second month, the focus shifts to standardisation. Every implemented Point Kaizen must trigger a review of the control plan, a revision of the work instruction, and retraining for the shift. This ensures the micro-efficiency is permanently captured, preventing regression to the older, less efficient working methods.
Point Kaizen Implementation Cycle
- 01IdentificationOperator identifies friction or waste during standard work.
- 02SubmissionOperator completes a physical Kaizen card detailing the issue.
- 03Rapid ReviewEngineering reviews and approves or rejects within 24 hours.
- 04ImplementationPhysical change executed and validated on the floor.
- 05StandardisationSOPs updated and operators retrained on the new standard.