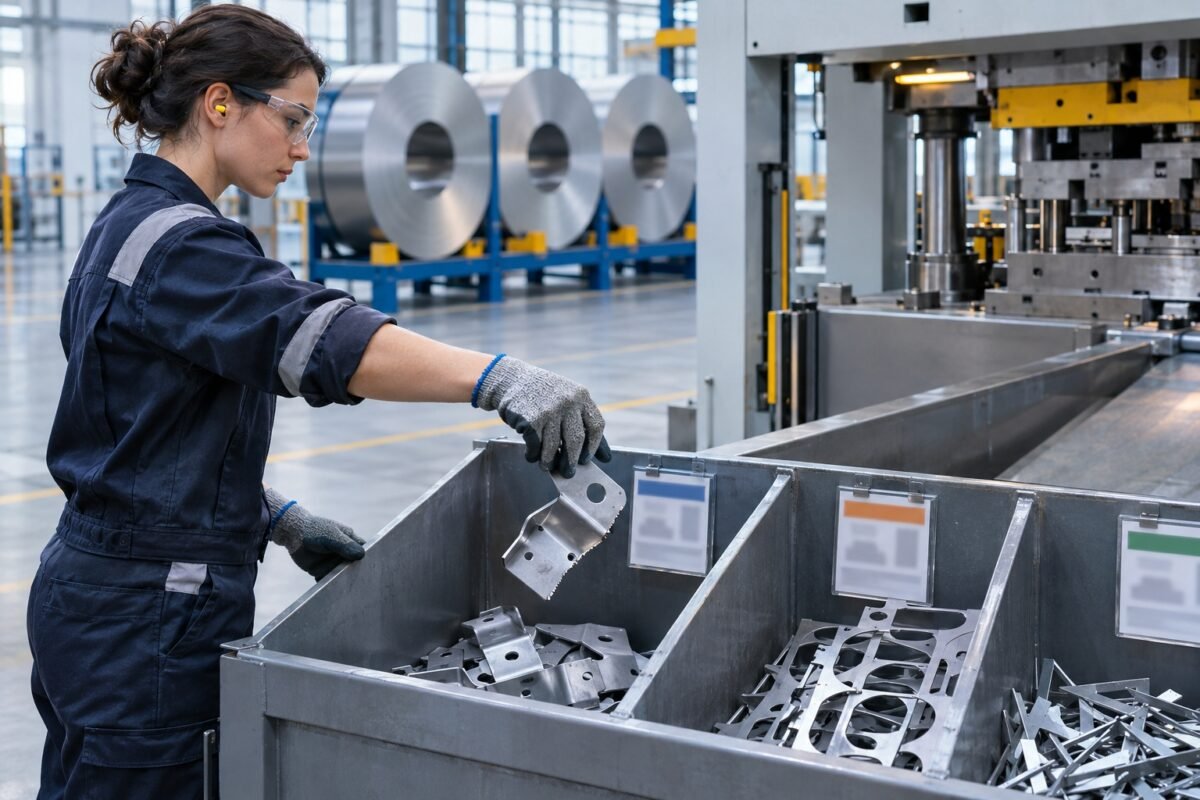
In every plant I have worked in, the environmental engineer and the quality engineer sat within thirty metres of each other and never compared figures. The environmental side tracked material yield because a regulator or a corporate sustainability report demanded it. The quality side tracked defect rates because a customer scorecard demanded it. Nobody noticed that both departments were largely measuring the same physical phenomenon from opposite ends.
A scrapped stamping is simultaneously a defect and a material loss. An offcut of extrusion too short to nest another part is both a yield loss and, often, a symptom of uncharacterised variation. When you split these into two ledgers, you lose the diagnostic information each one carries for the other. I have sat in scrap review meetings where the quality engineer agonised over root cause while the material utilisation report, held by someone else entirely, contained the answer in plain sight.
The argument of this article is simple: treat material efficiency as a quality metric, and defect rates as a material metric. Not as a management philosophy, but as a measurement discipline with specific numbers, specific failure modes and specific checks you can run next week.
What Yield Tells You About Process Control
Material yield data is often more honest than first-pass yield data, because material cannot lie about where it went. If a coil of steel enters a press line and you weigh the finished parts against the coil mass, the difference is accounted for by skeletons, offcuts, setup pieces and defective parts. Each category has a distinct process signature. Setup pieces cluster at the start of a run and tell you about die setting and first-off approval discipline. Skeleton loss tells you about blank development and nesting. Defective parts tell you about process capability and control.
When quality defects rise, material efficiency almost always falls with them, but not linearly. Consider a machining line where a bore drifts towards the upper tolerance limit. Parts go out of specification gradually, get quarantined, and the rework loop consumes additional clamp time, coolant, tools and — critically — often a second setup scrap event when the reworked batch is reintroduced. The material ledger captures this as rising consumption per saleable unit long before the monthly quality review captures it as a defect trend, because yield is measured per batch, not per inspection sample.
Run the test on your own operation. Pull twelve months of material issued per good part shipped, normalised for product mix, and overlay defect PPM on the same time axis. In my experience the two curves move together more often than either department expects. The divergences — where yield falls but defects hold steady — point you towards nesting problems, material handling damage, or supplier thickness variation that inspection never sees because it sits inside tolerance.
Offcuts as a Variation Mirror
Offcuts are the most neglected and most diagnostic loss category. An offcut is not waste in the innocent sense; it is material that failed to become product for geometric reasons. In sheet metal, bar stock, extrusion and textile cutting, offcut volume is a direct function of variation in incoming material dimensions and the aggressiveness of the nesting strategy. If your supplier's coil width varies by a few millimetres either side of nominal, your nesting software — or your nesting planner — will protect itself by using the worst-case width, and you will carry that margin as permanent offcut loss on every coil.
Here is the quality connection: the same width variation distorts blank positioning, shifts trim edges, and can push burr height or edge condition towards failure. I recall an aluminium extrusion line where the saw continually produced offcuts of a suspiciously consistent length. The operators had quietly increased the cut-back allowance because incoming stock had a chronic bow that receiving inspection, measuring only cross-section, never detected. That bow was also the root cause of a persistent flatness defect downstream. Two years of offcut data contained the evidence; nobody had looked.
What to measure: log offcut length, width and reason code at the point of creation, not retrospectively from stock movement transactions. Reason codes should distinguish plan-remainder (material left over by design), mix-remainder (wrong length for the next order), quality-cut (material suspected non-conforming and cut back) and nesting-loss. The proportions between these categories shift with process health, and a drift in the mix is an early warning worth more than most end-of-line inspection.
Scrap Classification: Where the Two Ledgers Meet
Scrap is the point where the two systems formally touch, and in most plants they touch badly. The quality system records scrap against defect codes: dimensional, surface, material, functional. The ERP records scrap against cost centres and material codes. The two rarely reconcile. Parts scrapped in quality terms are written off in the material ledger as aggregated "process loss", destroying the defect-specific information. Reconciliation meetings, where they exist, happen monthly at a level of aggregation that prevents engineering action.
Fix this by making the quality defect code a mandatory field on the material scrap transaction. It sounds trivial; in practice production fights it, because scrap happens at a pace that makes coding feel like bureaucracy. The answer is not exhortation but simplification: a code list short enough to fit on a laminated card at the machine, with an "other" code that you monitor and drive towards zero. "Other" is where diagnostic information goes to die.
Unifying the scrap transaction
- 01Scrap createdEvent logged at the machine, at the pace of production
- 02Defect code assignedShort list, laminated card, monitored "other"
- 03Material transaction writtenCode is a mandatory field, not an afterthought
- 04Joint Pareto in kilogramsLoss split by cause, mass-weighted, not part-counted
- 05Shared reviewQuality and environmental engineers act on one number
Once the codes are unified, build the single number: total material consumption divided by material in saleable product, split by cause. This gives you a Pareto in kilograms rather than parts, and that Pareto is a revelation to most organisations. A porosity defect in a casting may be a small number of parts but a huge mass of aluminium. A cosmetic defect on a small bracket may dominate your PPM count and barely register in tonnage. Knowing which losses carry the environmental and cost weight changes your improvement priorities.
A defect is not merely a customer risk and a cost; it is an emission event with the entire upstream chain attached.
Failure Modes of the Measurement Itself
Material efficiency metrics have their own failure modes, and I have watched good plants draw wrong conclusions from bad yield numbers. The commonest is yield measured at the wrong boundary. If you measure utilisation only within the press shop, you are blind to material consumed by defects created downstream — a cracked weldment discovered in assembly scraps back to material the press shop recorded as good output. Conversely, if you measure at the plant gate only, you cannot separate supplier-caused losses, such as off-spec incoming stock, from your own process losses. Define the boundary explicitly and keep it stable, or your trend lines are noise.
The second failure mode is the denominator problem. Material per part shipped changes with product mix, order size and batch frequency. Smaller batches mean more setups and proportionally more setup scrap; a plant moving towards smaller, more frequent deliveries will see apparent efficiency decline while doing exactly what its customers want. Normalise for it — material per part per setup event, or yield indexed against a mix-adjusted baseline — or you will punish the very flexibility you need.
Third, watch the rework loop. Reworked material can be counted twice as consumed if the transaction system issues material again at rework entry. I have audited yield calculations where rework routing errors inflated apparent consumption by more than the entire defect scrap stream. Before you trust the number, trace ten reworked parts end to end through the transactions and see what the system believes happened to them.
Two ledgers, one quantity
Separated systems
- Scrap written off as aggregated process loss
- Offcuts logged retrospectively from stock moves
- PPM Pareto driven by part count
- Monthly reconciliation, too aggregated to act on
Unified measurement
- Defect code mandatory on scrap transaction
- Offcut reason codes captured at the point of creation
- Pareto in kilograms alongside PPM
- Weekly joint review of one shared number
What to Put on the One Page
If I had one page for the plant manager each week, it would carry five items: material utilisation percentage (good material out over material in, boundary-defined), scrap mass by defect code in a Pareto, offcut mass by reason code, setup scrap mass per setup event, and the ratio of defect mass to total defect count. That last ratio is the quiet masterpiece — it tells you whether your defect profile is dominated by mass-heavy or count-heavy failures, which determines whether improvement effort should go towards process control or towards inspection and containment.
Alongside the numbers, run the physical checks. Weigh a sample of skeletons and offcuts against the transaction records monthly; scale errors and estimation creep in. Audit the quarantine area quarterly and reconcile the physical scrap bins against the defect codes claimed. You will find parts coded conveniently, parts recycled without coding, and the occasional bin of premium alloy sold as mixed scrap because nobody separated it — an environmental and a financial sin at once.
Then put the environmental and quality people in the same meeting with this page. That is the whole organisational change required: not a new department, not a steering committee — a shared metric, a shared Pareto in kilograms, and a shared responsibility for a number neither of them owns alone. In my experience the first such meeting produces more corrective action ideas than the previous six months of separate reviews, because the two halves of the evidence finally sit next to each other.
The Environmental Argument, Made Concrete
Every kilogram of scrap carries the embodied energy and emissions of the entire upstream chain: smelting, rolling, casting, transport, heat treatment. When you scrap a machined forging, you discard not the forging alone but the billet, the furnace time and the machining energy already invested. Rework doubles portions of that chain. Offcuts recycled in-house recover material value but not the forming energy, and remelting carries its own burden.
For the quality practitioner, this reframes the stake. It matters increasingly in automotive and aerospace supply chains, where customers now ask for carbon footprints per part and where scrap rate feeds directly into declared figures. A plant with a rigorous, code-level material efficiency metric can answer those questions from real data. A plant with an aggregated "process loss" line item cannot, and will eventually be asked to.
The overlap between material efficiency and defect rates is not a metaphor. It is a single physical quantity — material that failed to become product — recorded by two departments under two names. Quantify it once, jointly, in kilograms, and both the quality system and the environmental account become sharper instruments than either was alone.