Overall Equipment Effectiveness is widely treated as a maintenance metric, something the reliability team tracks to justify its budget. That framing limits its value. OEE measures how well a process converts equipment time, material and energy into conforming product, which puts it squarely in the domain of quality engineering.
The formula is simple: Availability multiplied by Performance multiplied by Quality. The implications are not. A press that runs at full speed but produces 12 percent scrap is not effective. A grinder that stays clean but changes over every forty minutes is not effective. OEE forces the organisation to confront the combined loss, not just the component that suits the current narrative.
Over twenty years implementing quality systems at a major aerospace manufacturer, SNOP, WITTE Automotive and elsewhere, I have watched plants chase individual factors and miss the system. A line supervisor hits his availability target by skipping preventive maintenance. Scrap rises. OEE drops. The lesson is that the three factors are interdependent, and improving one at the expense of another is regression dressed up as progress.
The three factors and where they fail
Availability is the ratio of planned running time to actual running time. Every unplanned stoppage, every changeover, every micro-stop erodes it. The standard TPM response is autonomous maintenance, SMED for changeovers, and disciplined shift handovers. The failure mode I see most often is generous planning: the schedule absorbs so much buffer that a 70 percent availability figure looks acceptable because the line still ships on time.
Performance measures actual cycle time against the nameplate or engineered standard. A machine running below rated speed is losing capacity, even if it never stops. The hidden enemy here is chronic slowdown: operators deliberately run at 80 percent to avoid jams, and within a quarter that becomes the unofficial standard. SPC and cycle-time analysis expose the gap, but only if the engineered standard is correct and enforced.
Quality is the first-pass yield ratio: good parts divided by total parts produced. This is the factor quality engineers own, yet it is the one most often miscalculated. Plants count reworked parts as good. They exclude start-up scrap. They measure yield at final inspection rather than at the source. An honest Quality factor requires counting every part that does not meet specification on first pass, including the ones you successfully rework.
World-class OEE and its component targets
Building OEE into a greenfield plant
At WITTE Automotive I built a greenfield QA and QC department for a plant with over 900 employees. OEE was embedded from day one, not bolted on after commissioning. Every line had an OEE standard defined before the first part ran. TPM was structured into the maintenance plan, SPC governed the performance factor, and quality controls measured first-pass yield at the source, not at final audit.
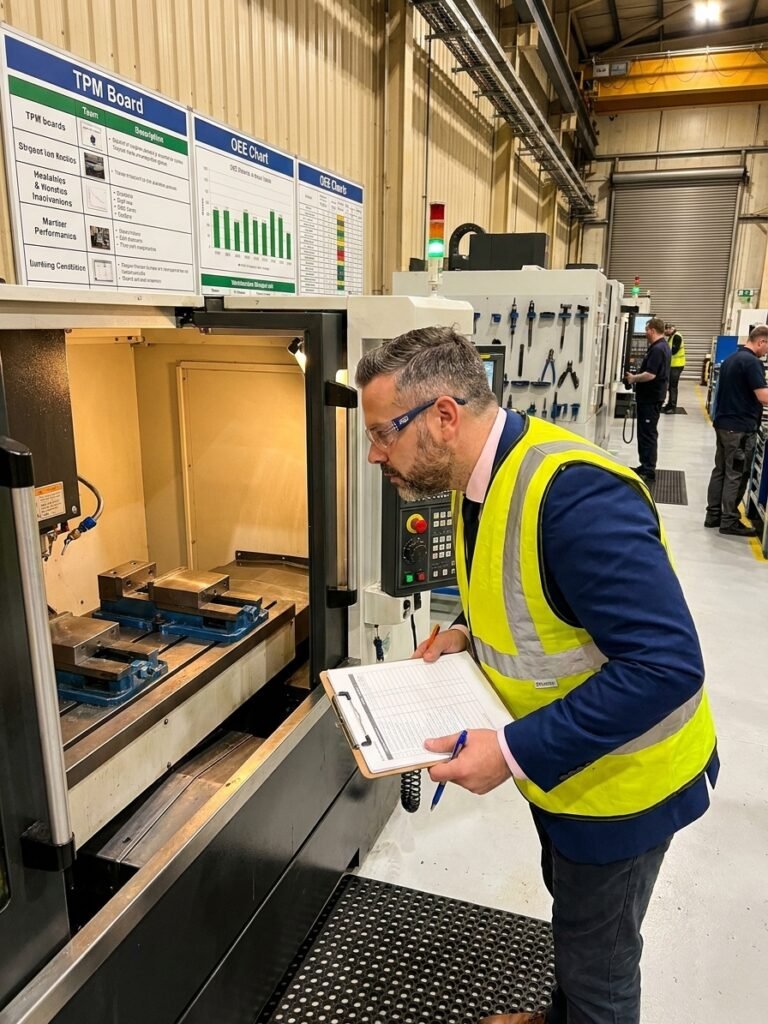
Visual management was the critical mechanism. OEE dashboards sat on the shop floor, updated each shift, visible to every operator and team leader. Daily review meetings were short, fact-driven and tied to action logs. The discipline was not in the software but in the conversation: the number triggered a root-cause discussion every single day, and unresolved losses escalated to engineering within 48 hours.
The systemic result was that availability losses were attacked through TPM and SMED, performance losses through cycle-time optimisation and tooling revision, and quality losses through PFMEA-driven process changes. Because all three factors were measured and reviewed together, the plant avoided the trap of trading scrap for speed or uptime for yield. OEE functioned as the integrating metric it was designed to be.
OEE in high-precision environments
Cleanroom and high-precision manufacturing adds a constraint: process capability is measured not only in dimensional terms but in contamination and defect rates. In these environments the Quality factor carries disproportionate weight. A machine running at 95 percent availability and 98 percent performance is irrelevant if particle counts drift and force batch rejection. The OEE calculation must reflect that reality.
This means adapting the measurement. In precision electronics, a yield figure that ignores micro-contamination is a fiction. The quality leg of OEE has to capture in-process and end-of-line defect data, including defects that pass dimensional checks but fail functional or cleanliness tests. Where I have seen this done well, the SPC system feeds the quality factor directly, so the OEE number reflects real conformance, not an optimistic proxy.
The maintenance strategy shifts in tandem. TPM in a cleanroom is not just about preventing breakdowns; it is about preventing the slow degradation that introduces variation. Filter replacement schedules, wipe-down procedures and gowning discipline all feed availability and quality simultaneously. The lesson is that OEE implementation must reflect the physics of the process, not a generic template copied from an automotive press shop.
The measurement discipline that makes OEE honest
The hardest part of OEE is not the arithmetic. It is the data integrity. Manual OEE logging, where operators record stoppage reasons at the end of a shift from memory, routinely overstates performance by 15 to 20 percentage points. People remember the big breakdown and forget the twenty micro-stops. They round cycle times favourably. They classify ambiguous stops as planned. The result is a number that feels good and drives no improvement.
Automated data capture solves part of this, but it introduces its own failure mode: loss categorisation. If the system logs every stop as unspecified downtime, the data volume is high but the actionability is zero. The discipline lies in defining a loss structure that maps to your real failure modes, training operators to use it correctly, and auditing the categorisation weekly. Without that, you have a chart, not a tool.
A plant that reports 90 percent OEE but shows no improvement plan is either lying or not trying.
The practical test is whether the OEE number drives an 8D or a CAPA. If the daily review produces a discussion but no action items, the metric is decorative. I have audited plants where the OEE dashboard was the most polished object on the shop floor and the corrective action log was empty. The dashboard existed to impress visitors. The real signal of a mature OEE system is a congested action log, not a clean one.
Connecting OEE to the management system
OEE belongs inside the ISO 9001 or IATF 16949 management system, not alongside it as a parallel tracking exercise. The quality factor maps directly to clause 8.5.1 control of production and the requirement for process monitoring. Availability and performance map to resource management and infrastructure. When OEE is integrated into the management system review, it becomes an input to decisions about investment, training and process redesign.
The alternative is the shadow system: a spreadsheet that production maintains, quality ignores, and maintenance disputes. Each function measures its own piece and defends its own number. Availability is high because maintenance reclassifies breakdowns. Performance is high because production uses a soft standard. Quality is high because the quality team excludes rework. The integrated OEE forces a single, reconciled truth.
Isolated tracking versus integrated OEE
What teams typically do
- Each department tracks its own KPI in isolation and reports independently.
- Availability is measured against a generous, buffered plan that hides losses.
- Cycle-time standards are informally adjusted downward to make output look good.
- Reworked parts are counted as good yield, inflating the quality figure.
What actually works
- One cross-functional OEE figure is owned jointly by production, quality and engineering.
- Availability is measured against engineered, validated running-time standards.
- Performance is benchmarked against original equipment nameplate or validated standards.
- Quality is strictly first-pass yield; every reworked or scrapped part is a loss.
Sustaining the gain after the project ends
OEE improvement projects produce strong early results and then plateau. The first three months of rigorous measurement typically expose so much low-hanging waste that the number climbs fast. Then the easy problems are solved, the cross-functional meetings become routine, and attention drifts. The OEE figure stagnates at 60 or 65 percent and the organisation accepts it as the new normal. This is where most implementations fail.
Sustaining the gain requires escalating the rigour. The loss-cause structure becomes more granular. The action-log review moves from weekly to a tiered daily-and-weekly cadence. The engineering team takes ownership of the chronic losses that operators cannot solve on the floor. The MSA on the data-collection system itself is audited, because measurement error in cycle-time or stoppage logging corrupts the entire OEE calculation.
At its best, OEE is not a metric you report. It is a discipline you practice. It tells you where the process is bleeding, whether the bleeding is in uptime, speed or conformance, and whether your corrective actions are actually working. The plants that get this right treat OEE the way they treat Cpk: as a number that must be earned every shift, defended through process control, and never taken for granted.