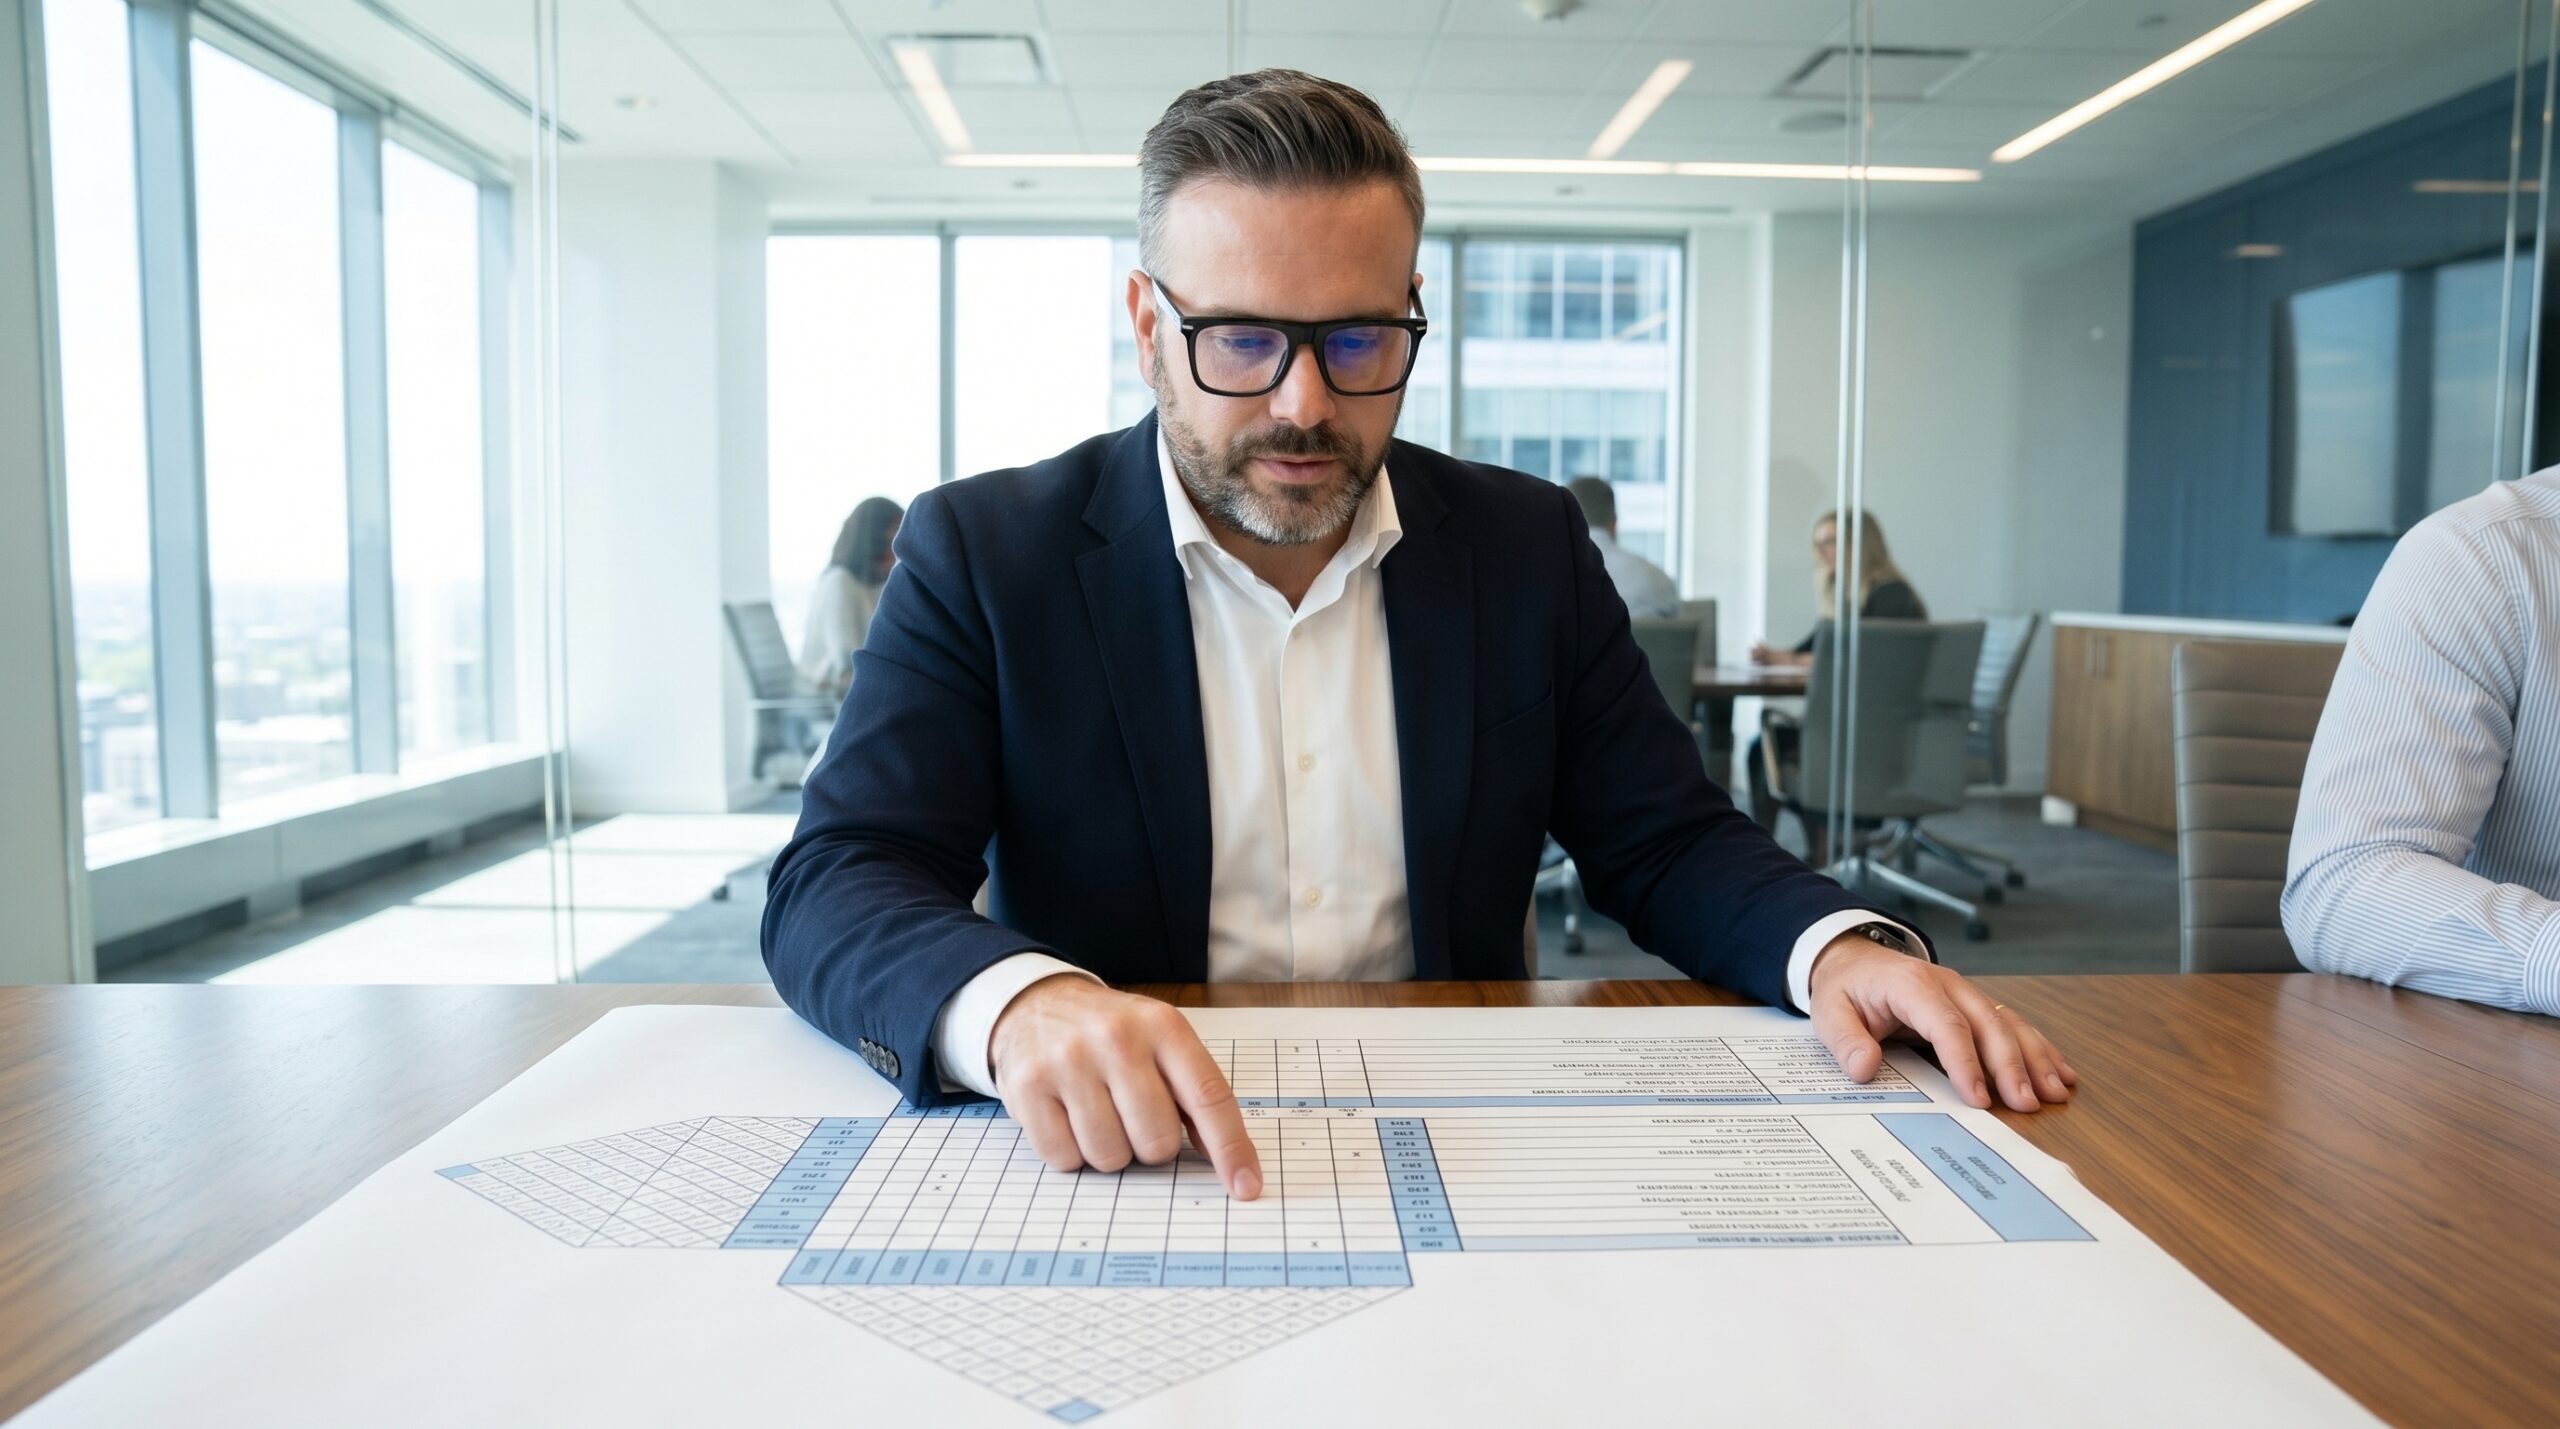
I was sitting in a conference room at a Tier 1 automotive supplier when the marketing director asked a question I have heard dozens of times: we know what the customer wants, but our engineers cannot translate those wishes into technical parameters.
On the table sat a prototype for a new plastic trim cover. The OEM demanded a robust feel, a quiet closure, and an elegant appearance. The design team delivered a standard specification: wall thickness 2.5 mm, standard PP-T20 material, and a generic sealing profile.
Nobody had verified whether 2.5 mm actually produces a robust feel. Nobody tested whether that specific material dampens sound effectively during closure. The team simply copied the previous project's solution and hoped it would satisfy the new OEM. That is the exact moment I told them they needed Quality Function Deployment.
The High Cost of Guessing in Product Development
Without a structured translation method, customer requirements are interpreted rather than measured. A robust feel means a 3 mm thickness to one engineer, while another assumes 2 mm with reinforced corners. Technical parameters are configured based on legacy projects rather than current customer demands.
This guessing approach means conflicts between requirements remain hidden until prototyping. The customer simultaneously demands low weight and high robustness. Without a correlation matrix, the design team has no mechanism to identify where the mechanical trade-offs lie.
In the automotive sector, where a single injection moulding tool can cost over 50,000 EUR and APQP cycles run for 18 months, guessing is a liability. Iterations consume budget, delay launch dates, and exhaust engineering resources. Quality Function Deployment (QFD) eliminates this ambiguity by deploying quality controls into every step of product development.
Developed in Japan in the 1960s by Yoji Akao, QFD became an automotive standard through Toyota and Mitsubishi. The core tool is the House of Quality (HoQ), a matrix that maps subjective customer needs directly to measurable engineering parameters and manufacturing tolerances.
Anatomy of the House of Quality Matrix
The left side of the matrix captures the WHATs: specific customer requirements. This is not a list of technical parameters, but exactly what the customer feels and experiences. We assign an importance weighting (typically 1 to 9) to each requirement to ensure the team prioritises what is actually critical to the OEM.
The top row defines the HOWs: the measurable engineering characteristics that influence those needs. Parameters must be strictly quantifiable. A robust material is not a parameter; a PP-T20 compound with a flexural modulus of 2800 MPa is a parameter. Vague targets guarantee vague results downstream.
At the intersection of WHATs and HOWs sits the relationship matrix. The team assigns a numerical value to each interaction: a strong relationship scores 9, a medium relationship scores 3, and a weak relationship scores 1. This calculates which technical characteristics drive customer satisfaction.
The final output is a prioritised list of target values. High-scoring engineering parameters dictate the focus of the PFMEA, Control Plan, and MSA. Low-scoring parameters can remain at standard specification levels, saving valuable engineering hours on variables that do not impact the end user.
Legacy Design vs QFD-Driven Design
Standard Approach
- Parameters set by copying previous project files
- Subjective OEM demands left open to interpretation
- Technical conflicts discovered during physical prototyping
- Costly tool modifications and delayed PPAP submissions
QFD Approach
- Parameters driven by weighted customer needs matrix
- Subjective demands quantified into exact mechanical targets
- Technical trade-offs resolved mathematically before tooling
- First-time-right prototypes and seamless APQP delivery
Mapping Correlations to Resolve Engineering Conflicts
The roof of the House of Quality matrix exposes the relationships between the engineering parameters themselves. These correlations can be positive, where increasing one parameter benefits another, or negative, where improving one variable damages a separate requirement.
Increasing wall thickness improves vibration resistance, creating a positive correlation. However, increasing wall thickness directly conflicts with the low weight requirement, creating a negative correlation. Increasing the number of locking mechanisms improves the quiet closure but complicates manual assembly on the production line.
Teams routinely skip the roof of the matrix because it demands difficult conversations between design and manufacturing engineers. This is a critical mistake. The roof is where the most expensive engineering conflicts live. If you do not resolve these trade-offs on paper, they will materialise as steel rework in the tool shop.
If you do not resolve technical trade-offs on paper in the matrix, they will materialise as steel rework in the tool shop.
Executing a QFD Workshop in Three Days
At that Tier 1 supplier, I proposed a three-day workshop bringing together marketing, design, quality, and manufacturing. Day one focused entirely on gathering and structuring the Voice of Customer. We mapped the OEM requirements systematically and uncovered massive data loss between the commercial team and the engineering desk.
The OEM had defined a quiet closure as generating a maximum noise level of 35 dB. This exact metric had never reached the design engineer. Instead of designing to a decibel target, the engineer had simply guessed at a material density. This single insight justified the entire QFD exercise.
On day two, the engineering team defined twelve technical parameters and populated the relationship matrix. We immediately uncovered three critical negative correlations in the roof of the matrix: wall thickness versus weight, the number of locks versus assembly ease, and material hardness versus sound dampening.
Day three was dedicated to resolving those conflicts with innovative solutions. We specified variable wall thickness with 3 mm reinforced zones in critical stress areas and 1.8 mm walls in non-loaded areas, dropping weight by 15 percent while maintaining robustness. We redesigned the locking system into a snap-fit geometry with guiding ribs, reducing the part count while improving assembly ergonomics.
The Three-Day QFD Workshop Structure
- 01Day 1: Voice of CustomerMarketing and sales define and weight the exact WHATs, clarifying lost data like specific decibel limits.
- 02Day 2: Technical TranslationEngineering establishes the HOWs and maps the relationship matrix to identify hidden negative correlations.
- 03Day 3: Conflict ResolutionCross-functional teams design alternatives for technical trade-offs and finalise target values for the Control Plan.
Integrating QFD With Core Quality Tools
QFD does not operate in isolation. It serves as the critical input for your entire Advanced Product Quality Planning (APQP) system. The prioritised technical parameters flow directly into Product Design and Development, forming the foundation for subsequent core tools.
High-scoring characteristics from the HoQ matrix dictate the focus of the DFMEA. The design team finally has data proving which parameters cannot fail. These critical parameters then migrate into the Control Plan as key characteristics, requiring specific measurement system analysis (MSA) to verify gauge capability before PPAP submission.
During a PPAP audit, a well-executed QFD matrix serves as documented evidence of design rationale. It demonstrates exactly why specific tolerance values were chosen and proves the design is driven by customer data rather than engineering guesswork. It functions as the structural bridge between commercial intent and manufacturing execution.
I have seen teams fail by building matrices with fifty requirements and forty parameters, resulting in thousands of unmanageable cells. The standard rule is to restrict the scope to a maximum of twenty WHATs and twenty HOWs. If the product is highly complex, break it into three sub-system matrices instead of building one massive, unreadable document.
Another frequent failure occurs when engineers populate the relationship matrix purely from memory. If you do not know whether a parameter has a strong or medium impact, go measure it. Run a physical test, execute a simulation, or push the commercial team to clarify the requirement with the OEM. A QFD matrix built on assumptions provides no actual risk mitigation.
Measuring the ROI of Deployment
The success of QFD is measurable through concrete launch metrics. Track the number of physical prototypes required before OEM approval. A properly executed matrix should reduce iterations to two or fewer before final sign-off. Concept-to-approval lead times should drop significantly, driven by the elimination of late-stage design disputes.
Costs associated with engineering change orders in the late phases of APQP should plummet. When teams resolve mechanical trade-offs during the initial three-day workshop, they avoid the massive expense of modifying hardened tooling. The focus shifts from reactive problem-solving to proactive design optimisation.
Post-launch customer complaints should align strictly with the benchmarked targets established in the right side of the HoQ matrix. The subjective requirements mapped on day one must translate directly into the final user experience. When executed correctly, QFD fundamentally alters organisational behaviour, replacing internal opinions with structural data.
That initial plastic cover prototype passed all OEM testing requirements without a single engineering reservation. The OEM subsequently adopted it as the benchmark component for future programmes. The supplier's internal team went on to apply the QFD methodology to seven subsequent platform launches, achieving consistent quality and predictable APQP timelines.