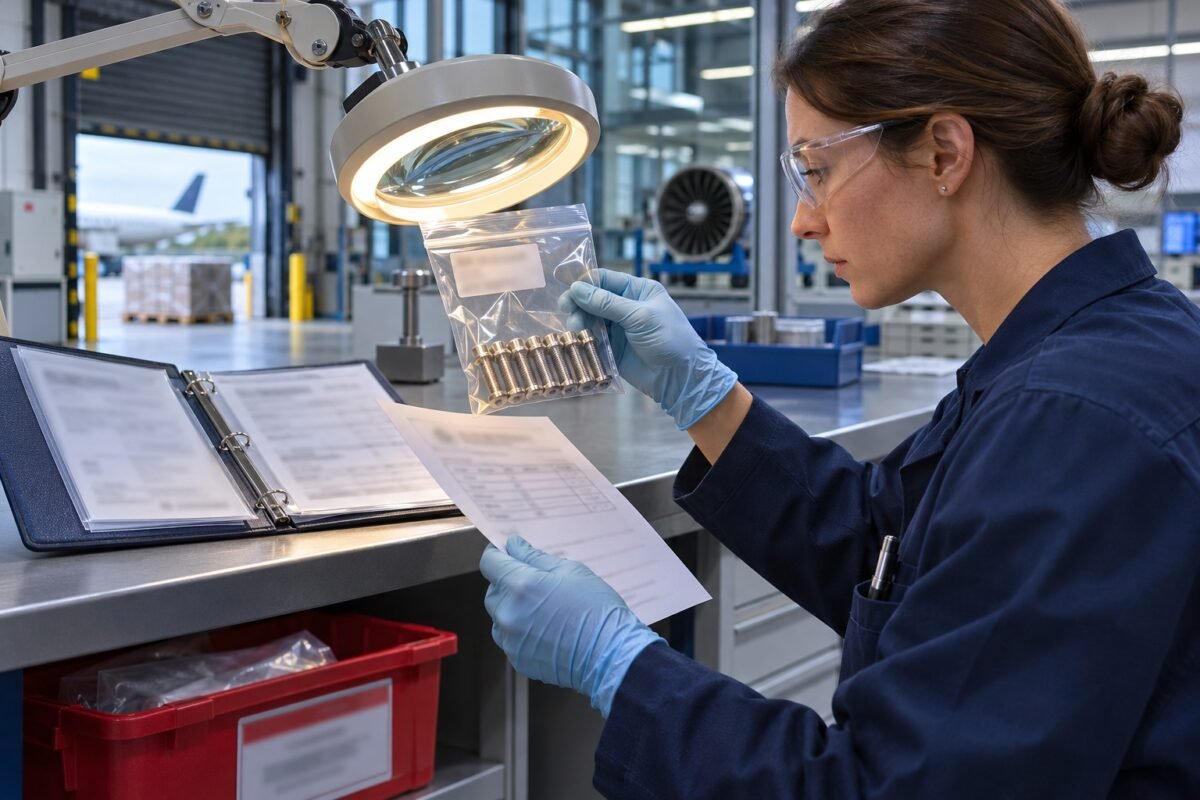
The Part That Is Too Clean
In my experience, the counterfeit or unapproved part rarely announces
itself through poor workmanship. On the contrary, it is often the
best-looking item in the delivery: correct finish, correct packaging,
correct markings, and a documentation folder that reads like a textbook.
That perfection is precisely what should raise suspicion. Genuine
aerospace hardware accumulates honest irregularities — a reissued
certificate because a typographical error was corrected, a batch split,
a slightly out-of-order date code on plating paperwork.
The suspect part tends to have a linear, unbroken chain: raw material
certificate, forging report, heat treatment chart, NDT release, final
inspection, all dated in tidy sequence with no amendments. Real
manufacturing history is messy. When I review a first-article dossier
that contains no deviations, no concession notes and no rework records
across a multi-year production run, I start asking questions rather than
congratulating the supplier. Statistical reality says friction exists; a
frictionless history is a constructed one.
Where
Traceability Breaks: The Gaps That Matter
Traceability failures cluster in predictable places, and knowing them
focuses your audit effort. The first is the transfer point between
process owners — forging to machining, machining to surface treatment,
treatment to assembly. Each handover is an opportunity for a lot number
to be transcribed incorrectly or, more dangerously, for a certificate to
be regenerated under a new reference that no longer links back to the
melt or heat. Check whether the heat treat furnace chart carries the
same lot identity as the incoming forging certificate, not merely a
plausible date.
The second gap is the distributor tier. Authorised distribution
agreements get quietly terminated, stock gets sold on, and the paperwork
follows the part rather than the approval status. I always trace the
purchase order path backwards: who held the design approval or PMA at
the time of manufacture, and did that approval actually cover the
specific part number and configuration sold? A certificate can be
entirely authentic and still describe a part that was never approved for
the application it ended up in. Revision level mismatches — an old
configuration sold against a new drawing — are the classic instance.
Forgery Signatures in the
Paperwork
Forged documentation has recognisable signatures once you have stared
at enough of it. Watch for certificates produced on the standard
holder’s template but with the signature block pixelated, rotated a
fraction of a degree, or in a font that differs subtly from the rest of
the document. Cross-check the signatory’s name against the accredited
laboratory’s scope and personnel records where possible; accreditation
bodies publish these. A tensile test report signed by someone who
appears nowhere in the lab’s records is a finding in itself.
Content errors are often more telling than formatting ones.
Conversion errors between units, hardness values reported for a material
specification that calls only for tensile, chemical compositions that
match the previous certificate on file exactly down to the third decimal
place — genuine spectrometer results show scatter. Compare the
certificate’s test values against the specification limits: forged
documents frequently sit comfortably near the centre of the band because
the forger copied an example rather than generating real data. Pull the
raw trace: a legitimate lab can usually produce the instrument output
behind any certificate it issued, and hesitation to do so is
diagnostic.
Physical
Inspection: Interrogating the Hardware
Examination of the part itself must go beyond visual comparison.
Dimensional verification against the drawing, including thread forms,
radii and surface texture callouts, catches reworked or substituted
configurations. Material identification by X-ray fluorescence or, where
the alloy demands it, optical emission spectrometry, will expose a
300-series stainless bolt masquerading as A286 or an aluminium fitting
sold as titanium. Hardness testing on a non-critical surface provides a
fast screen against the certificate’s claimed heat treatment
condition.
Markings deserve forensic attention. Genuine part numbers and serials
are typically applied by dot-peen, laser or electro-etch with consistent
depth, spacing and font geometry for a given manufacturer. Look under
magnification for evidence that a marking was ground off and re-struck,
adhesive residue from overlay labels, or serial number fonts whose
kerning varies character by character — a hallmark of hand-engraved
re-marking. Weigh the part: counterfeits in substitute alloys frequently
miss the nominal mass by a margin noticeable on a calibrated balance.
Where the application is critical, metallographic sectioning of a
sacrificial sample can reveal grain flow inconsistent with a forged
original, indicating a machined-from-bar substitute.
Reporting
Duties: What the Regulations Demand of You
This is where I see otherwise diligent organisations stumble. A
suspect unapproved part is not just an internal quality problem; it
carries mandatory external reporting obligations. Under EASA Part-21 and
the associated provisions, and under FAA rules, an organisation that
identifies a part suspected of being unapproved must report it to the
competent authority — promptly, in writing, with the part quarantined
and its source identified. Suspected aeronautical parts arriving from
civilian channels additionally carry a duty to notify law enforcement,
because distribution of such parts can be a criminal matter.
The sequence matters in practice. Quarantine the part physically and
in your records, preserve all accompanying documentation and packaging
as evidence, and do not return it to the seller — returning it destroys
the evidential chain and lets the counterfeit circulate onward. Notify
your airworthiness authority through the established channel, file
against your regulatory reporting requirements, and cooperate with the
design approval holder, who can often perform definitive authenticity
checks against their build records. Waiting to see whether the supplier
“sorts it out” before reporting is a compliance failure I have watched
organisations pay for twice: first in regulatory enforcement, and later
when the same part resurfaced elsewhere in the fleet.
Building
Detection into Receiving, Not Just Audits
Annual supplier audits alone will not catch this; the detection point
must be the receiving dock. Define a risk-ranked incoming inspection
regime: parts sourced outside the approval holder’s direct distribution
network, flight-safety-critical hardware, and items purchased from
stockists get enhanced verification. That means certificate content
review against the specification, checking that the cited approval
reference is current and covers the part, and physical verification
proportionate to criticality. Segregate and flag anything where the
paperwork cannot be reconciled before it touches stores.
Train receiving inspectors on the specific tells discussed above —
font inconsistencies, centred test values, missing raw data, mismatched
lot identities between documents. Give them a standing instruction that
suspicion is a legitimate basis for rejection, and a quarantine route
that carries no penalty for false alarms. I would rather review ten
rejected batches that turn out genuine than wave through the eleventh
that is not. Keep a register of suspicious documentation encountered,
because patterns emerge: the same template errors, the same signatory
names, recurring across ostensibly unrelated suppliers.
What I Tell My Teams
The unapproved part survives because everyone assumes someone else
checked. The buyer assumes the distributor verified approval status; the
distributor assumes the certificate proves it; receiving inspection
assumes the purchase order guarantees pedigree. In a suspect-parts
investigation I led some years ago, the counterfeit entered precisely
through that chain of assumptions — the paperwork was flawless, and
nobody had ever asked whether the cited approval reference actually
existed in the authority’s database.
Verification is cheap; assumptions are not. Check the approval
reference against the regulator’s published listings. Telephone the
issuing laboratory on a number you source independently, not one printed
on the certificate. Compare test data across batches for suspicious
uniformity. And when something feels wrong, report it properly and
quickly — the duty exists because the next recipient of that part may be
an aircraft with people on board. A perfect history deserves scrutiny
precisely because it is perfect. Real parts, like real processes, carry
the marks of their making.
Peter Stasko is a Quality Director with 25+ years of experience
leading quality management systems across the automotive and aerospace
industries.