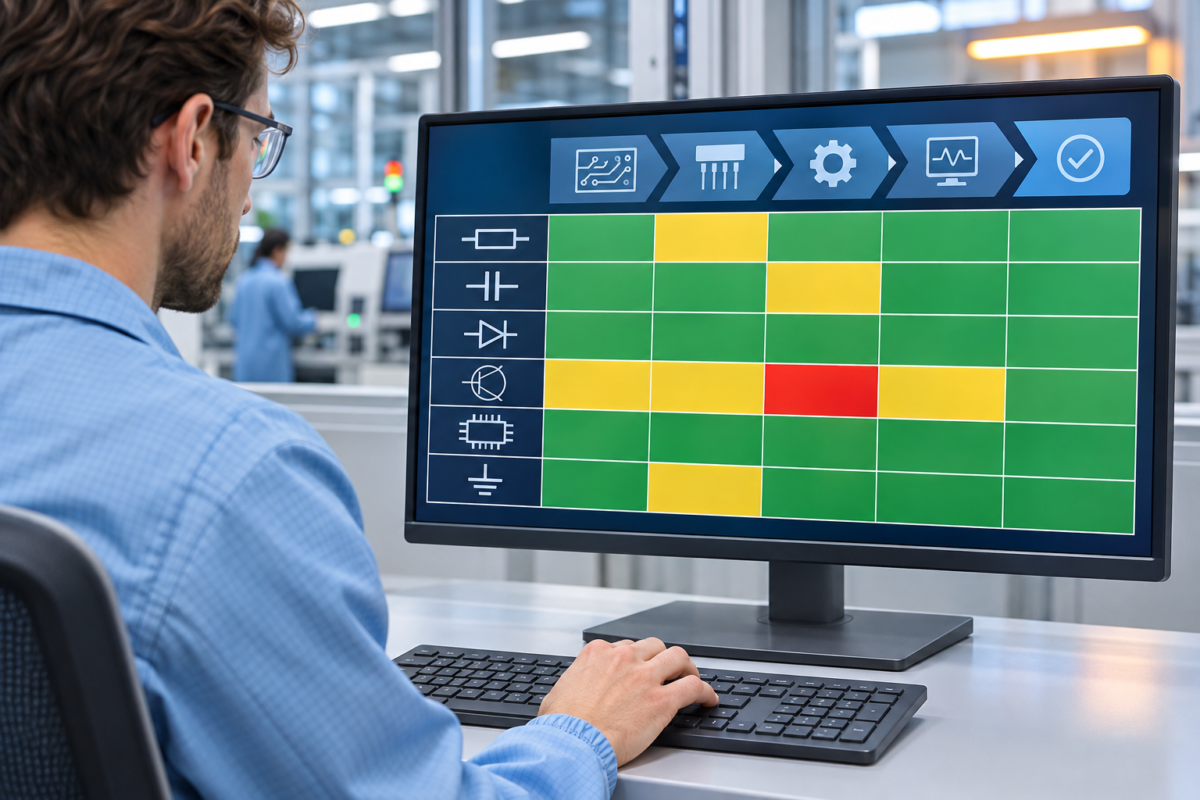
Every electronics manufacturer I have worked with can tell me what their tester checks. Very few can tell me what it does not check, and that gap is where field failures come from. A functional test that passes a board has not proven the board good; it has proven the board good at the specific things that test sequence exercises. Solder joints on unused pins, dormant logic paths, marginal timing windows and untested protection circuitry all sit outside the net.
The uncomfortable truth is that fault coverage is a property of the test, not the product. Two identical boards sent through two different test strategies will carry entirely different escape risks. When a customer returns a unit with an intermittent open on a bypass capacitor that functional test never stimulated, the failure was not a surprise — it was simply invisible to the architecture you built.
My working definition for a mature programme: you can produce, on demand, a documented statement of which fault types you detect, which you infer, and which you knowingly accept as escapes. That statement is a living document, revised with every test programme release and every field failure analysis. If you cannot produce it, you do not have a test strategy; you have a test habit.
Fault Coverage Analysis: Counting What Matters
Proper coverage analysis starts with a fault model. For board-level work, the staple is the stuck-at model borrowed from chip test — a node permanently at logic high or low — supplemented with open and short models for interconnects, and increasingly with bridging faults modelled from adjacent nets on the layout. For process defects on assembled boards, opens and shorts dominate: a BGA ball not wetted, a tombstoned 0201, a solder bridge between fine-pitch leads.
Fault simulation is the mechanism that converts these models into a number. You simulate each candidate fault, apply your test vectors, and record whether the fault propagates to an observable output. The faults that never propagate are your undetected set. On digital logic this is tractable with boundary scan infrastructure and ATPG tools. On analogue and mixed-signal circuitry it is far harder — fault simulation of an op-amp stage requires modelling parametric drift, not just opens and shorts, and many teams fall back on heuristic coverage estimates. Say so explicitly in your documentation rather than dressing a guess as a measurement.
Coverage claims deserve healthy scepticism. A figure quoted without the fault universe it was calculated against is meaningless. Coverage of stuck-at faults within boundary-scan-supported logic is not coverage of the board. Segment your reporting: interconnect coverage, component-level coverage by package type, functional coverage of software-visible behaviour. A granular, honest breakdown beats a single flattering aggregate every time, and it tells the failure analysis engineer precisely where to look when escapes occur.
Escape Modelling: Reasoning About the Leaks
Escape modelling asks a narrower question than coverage: of the defects that actually occur in my process, what fraction will pass through my test wall? This is driven by the defect spectrum, which varies by process. A line running 0.4 mm pitch QFPs generates bridging faults; a line running bottom-terminated components generates head-in-pillow and solder starvation under the body — invisible to any electrical test that does not stress the joint mechanically or thermally.
The practical method is defect-mode mapping against test detection capability. Build a table: rows are realistic defect modes per component family and process step; columns are your test stages — ICT, boundary scan, functional, system test, burn-in. For each intersection, state detection confidence honestly: detected, partially detected, conditional on vector content, or not detected. The not-detected column is your escape model.
Every field return should be checked against this table. Either the model predicted the escape, in which case you accepted a known risk, or it did not, in which case the model is wrong and needs revision. That discipline is what separates a model from a wall chart. Without the feedback loop, the table degrades into an opinion about defects rather than a measurement of them.
Latent and intermittent defects deserve their own treatment. A cracked joint under a large inductor may conduct at room temperature and fail under vibration or thermal cycling. If your test wall is entirely at room ambient with no stimulus, no amount of electrical coverage addresses it. Escape modelling should therefore include environmental detection stages, and where they are absent, the model must record those defect families as accepted risk rather than pretending electrical test covers them.
Boundary Scan: Honest Assessment of Its Reach
Boundary scan, built on the IEEE 1149.1 architecture, remains the most under-exploited coverage tool I see. Its core value is interconnect test: shorts and opens on nets connecting boundary-scan-enabled devices, tested through the test access port without physical nodal access. As fine-pitch BGAs and stacked packages have eroded bed-of-nails access, boundary scan has gone from convenient to essential on dense digital boards.
Its limits must be stated plainly. Boundary scan tests the boundary registers and the interconnect between them — not the internal logic of non-scan devices, not analogue signal chains, not the functional integrity of the silicon behind the pins. A net driven by a non-scan component and received by a scan component can be tested in one direction only, and nets between two non-scan devices are dark entirely. Coverage figures that include chain integrity as tested interconnect flatter the reality; chain test proves the TAP path works, nothing more.
Extended uses are where the real leverage sits. BSDL-driven interconnect tests combined with silent running for cluster testing of memory interfaces, programming of flash devices in-circuit, and PLD-based bitstream verification all add coverage at essentially zero fixture cost. Getting there requires discipline at design time: JTAG access maintained on every scan device, no gated or multiplexed TAP lines without documented workarounds, and schematic annotations that the test engineer can trace. When design reviews treat test access as a requirement rather than a request, boundary scan pays for itself in reduced fixture complexity.
Test Economics: Where the Money Actually Sits
Test economics is not about minimising test cost per board; it is about optimising the total of test cost plus escape cost. An additional screen that costs seconds of cycle time and modest fixture investment is trivially justified if it removes a defect family whose escape cost — warranty analysis, containment, customer sorting, reputation — is two or three orders of magnitude higher. The hard part is that escape cost is diffuse and lands in someone else's budget, whilst test cost lands visibly in manufacturing.
The framework I use positions test stages by defect detection capability and cost of application. Structural tests such as ICT and boundary scan catch defects early, when repair is cheap and diagnosis is precise. Functional test catches integration and performance issues later, where diagnosis is slower and rework is more expensive. Burn-in and environmental stress screening catch latent defects that nothing else sees, at the highest cost per detection. Removing a stage to save cost shifts its defect population downstream, where the same defect costs more — the economics are unfavourable by construction.
Investment logic follows the escape model. Concentrate spend where the model shows large undetected defect families with credible escape consequences. Sometimes that means adding vectors to an existing functional test — nearly free. Sometimes it means AOI or X-ray inspection for joints electrical test cannot discriminate: a solder bridge detected by ICT costs a rework touch-up; detected by the customer it costs an eight-week investigation. Run the numbers per defect family, not per test stage, and the investment priorities usually become obvious.
A passing functional test has not proven the board good; it has proven it good at the specific things that sequence exercises.
What to Measure and Audit on the Line
Coverage is not a one-time calculation. Measure escape rate against modelled expectation, tracked by defect family, and treat divergences as findings. Track first-pass yield per stage, but more importantly track the defect pareto per stage — a stage that catches nothing is either a redundant screen or an indicator your vectors are thin. Correlate field returns to the stage that should have caught them, and feed every escape back into the coverage model.
Audit the test programmes themselves. Vector sets drift from the design as revisions accumulate, and I have repeatedly found functional tests still stimulating circuits removed two board revisions earlier. Verify that boundary scan chain tests and interconnect tests reflect the current netlist, that fixture probes hit present pads, and that pass criteria match current specification limits. Configuration control of test programmes belongs under the same change discipline as product drawings; an uncontrolled test release is an unmeasured product.
Finally, measure detection, not just coverage. Inject known defects — deliberately faulted units, or fault injection in simulation — and confirm each stage catches what the model claims. This validation closes the loop between the paper model and the physical wall. It takes modest effort, exposes soft spots quickly, and gives the escape model the empirical footing it otherwise lacks. Without it, your coverage documentation is theory wearing a lab coat.
Building the Strategy Into Design
Coverage is decided in schematic capture and layout, long before any test programme is written. Test points on critical nets, maintained JTAG access, design-for-test rules on reset and clock control so devices can be held in a testable state — these decisions are cheap in design and prohibitively expensive to retrofit. Where I have seen coverage succeed, the test engineer had a seat at the design review with the authority to block access deletions.
Component selection matters as much as layout. Choosing devices with boundary scan, or with built-in self-test on complex silicon, transfers detection burden into parts that can verify themselves. Conversely, every non-scan device placed between two scan devices punches a hole in the interconnect net. A design review that maps expected coverage per net group before layout freezes can redirect routing or add access points while the cost is still a conversation rather than a respin.
Across two decades in automotive and aerospace quality, my closing position is this: the maturity of an electronics test programme is measured by how confidently it can name its own blind spots. Coverage numbers will never reach totality, and chasing a single headline figure wastes effort. Characterise the dark zones, model what leaks through them, price the leaks honestly, and spend where the arithmetic says so. That is a strategy — and it survives contact with field data.
Coverage claims versus escape reality
What teams claim
- One headline coverage percentage for the board
- Stuck-at coverage within scan logic quoted as board coverage
- Chain integrity counted as tested interconnect
- Heuristic estimates presented as simulated results
What a mature model states
- Segmented coverage: interconnect, component, functional
- Not-detected defect families named as accepted risk
- Environmental limits stated where no stimulus exists
- Field returns fed back to revise the model
Closing the loop between model and line
- 01Model defect spectrumRows per component family and process step, matched to the real line.
- 02Map detection capabilityPer test stage: detected, partial, conditional, or not detected.
- 03Price the escapesCost per defect family, not per test stage; compare to screen cost.
- 04Validate by fault injectionConfirm each stage catches what the model claims.
- 05Feed back field returnsPredicted escape means accepted risk; unpredicted means the model is wrong.