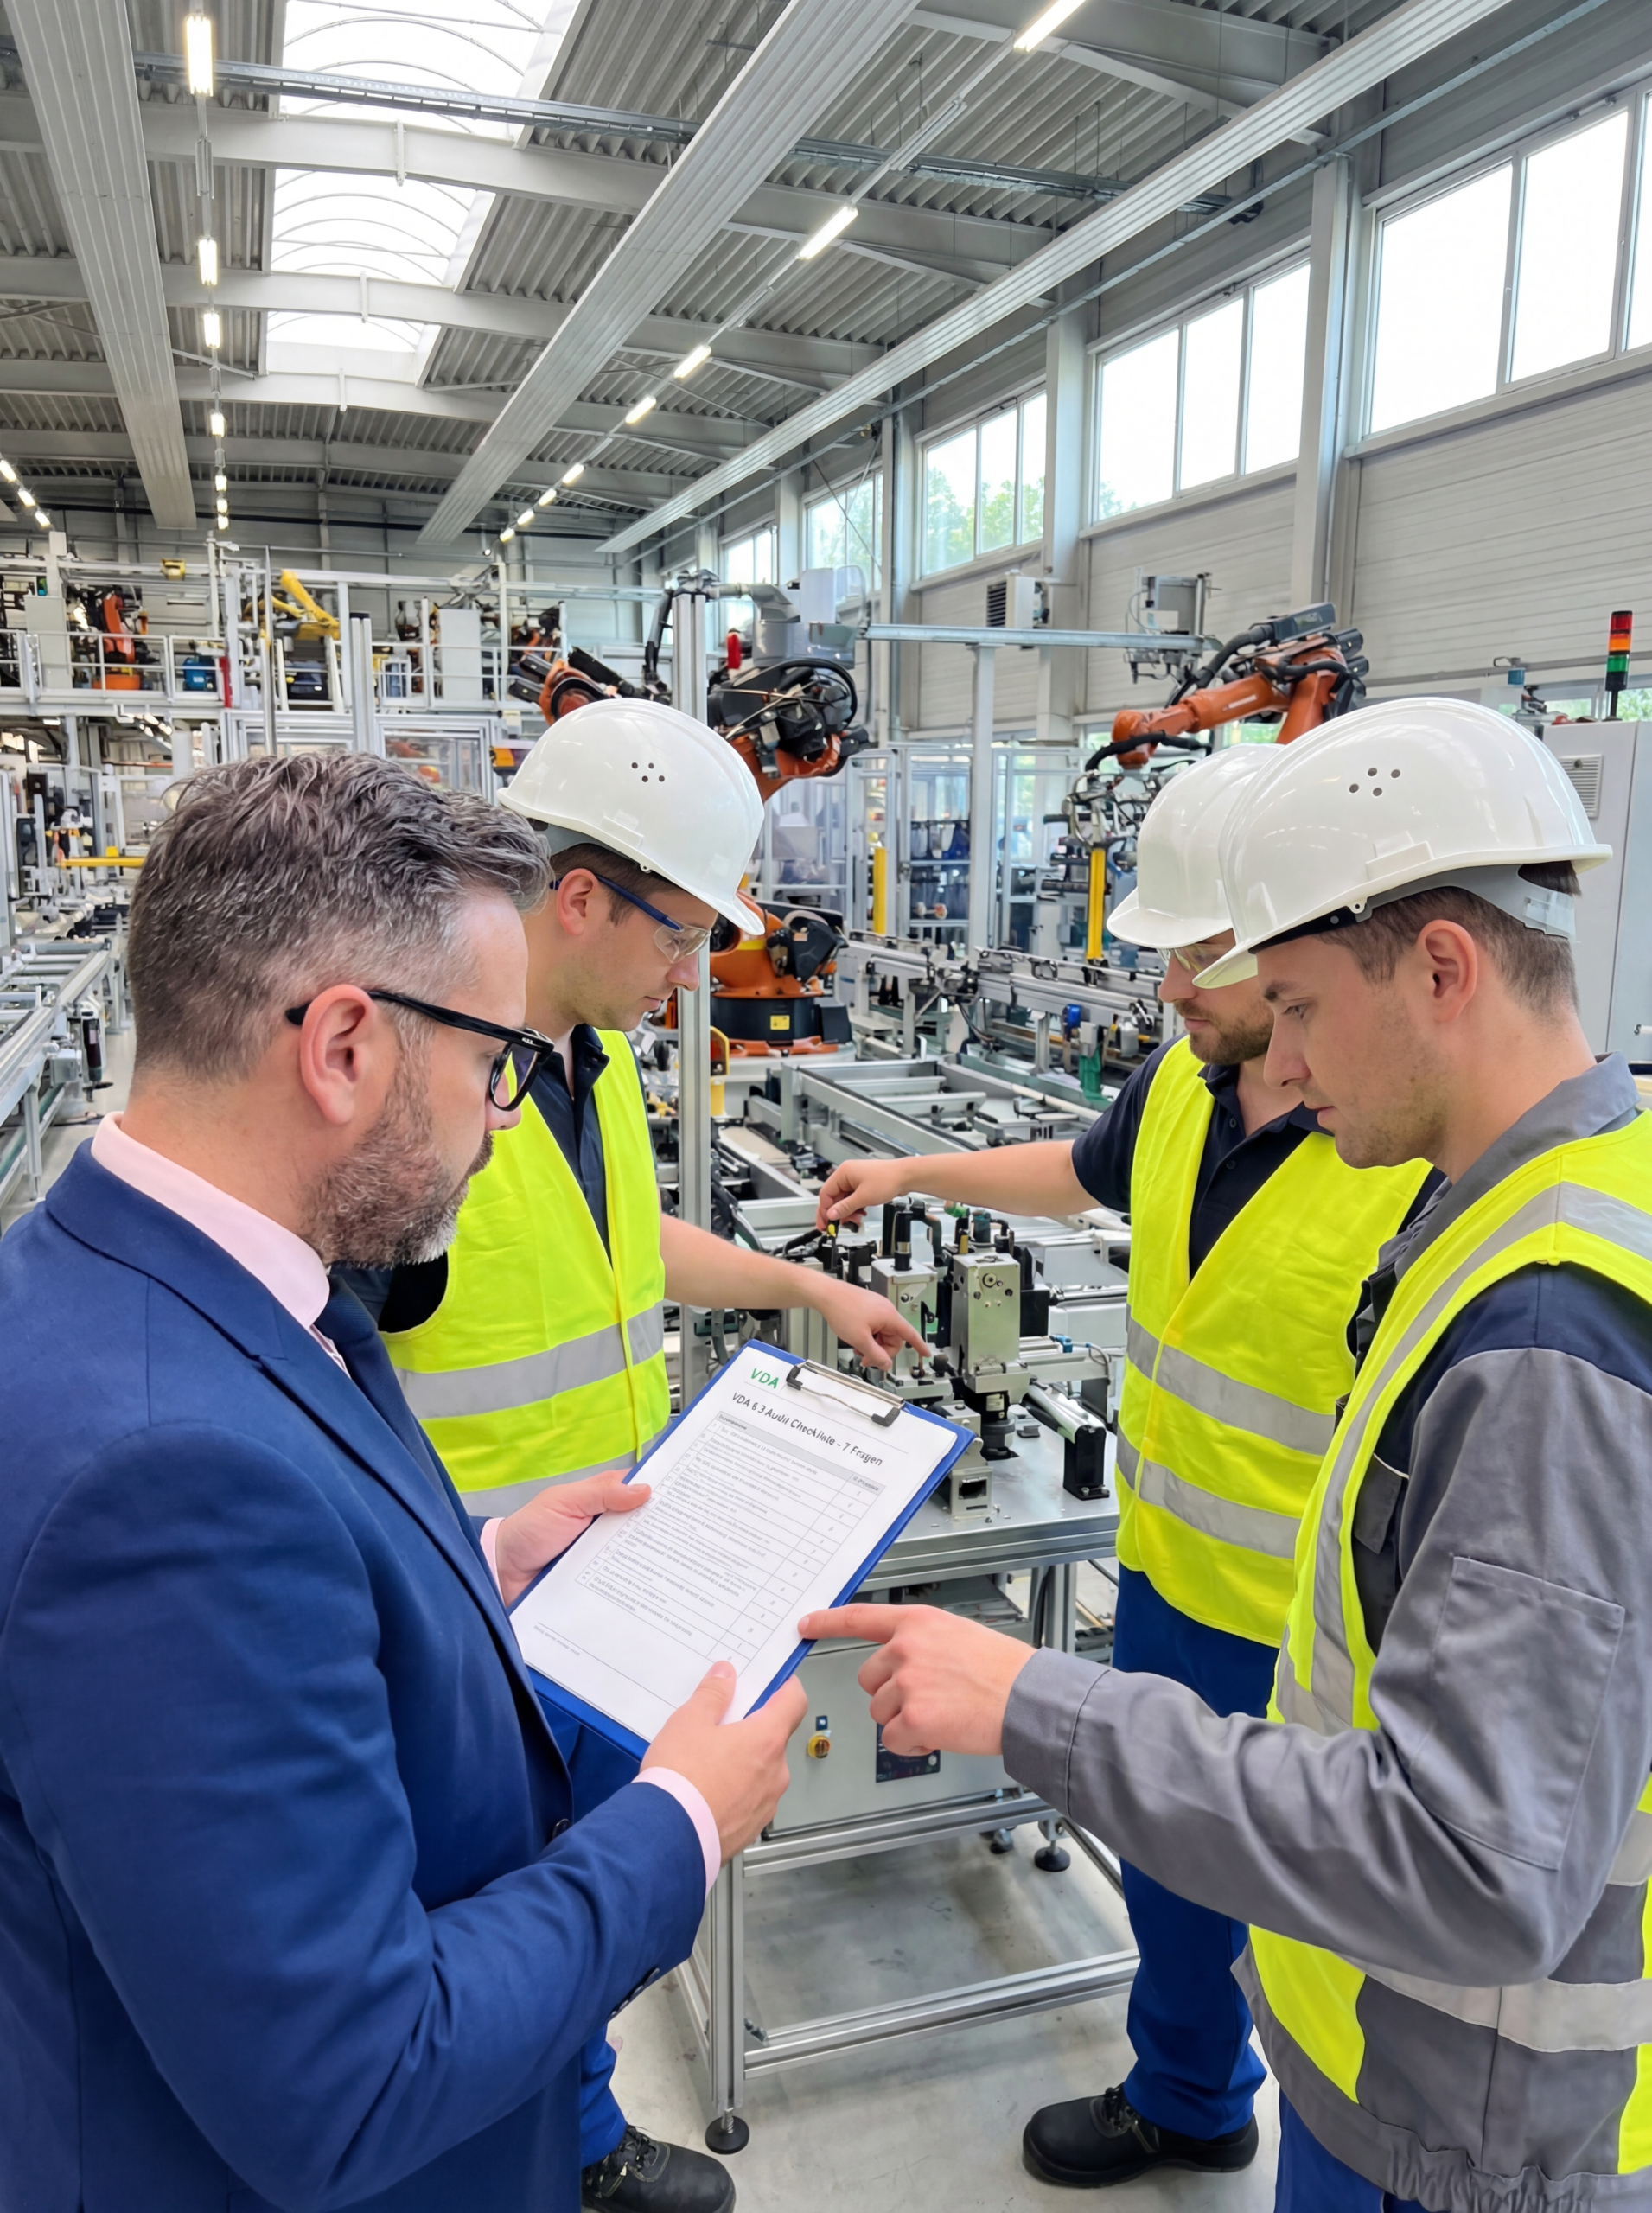
IATF 16949 certification tells a customer you have a quality management system. It does not tell them whether a specific production line can reliably hit specification. For that, German OEMs rely on VDA 6.3. Developed by the Verband der Automobilindustrie (VDA), this standard enforces a rigorous, evidence-based evaluation of individual processes.
I first encountered VDA 6.3 while supplying a major German OEM. We had a stable IATF 16949 system and years of clean delivery records. The VDA 6.3 audit request initially seemed like a formality. It was not. The methodology strips away systemic generalities and forces you to prove process capability on the shop floor.
The standard evaluates process elements across a supply chain, scoring them against strict criteria. It assumes that robust quality is built into the process flow, not inspected at the end. Understanding its specific scoring mechanism and what the auditors expect is critical for any supplier in the European automotive sector.
System Certification vs. Process Validation
The distinction between IATF 16949 and VDA 6.3 is fundamental. IATF asks whether you have documented procedures, a quality manual, and a functional management system. VDA 6.3 asks whether the specific manufacturing process for a specific part consistently produces conforming product.
This difference in scope dictates how you must prepare. A system audit relies heavily on document control and management reviews. A VDA 6.3 process audit puts the PFMEA, control plan, and work instructions under a microscope, then walks out to the machine to see if reality matches the paperwork.
Auditors do not accept partial credit. If a process element is defined but not followed, or followed but not capable, the finding is clear. The evaluation relies on a percentage calculation derived from specific questions, and falling below the classification threshold drops the process rating entirely.
| Audit Focus | IATF 16949 Scope | VDA 6.3 Scope |
|---|---|---|
| Primary Question | Does a functional quality system exist? | Does this specific process reliably work? |
| Evidence Base | Manuals, procedures, policies | Process flow, control plans, Cpk data |
| Failure Mode | Documentation gaps or overdue reviews | Incapable machinery or high gauge variation |
| Result Impact | Certification maintained or suspended | Process rated A, B, or C (Pass/Fail) |
The Core Evaluation Elements
VDA 6.3 organizes its evaluation into process elements covering the entire lifecycle, from project management to customer support. The most intense scrutiny falls on process element P6 (Process Analysis/Production). Here, auditors verify that requirements are understood, specifications are documented, and processes are statistically capable.
Evaluating process capability means proving that critical characteristics are stable. Standard practice demands a Cpk of at least 1.33 for stable parameters, but 1.67 for critical characteristics. If you cannot produce an MSA study and a stable control chart proving these metrics, the process is not capable.
Personnel qualification and nonconformity management carry equal weight. You must demonstrate that operators are trained specifically for the tasks they perform, with documented evidence. When a defect occurs, the 8D report must identify a verified root cause, not just a symptom.
Measurement System Analysis is Non-Negotiable
A common failure point in VDA 6.3 audits is the assumption that an existing Cpk report is sufficient evidence. Auditors will immediately investigate the Measurement System Analysis (MSA). If the gauge variation is too high, your process data is invalid. I have seen auditors completely dismiss a year of production data because the GR&R was above 15%.
To survive this scrutiny, your GR&R must be 10% or below. If the gauge contributes significant variation, you cannot prove that the process itself is stable. You are simply measuring noise. In my experience, correcting the measurement system often resolves the perceived process failure, bringing the true Cpk back into specification.
Statistical Thresholds for VDA 6.3 Compliance
Conducting Internal Process Audits
Suppliers should not wait for an OEM auditor to identify process weaknesses. Internal VDA 6.3 audits must become a standard part of your quality planning. This means assigning trained internal auditors to evaluate new product introductions, process changes, and annual re-qualifications using the VDA framework.
The internal audit must follow the exact same logic as the external one. Start with the process flow diagram, verify the control plan, and then physically walk the shop floor. Compare the work instruction to the operator's actual movements. Check the calibration dates on the gauges and review the latest SPC charts.
A process audit is not a paperwork exercise; it is a physical verification of how work actually happens on the floor.
Any deviation found during the internal audit requires immediate root cause analysis. Do not wait for a customer finding. If an operator is bypassing a step in the work instruction, the immediate reaction should not be disciplinary. It should be an investigation into why the documented process is not feasible or ergonomic.
Correcting Systemic Audit Failures
When a VDA 6.3 audit identifies a downfall, the immediate response must be systematic. The most frequent failure mode I encounter is missing or inadequate training records. Operators may know exactly how to assemble a part, but if the competency matrix is outdated, the process fails the audit on paper.
Another systemic issue is the quality of root cause analysis in 8D reports. Auditors will reject corrective actions that stop at 'operator error.' Effective root cause analysis uses tools like the 5 Whys to dig into the systemic failure. Was the fixture worn? Was the lighting inadequate? Was the gauge unreliable?
Auditor Logic for Process Capability Verification
- 01Review MSAVerify GR&R is below 10% before trusting any data.
- 02Verify StabilityCheck control charts for out-of-control points.
- 03Calculate CpkConfirm capability meets the 1.33 or 1.67 threshold.
- 04Floor VerificationObserve the process running live to confirm compliance.
Integrating VDA into Daily Operations
VDA 6.3 methodology should not be siloed within the quality department. It is a powerful operational tool. Plant managers can use the process element scoring to track manufacturing health. By calculating a monthly VDA score for critical lines, leadership gains a leading indicator of quality risk, rather than waiting for scrap reports.
This integration requires production supervisors to understand the standard. They must know which characteristics are critical (requiring Cpk 1.67) and ensure the control plans are followed meticulously. If the control plan specifies a check every 50 pieces, that frequency must be enforced and recorded without exception.
Ultimately, VDA 6.3 enforces a discipline that separates world-class suppliers from the rest of the market. It eliminates the grey areas in quality assurance. By demanding measurable proof of process capability and rigorous root cause analysis, it establishes a baseline where consistent quality is a mathematical certainty, not a best effort.