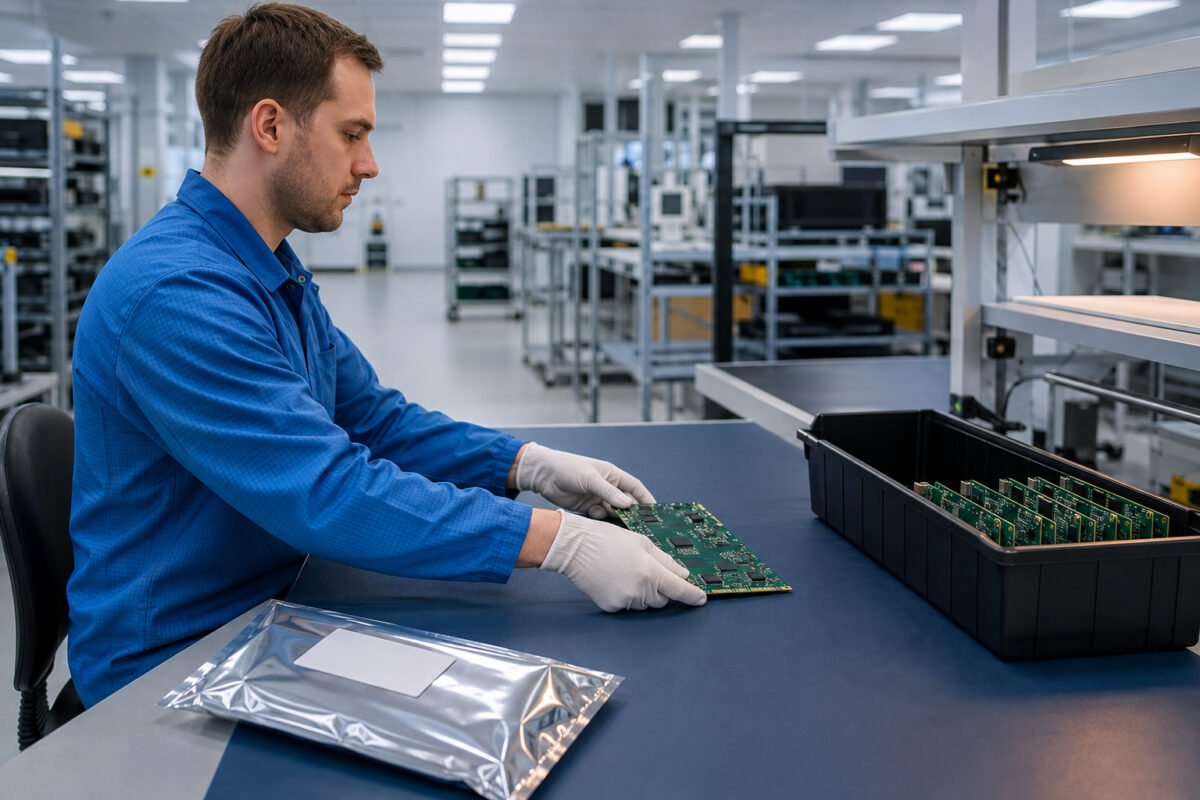
The most expensive ESD event I ever witnessed produced no scrap ticket, no alarm, and no operator report. A board passed every functional test at end of line, shipped, and failed in the field after roughly four months of service. Failure analysis traced it to a gate oxide rupture on a microcontroller input pin — the classic latent defect signature. The device worked because the damaged oxide still held charge; thermal cycling and electrical stress enlarged the defect until the pin leaked beyond specification.
That is the central problem with static damage: it is largely invisible at the moment of infliction. Catastrophic failures — a shorted junction, an open metallisation trace — get caught at test and cost you a board. Latent failures get caught by your customer, or worse, by their customer. The economics invert completely: a rejected board costs rework and material; a field failure costs analysis, containment, sorting, travel and credibility.
The mechanism is well documented in semiconductor physics. A charged device event discharges through a small-geometry structure and partially punctures the gate oxide without destroying it. Electromigration and oxide trapping then degrade the site progressively. Nothing in standard functional or in-circuit test will see it, because the defect does not yet affect electrical parameters at room temperature.
The Physics of the Failure You Cannot See
Latent damage occupies the middle ground between a hard failure and a healthy die. The oxide is punctured but still functional, so parametric tests at room temperature read clean. Time, temperature and operating voltage do the rest: the trap density at the rupture site grows, leakage rises, and the part eventually drifts out of specification or latches up in service.
This changes what you audit for. You are not auditing to prevent visible scrap. You are auditing to prevent a failure mode that will surface statistically somewhere between weeks and years from now — long after the process that caused it has shifted, the operator has changed shifts, or the contract manufacturer has changed. That temporal disconnect is precisely why ESD programmes decay: the penalty arrives after the evidence has disappeared.
It also changes how you read your own metrics. First-pass yield, defect logs and rework rates will register nothing from a latent defect mechanism. A plant can post excellent quality numbers while systematically implanting field failures. If your ESD programme is judged by yield, it is being judged by the one instrument that is structurally blind to the risk.
Auditing for What Does Not Show Up in Yield
Standard process audits look for evidence tied to immediate output. ESD auditing must assume the evidence of failure will never appear in those records. The audit becomes an exercise in verifying physical conditions and behaviours whose absence of consequence proves nothing — today.
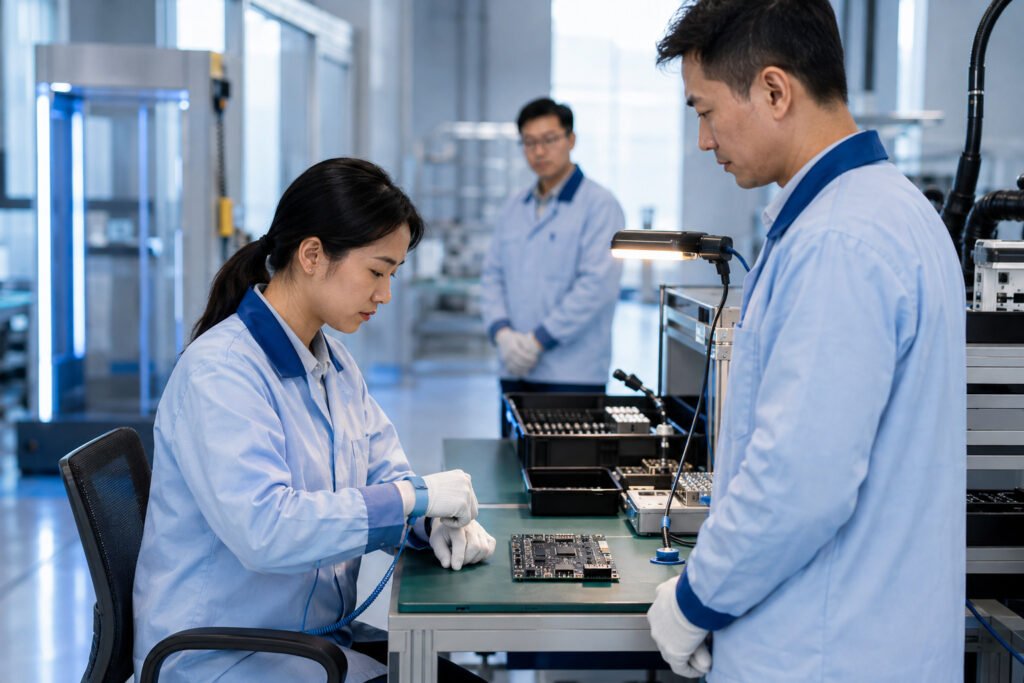
I audit to the physical requirements, not the paperwork. That means walking the protected area with a meter, not a checklist. Verify worksurface mats are actually bonded to the common point ground — I have found mats daisy-chained to a bench socket safety earth where one corroded link left three benches floating. Measure wrist strap continuous monitors against a calibrated verifier, because monitors drift and can fail silently into a pass state. Check that ground cord snaps actually engage; worn sockets that no longer lock are among the most common and most ignored findings.
Footwear and flooring deserve measured verification, not observation. A foot grounder tester tells you the strap was good at the door. It says nothing about contaminated soles, floor finish worn through on high-traffic lanes, or dissipative tiles cleaned with a product that left an insulative film. Measure point-to-point resistance along actual walking paths, not just at the entry point where everyone prepares for the audit.
Ioniser verification is the most neglected item. Ionisers neutralise charge on insulators and ungroundable items, but they demand emitter cleanliness, balance calibration and airflow verification — an unbalanced ioniser can itself induce charge on nearby assemblies. Records must show periodic discharge-time and offset-voltage checks with measured values. "Checked and OK" is not a record; it is a liability.
Wrist Strap Monitoring: Where Programmes Quietly Die
Wrist straps fail in ways monitoring should catch but often does not. The obvious failure — a broken conductor or worn curl cord — is caught by daily testers. The insidious failure is skin contact. An operator with dry skin, or one wearing the band loosely over a sleeve, can present a resistance path well above the acceptable range while still getting a green light from a tester with too generous a pass threshold.
Single-wire vs dual-wire continuous monitors
Single-wire monitor
- Verifies the ground path through a strap resistor
- Cannot detect a band that has slipped off the wrist
- Cheaper to install, structurally blind to skin contact
- Acceptable only for less sensitive assemblies
Dual-wire monitor
- Measures the resistance loop through the operator's skin
- Detects loose bands, dry skin, sleeve interference
- Provides an auditable resistance value per operator
- Required where device sensitivity warrants it
Then there is the behavioural dimension. Operators defeat monitors: clipping the band to a grounded bench edge, wrapping the strap over a glove, or working around an alarm that has cried wolf too often. During audits I watch for the alarm-acknowledgement reflex — if an operator silences a monitor without looking at it, the monitor has become furniture. Interview them. Ask what the alarm means and what they do about it. The answers tell you more than the calibration sticker.
Records matter most at the boundaries. Daily test logs, verifier calibration, monitor function checks and the disposition when an operator fails all need to be current. A strap tester out of calibration for a year means every logged pass in that period is unsupported. If a latent-failure field return traces back through that window, you have no defence and no data to bound the exposure.
Packaging That Undoes Everything Downstream
You can run a flawless protected area and still inflict charged device events in the warehouse. The dominant failure mode is tribocharging inside packaging that looks acceptable: pink poly bags, foam, bubble wrap. Many materials are graded low-charging rather than dissipative or conductive, and low-charging properties decay with handling, humidity and age. A bag that met specification new may not after six months in your kitting loop.
An open shielding bag with a folded top is not a Faraday cage; it is a decorated plastic bag.
The charged device event deserves particular attention. Devices with fine-pitch leads and assembled boards with exposed connectors charge themselves through friction against packaging during transport and vibration. When a hand or metal surface then touches a pin, the device — not the person — discharges. Shielding bags address this with a metallised layer forming a Faraday cage, but only if the bag is closed and undamaged.
I inspect packaging on three points. Integrity: shielded bags with perforations, torn seams or delaminating metallisation go straight to scrap. Closure: labels, not staples; folds secured, not just creased. Marking: the ESD protective symbol and material classification must be legible, because downstream handlers at the customer or repair centre make decisions based on it. Do not confuse moisture barriers with ESD shielding — they are separate properties and both must be specified.
Incoming and outgoing goods are part of the chain. Verify how your supplier ships subassemblies and how your own despatch area handles product after final test. The field failure I described at the start traced back not to production but to despatch, where finished boards were slid across a nylon-covered table into open bins before bagging — a step nobody had included in the protected area boundary because the product was already tested.
The Economics of Latent Damage
Cost accounting for ESD is structurally biased towards inaction. Visible failures appear in scrap and rework accounts, where they are small and manageable. Latent failures appear in warranty returns, field failure analysis, customer scorecards and occasionally a recall-class event — accounts that are aggregated, delayed, and rarely attributed back to the ESD programme that caused them. When the cost arrives, the causal process has usually changed beyond reconstruction.
Count what one field return actually costs beyond the replacement part: 8D-style analysis with cross-functional hours, decap or acoustic microscopy at an external lab, sorting of suspect stock, engineer travel to the customer, and the escalation meeting where you explain why your test coverage missed it. Then consider that a single latent-defect mechanism typically produces not one return but a scattered population, because the process condition affected every unit processed during that window. You rarely identify the window cleanly, so the customer sorts or replaces everything.
Where ESD costs actually land
Against that, the cost of a functioning programme is mundane: straps, monitors, mats, flooring maintenance, packaging stock, verification labour and training refresh. None of it generates revenue or visible yield improvement, which is why it is the first candidate when budgets tighten. The programme is cheap insurance against an unbounded tail risk, and the tail is what ends careers and supply relationships.
There is also a contractual dimension. Automotive and aerospace customers increasingly flow down ESD control requirements against recognised standards — IEC 61340-5-1 in electronics, with ANSI/ESD S20.20 widely referenced — and audits check for documented compliance plus objective evidence. Losing a certification of conformity, or scoring poorly on a customer process audit because of corroded ground snaps and unverified ionisers, is a self-inflicted wound with commercial consequences well beyond the ESD programme itself.
Making Latent Risk Visible Before It Ships
If you cannot detect latent damage with functional test, you must manage it through the conditions of processing, then verify those conditions continuously rather than periodically. The practical tools are dual-wire continuous monitoring where sensitivity warrants it, defined and marked protected area boundaries that include test, repair and despatch, and a packing specification controlling material class, closure and handling surfaces.
Verification needs teeth. Set measurable acceptance criteria — worksurface-to-ground resistance, floor point-to-point resistance, ioniser discharge time and balance voltage — and record actual values on a schedule with trend review. When a measured value drifts towards the limit, treat it as an early warning, not a pass. Flooring and worksurface materials degrade, and the drift pattern tells you the replacement interval before you start failing.
Humidity is part of the programme whether you own it or not. Low relative humidity, typically in winter heating seasons, dramatically increases tribocharging on flooring, garments and packaging alike. Coordinate with facilities so humidity logging in the protected area is reviewed by the ESD coordinator, not just by a building management system nobody reads. A seasonal spike in field returns traced to a dry-weather processing window is a painful way to learn this.
Finally, when a field failure analysis points to EOS/ESD damage, treat it as programme intelligence rather than an isolated event. Pull the processing records for the date code, reconstruct the conditions — monitor logs, maintenance history, staffing, humidity — and feed the findings back into the audit checklist. Each confirmed latent failure gives you a specific, evidenced weak point. That is the only feedback loop that works, because the yield data will never tell you.