Every quality culture has a stress test, and it never arrives conveniently. A line operator, a test technician or a supplier quality engineer notices something wrong with a part or process that is holding up a shipment, feeding a launch, or protecting a customer relationship already under strain. They raise it. The room goes quiet. Production wants to run, sales wants to ship, and management wants the problem to be a misunderstanding.
What happens in the following forty-eight hours tells you more about your quality system than any audit ever will. Across two decades in automotive and aerospace plants, I have watched this scenario play out dozens of times. The organisations that handle it well share specific, observable behaviours: protection for the reporter, genuine independence in the investigation, and outcomes that follow the evidence rather than the schedule.
The organisations that handle it badly share behaviours too, and they are depressingly consistent. This article is about the mechanics of getting it right — the procedures, boundaries and authorities that hold when pressure is applied — not the slogans on the wall.
Protect the Messenger Before You Protect the Schedule
The first failure mode in these situations is rarely technical. It is the slow, often unintentional campaign of pressure that begins the moment an inconvenient concern is voiced. The reporter gets pulled aside by a supervisor asking whether they are "sure" about what they saw. Colleagues hint the line might move to another shift if this continues. Someone in the production meeting asks, loudly, who flagged the issue, as though the reporter's identity were a relevant engineering fact.
None of this appears in any procedure, yet all of it destroys the reporting channel faster than any formal policy can rebuild it. Escalation protection therefore has to be structural, not aspirational. Write into the concern-reporting procedure an explicit statement that adverse personnel action linked to a good-faith quality report is a dismissible offence — endorsed by the site director, not just the quality manager. Provide a bypass around the immediate chain of command: a confidential hotline, a direct line to the quality director, or an electronic system where the reporter controls who sees their name.
Then audit the protection. Trace who raised each concern and check, six months later, whether their performance ratings, shift assignments or overtime access changed. Patterns there are your real culture metric. Watch for the subtle signals as well: if the only people reporting concerns are those already friendly with the quality department, your channel is narrower than the report count suggests. When a serious report comes from an unexpected source — a contractor, a new hire, a maintenance fitter — treat that as evidence the channel is working, and say so publicly.
Quarantine First, Argue Second
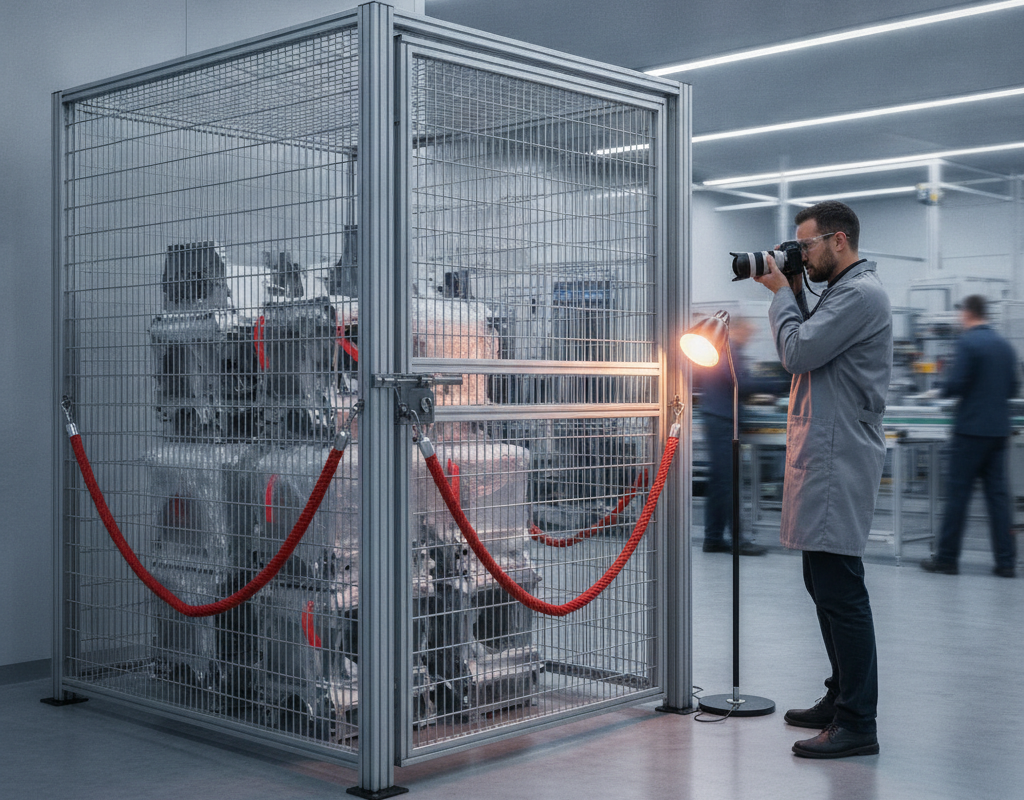
Once a concern is raised about potentially nonconforming product, the physical handling of that product becomes the immediate battleground. The instinct in every plant is to keep material moving while the debate happens — set it aside in a lane, keep the line running, hold it "in the system". The problem is that stock in a logical hold is still physically available, and under schedule pressure someone will dip into it. I have seen suspect material shipped from a "quarantined" pallet more than once because the hold was a label on a screen, not a locked cage.
Physical segregation must be immediate and unmistakable: red tags, a roped or caged area, material moved out of the production flow entirely where volumes allow. If the suspect lot cannot be physically isolated because it is already interleaved with good stock, then the containment boundary is bigger than the suspect quantity, and you must accept that. Pull the traceability records — heat numbers, serials, date codes, batch records — now, not later, because reconstruction after further processing is far harder.
The quarantine decision itself must not depend on consensus. Define in advance who holds stop-ship authority, and ensure that authority sits with quality, not with the function whose output is being questioned. A production manager should never be able to overrule a quarantine unilaterally, however far behind the schedule is. Equally, quality must use the authority honestly — a quarantine that is really a negotiating lever breeds the cynicism that makes the next quarantine impossible to enforce.
Make the Investigation Genuinely Independent
Independence does not mean bringing in outsiders for every concern. It means the people determining whether the concern is valid cannot have their objectives, bonuses or standing damaged by the answer. If the concern implicates the process engineering group and the investigation is run by that group's own supervisor, the investigation is compromised regardless of how honest the individuals are. The findings will be framed, the scope narrowed, the conclusions softened — often unconsciously.
Practical independence looks like this: the investigation lead is one organisational level above the implicated function, or from a parallel function with no stake in the outcome. For serious concerns — anything touching safety-critical characteristics, flight safety or regulatory compliance — a corporate or external quality representative participates directly, not as a reviewer after the fact. Write the scope down before evidence gathering begins, because scope is where investigations are quietly steered: define the suspect window narrowly enough and you exclude the shipped material; widely enough and the data becomes unusable.
Evidence discipline matters as much as who leads. Photograph everything before it is disturbed. Preserve the actual suspect parts — do not let them be cut up for metallurgical analysis before dimensional and visual documentation is complete, and do not let them disappear into a scrap bin during cleanup. Pull the process data: machine parameters, torque traces, thermal profiles, operator logs, calibration records for the gauges involved. Interview the reporter early, without their supervisor present, and record what they actually observed rather than what they concluded. Their conclusion may be wrong; their observation is usually the most valuable evidence you have.
The first 48 hours of a serious concern
- 01Secure the reporterConfirm protection and record what was observed, not concluded.
- 02Quarantine physicallyLocked containment, red tags, boundary defined from records not guesswork.
- 03Appoint independent leadOne level above the implicated function; written scope before evidence gathering.
- 04Preserve evidencePhotograph, retain parts, pull process and calibration data.
- 05Contain the populationScreening method verified on known-bad parts before use.
- 06Notify the customerEarly, with a clear containment description, before the full picture exists.
Interim Containment While the Truth Is Being Established
The gap between "concern raised" and "root cause confirmed" is where organisations leak nonconforming product. Formal problem-solving has its place — 8D, fault-tree analysis, design of experiments — but containment is what protects the customer in the meantime. The question is brutally simple: what additional verification, applied to what population of product, gives reasonable confidence that nothing defective has escaped or will escape while we investigate?
Containment must be proportionate to the exposure. If the concern is a crack in a weld on the third operation of five, containment starts at the point of detection and extends backwards through every lot that passed the operation since the last verified good check — a clean boundary established from process records, not guesswork. Screening at incoming or final inspection needs a method actually capable of detecting the suspected defect: visual inspection will not find internal porosity, so you may need radiographic or ultrasonic screening, sectioning of a sample, or functional testing. Verify the screening method on known-bad parts before trusting it on unknown ones, and log every screened unit.
Tell the customer when the exposure reaches them, and tell them before you have the full picture. In aerospace this is largely non-negotiable under regulatory reporting expectations; in automotive it is what warranty and recall arithmetic demands anyway. A customer who hears from you early, with a clear containment description, is a partner. A customer who discovers the escape through their own line stoppage owns the narrative from that point forward. I have never seen early notification make an outcome worse.
Outcomes That Follow the Evidence
Once the investigation concludes, the outcome phase is where culture is either cemented or squandered. Three outcomes are possible: the concern was valid and product is affected; the concern was valid but no product escaped; or the concern was a misunderstanding and the product is fine. Each demands a different response, and conflating them is how organisations teach people to stop reporting.
The reporter's conclusion may be wrong; their observation is usually the most valuable evidence you have.
When the concern proves valid, act on the full population, not the convenient one. Suspect material gets dispositioned — scrap, rework to a documented and validated method, or use-as-is only with a formal material review board decision supported by engineering evidence, never by schedule pressure. The corrective action addresses the failure mode at its origin: a fixture redesign, a process parameter change with capability evidence such as a demonstrated Cpk, or a work instruction that reflects what the process actually requires. Communicate the outcome back to the reporter specifically and to the workforce generally, in terms that show the report made a difference.
When the concern proves unfounded, resist the temptation to treat it as a false alarm that wasted time. If the reporter reasoned from what they genuinely observed, the correct response is gratitude plus coaching: here is why the feature you saw is within expectation, here is the drawing clause or process characteristic that explains it. The only report deserving criticism is one made recklessly or maliciously, and those are vanishingly rare compared to the reports never made at all. Thank the reporter in front of the same audience that watched the quarantine happen, because that audience is calculating the social cost of speaking up next time.
Two plants, one concern
What compromised plants do
- Reporter's identity circulates in the production meeting
- Suspect stock held "in the system" but physically accessible
- Investigation led by the implicated function's own supervisor
- Unfounded concern treated as wasted time; reporter coached informally to be quieter
What sound plants do
- Protection confirmed by site director; bypass channel available
- Locked, red-tagged quarantine outside the production flow
- Independent lead, written scope, evidence preserved before analysis
- Reporter thanked publicly either way; observation recorded as evidence
Close the Loop Without Closing the Case Too Early
Verification is the step most often truncated once schedule pressure lifts. The corrective action gets implemented, one batch runs clean, and everyone moves on. Then the failure mode reappears six weeks later because the action addressed a symptom, or because the verification window was too short to catch an intermittent process behaviour. Weld porosity driven by humidity, torque variation driven by tool wear, sealant cure variation driven by seasonal temperature — none of these respect a one-week validation period.
Insist on a defined verification window with stated evidence: consecutive production runs, specific sample sizes, specific measurements tracked against limits, and a named person who signs off the closure. For characteristics with customer safety or regulatory weight, the verification evidence belongs in the permanent record, linked to the affected part numbers, so that the next engineer investigating a related issue five years from now can find it. Traceability of decisions is as important as traceability of parts.
Finally, examine the system question hiding inside every hard escalation: did this concern have to arrive as a surprise? Somewhere upstream there was usually a missed signal, an inspection that lapsed, a process drift nobody monitored, a design margin nobody challenged. The report nobody wanted to hear is often the system telling you, late but clearly, that an earlier signal was ignored. Treat each one as tuition already paid, and extract the learning — that is what separates a quality culture that survives its stress tests from one that merely survives the audit.